

[Principle and Operational Features of High-Calcium Powder Conveying Systems]
High-calcium powder conveying equipment is a specialized system designed for the efficient handling and transportation of powders with high calcium content. These systems are crucial in industries where calcium-rich materials are processed, such as food, pharmaceuticals, and chemical manufacturing. The equipment ensures precise and controlled movement of the powder, minimizing dust generation and maintaining product integrity.
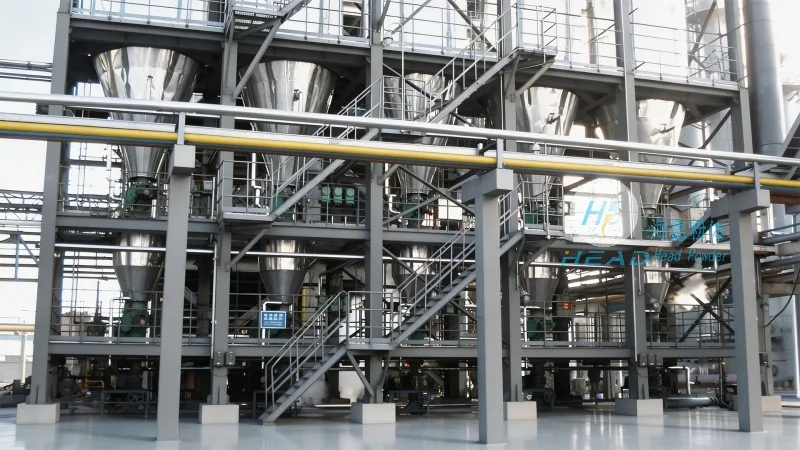
Principle of Operation
The core principle of high-calcium powder conveying systems involves the use of mechanical components to move bulk powders through a pipeline. Key components typically include a hopper for material storage, a conveyor mechanism (like a screw or pneumatic system), and a control unit to regulate flow. The design is optimized to handle powders with high moisture content or cohesive properties, which are common in calcium-rich materials. The system operates by creating a pressure differential or using mechanical force to propel the powder forward, ensuring consistent and reliable transport. This approach minimizes product degradation and maintains the purity of the calcium content, which is critical for applications in food and pharmaceutical industries.
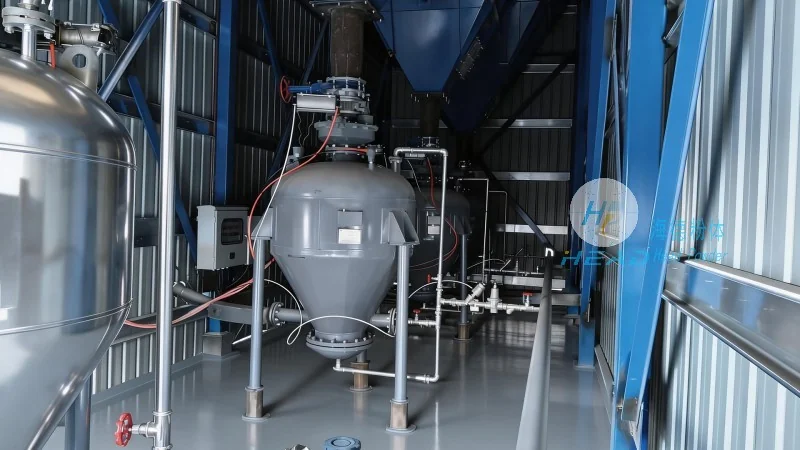
Key Features and Technical Specifications
High-calcium powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is engineered with several advanced features to enhance performance and durability. These systems are constructed from materials resistant to corrosion and wear, such as stainless steel, which is essential for handling calcium-based powders that may be abrasive or reactive. The equipment incorporates advanced control systems that allow for real-time monitoring of flow rates, pressure, and temperature, ensuring optimal operation. Additionally, the design includes features to reduce dust generation, such as sealed hoppers and enclosed conveyor paths, which improve safety and compliance with environmental regulations. The systems are also designed for easy maintenance, with accessible components that can be serviced without extensive downtime.
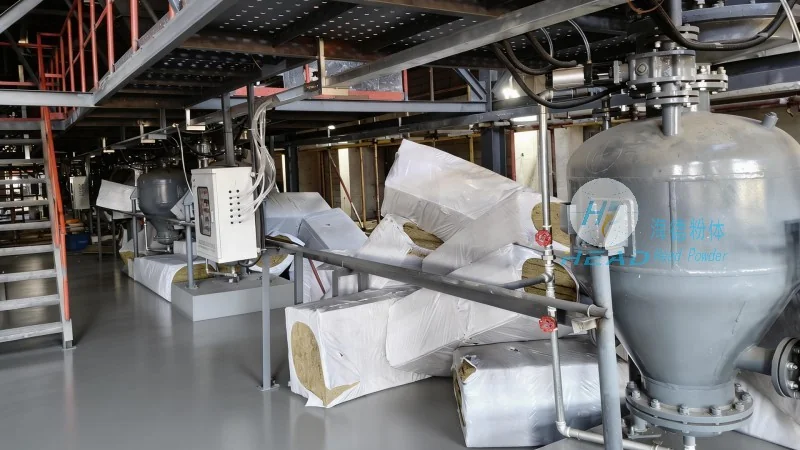
Application Scenarios
High-calcium powder conveying equipment is widely used in various industrial applications where calcium-rich materials are processed. In the food industry, these systems are used to transport calcium supplements, dairy powders, and other calcium-based ingredients to production lines. The equipment ensures that the powder is delivered in a consistent and hygienic manner, meeting the stringent quality standards required for food products. In the pharmaceutical industry, the systems are used to handle calcium-based active ingredients, ensuring that the powder is transported without contamination or degradation. The precision and control offered by these conveyors are vital for maintaining the efficacy of the pharmaceutical products. In chemical manufacturing, the equipment is used to transport calcium compounds used in the production of fertilizers, coatings, and other chemical products. The ability to handle high volumes of powder efficiently makes these systems essential for large-scale production.
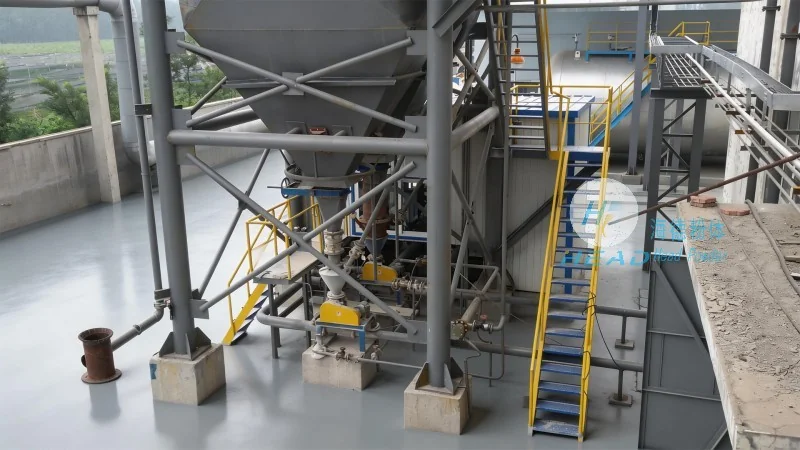
Benefits for Industrial Operations
Implementing high-calcium powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers several benefits for industrial operations. The primary advantage is the improved efficiency in material handling, as the systems can transport large volumes of powder with minimal labor and energy input. This leads to cost savings and increased productivity. Additionally, the equipment reduces product loss and waste by minimizing dust and spillage, which is critical for maintaining material quality and reducing environmental impact. The systems also enhance safety in the workplace by reducing exposure to airborne dust and ensuring that the powder is handled in a controlled environment. Furthermore, the advanced control systems allow for better process management, enabling operators to monitor and adjust the conveying process in real time. This leads to improved product consistency and reduced downtime due to equipment malfunctions.