

Principle and Working Scene Characteristics of Recycled Sand Powder Conveying System Equipment
In the casting industry, the recycling of reclaimed sand is a key factor in improving production efficiency and reducing costs. HeadPowder (Shandong HeadPowder Engineering Co., Ltd.)'s recycled sand powder conveying system equipment, through advanced technical design, effectively solves the challenges in the conveying process of reclaimed sand, providing a reliable solution for industrial production.
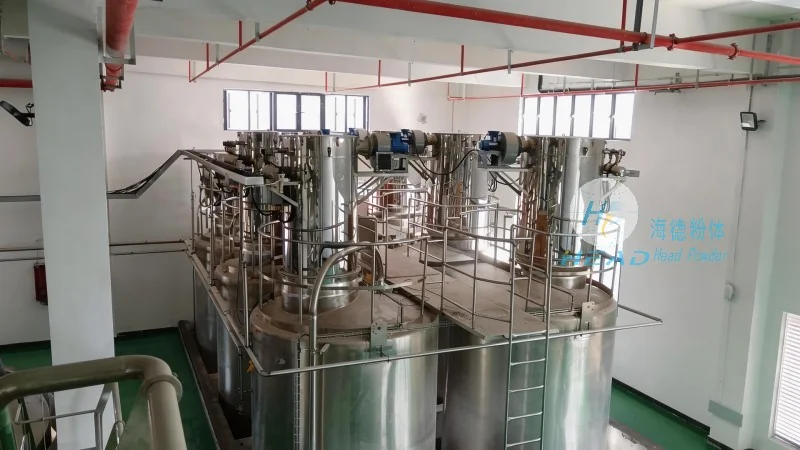
System Principle: The Technological Core for Efficient Conveying of Reclaimed Sand
HeadPowder's recycled sand powder conveying system equipment is based on mature powder conveying technology, optimized for the characteristics of reclaimed sand. The system typically combines pneumatic and mechanical conveying methods to ensure stable conveying of reclaimed sand, reducing dust dispersion and material loss. The internal structure of the equipment is designed rationally, such as using wear-resistant materials for conveying pipelines and valves, effectively extending the service life of the equipment. At the same time, the system is equipped with an intelligent control system, which can adjust the operating state in real time according to parameters like conveying volume and pressure, achieving automation and precise control to improve overall conveying efficiency.
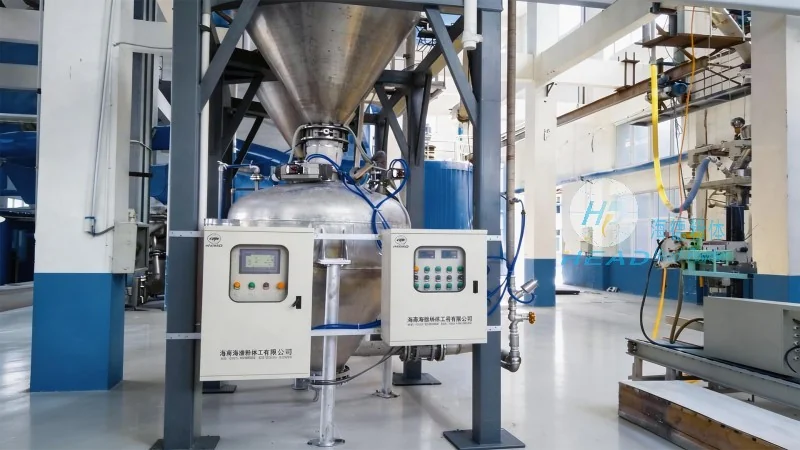
Working Scene Characteristics: Adapting to Diverse Industrial Needs
This conveying system equipment is widely applied in foundries, sand treatment facilities, and industrial sand recycling projects. In foundries, the equipment can efficiently convey reclaimed sand to mixers, molding production lines, and other parts of the production process, ensuring the continuity of the production flow. For sand treatment facilities, the equipment can handle reclaimed sand with different particle sizes and moisture contents, achieving the classification and conveying of sand materials. Additionally, the system has good adaptability, capable of dealing with different working environments such as high temperature and dust environments, reducing environmental pollution through sealing design and meeting the environmental requirements of modern industry. The equipment is easy to operate and has low maintenance costs, suitable for long-term stable operation, bringing continuous economic benefits to users.
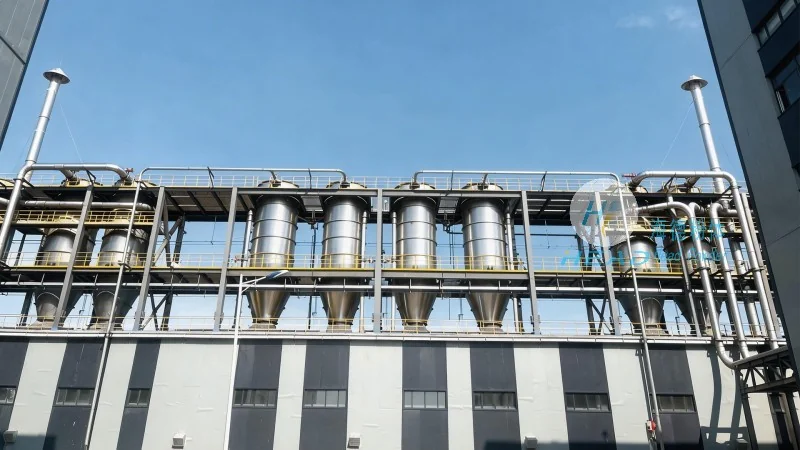
Technical Advantages and Practical Application Cases
HeadPowder's recycled sand powder conveying system equipment has significant technical advantages. For example, it adopts variable frequency control technology to adjust the conveying speed according to actual needs, reducing energy consumption; and is equipped with dust collection devices to reduce air pollution and improve the working environment quality. In practical applications, the equipment has been successfully applied in the reclaimed sand recycling systems of many foundry enterprises, effectively improving the utilization rate of sand materials and reducing the cost of new sand procurement. User feedback shows that the equipment operates stably, has a low failure rate, and is easy to maintain, fully reflecting HeadPowder's professional capabilities and technological innovation in the field of powder conveying equipment.