

Principles and Working Scene Characteristics of Rare Earth Material Handling Systems
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced rare earth material handling systems. These systems are engineered to efficiently transport and manage rare earth materials, which are critical components in modern industrial applications, including electronics, renewable energy, and advanced manufacturing.
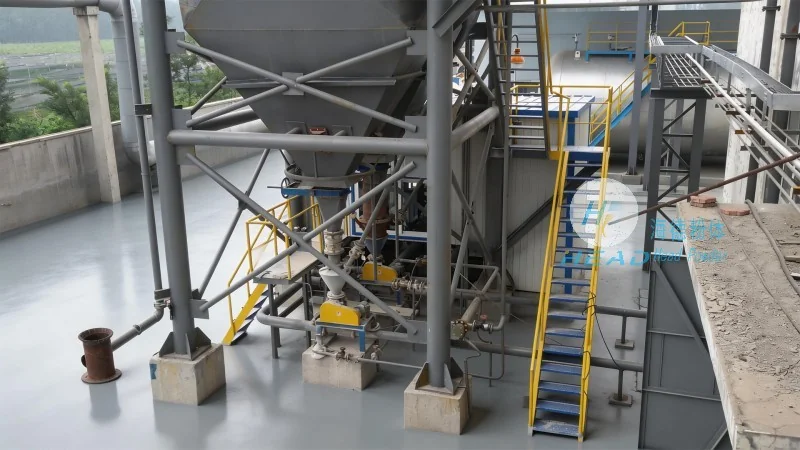
System Principles: The Core Mechanics of Rare Earth Material Transport
The rare earth material handling system operates on a combination of mechanical, pneumatic, and sometimes hydraulic principles, tailored to the specific physical properties of rare earth materials. These materials often exhibit unique characteristics such as high density, magnetic susceptibility, and varying particle sizes, which necessitate specialized handling solutions. The system typically includes components like feeders, conveyors, magnetic separators, and storage bins, all integrated to ensure a seamless flow of materials from extraction to processing.
At its core, the system uses controlled feeding mechanisms to regulate the flow rate of rare earth materials, preventing overloading or blockages. Conveyors, which may be belt, screw, or bucket types depending on the material's characteristics, transport the materials through the system. Magnetic separators are strategically placed to remove ferromagnetic impurities, ensuring the purity of the rare earth materials. Storage bins and silos are designed to hold the materials securely, with discharge mechanisms that allow for controlled release into subsequent processing stages.
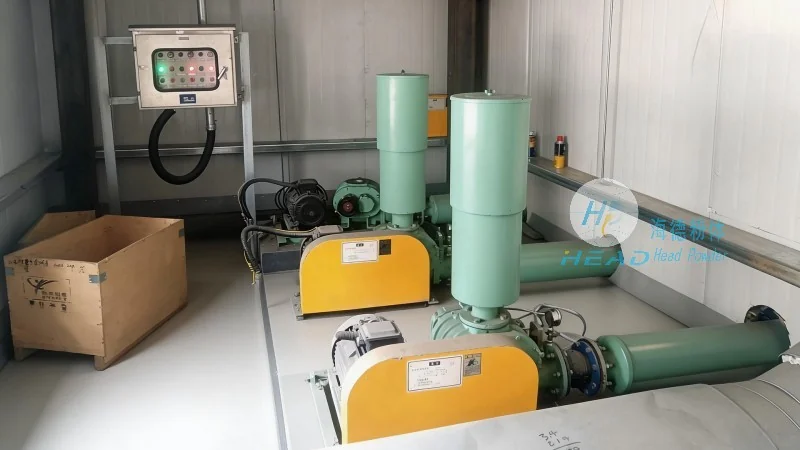
Working Scene Characteristics: Tailored Solutions for Diverse Applications
The working scene characteristics of rare earth material handling systems are defined by their adaptability to various industrial environments and processing requirements. In mining operations, the system may be used to transport raw rare earth ores from extraction sites to processing plants, where the materials are pre-treated and prepared for further refinement. The system's robust design and durability are essential in these harsh environments, where exposure to dust, moisture, and heavy loads is common.
In manufacturing facilities, the system is integrated into production lines to handle rare earth compounds and powders, ensuring a consistent supply to downstream processes like sintering, casting, or coating. The precision and reliability of the system are critical here, as any disruption can impact product quality and production efficiency. The system's ability to handle fine powders without generating excessive dust is particularly important, as rare earth powders are often sensitive to contamination and agglomeration.
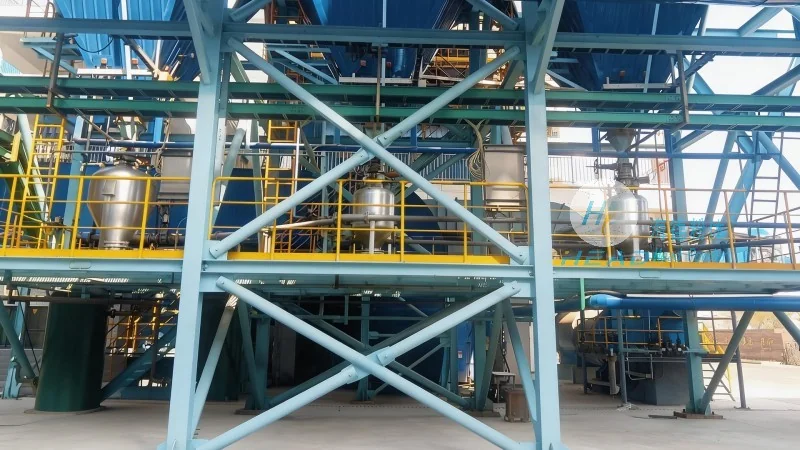
In recycling and reclamation operations, the rare earth material handling system plays a vital role in sorting and processing recovered materials. The system's flexibility allows it to handle a mix of materials, including scrap from electronic devices and industrial waste, and separate valuable rare earth elements from non-relevant components. This not only supports sustainable practices but also enhances the economic viability of rare earth recycling by optimizing material recovery rates.
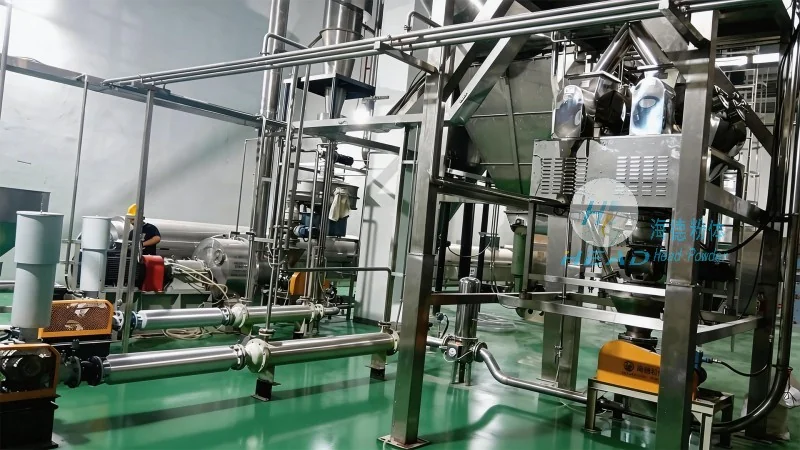
Company Expertise and Application Focus
Shandong HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, leverages decades of experience in material handling engineering to develop customized rare earth material transport solutions. The company's team of engineers and technicians works closely with clients to understand their specific operational needs, from initial material analysis to final system integration. By focusing on the unique challenges of rare earth materials—such as their reactivity, handling sensitivity, and processing requirements—HeadPowder ensures that each system is optimized for performance, safety, and efficiency.
The company's approach to system design emphasizes modularity and scalability, allowing clients to start with a basic system and expand as their operations grow. This flexibility is particularly valuable for businesses in the rare earth industry, which often face fluctuating demand and evolving processing technologies. HeadPowder's commitment to innovation and quality has made it a trusted partner for companies seeking reliable and efficient rare earth material handling solutions.