

Principle and Working Scene Characteristics of Phosphate Fertilizer Powder Material Handling System
Phosphate fertilizer powder, a critical component in modern agricultural practices, requires efficient and reliable material handling solutions to ensure smooth production and distribution processes. The equipment designed for transporting phosphate fertilizer powder must address specific challenges such as dust control, material flow uniformity, and operational durability. This article explores the underlying principles of phosphate fertilizer powder material handling systems, alongside the key working scene characteristics that define their effectiveness in industrial applications.
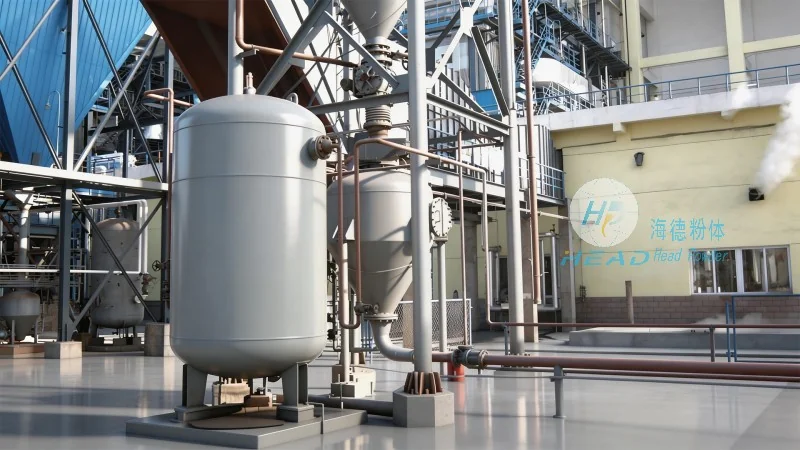
Core Principles of Phosphate Fertilizer Powder Handling Equipment
The fundamental principle of phosphate fertilizer powder material handling systems revolves around the efficient transfer of fine powders while minimizing operational risks. Key components include feeders, conveyors, and control systems engineered to handle the unique properties of phosphate fertilizer powder, which often involves high moisture content, abrasive particles, and potential for dust generation. The design of these systems prioritizes material flow consistency, ensuring that the powder moves uniformly through the handling process without clogging or degradation. Additionally, dust suppression mechanisms are integrated to comply with environmental regulations and maintain workplace safety. The equipment’s durability is enhanced through materials resistant to corrosion and wear, such as stainless steel or specialized coatings, which are essential for long-term performance in demanding industrial environments.
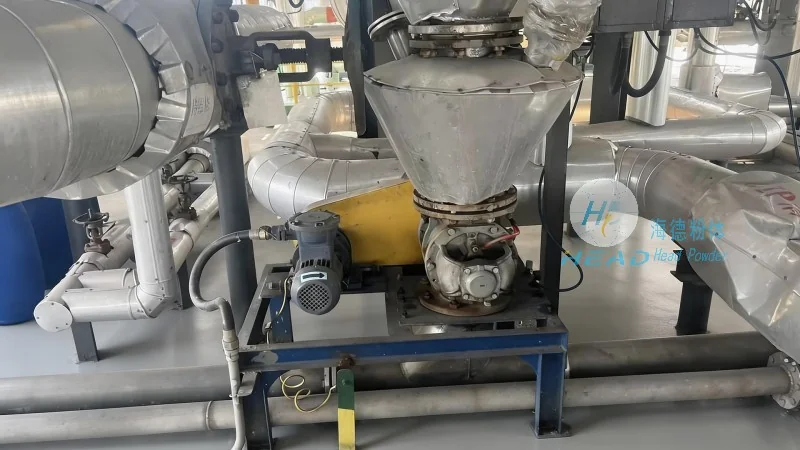
Working Scene Characteristics of Phosphate Fertilizer Powder Handling Systems
The operational characteristics of phosphate fertilizer powder handling systems are tailored to specific industrial settings, including fertilizer production plants, storage facilities, and distribution centers. In production environments, these systems are typically integrated into continuous processing lines, where they handle raw phosphate materials and intermediate products. The working scene often involves high throughput rates, requiring robust conveyor systems capable of maintaining consistent material flow rates. Storage facilities, on the other hand, utilize these systems for bulk storage and transfer, emphasizing reliability and low maintenance to minimize downtime. Distribution centers may employ these systems for packaging and shipping, where precision and speed are critical to meet customer demands. The working scene also considers environmental factors, such as temperature and humidity, which can affect powder properties and system performance. Adaptive control systems are often incorporated to adjust operational parameters in response to changing conditions, ensuring optimal performance under varying industrial scenarios.
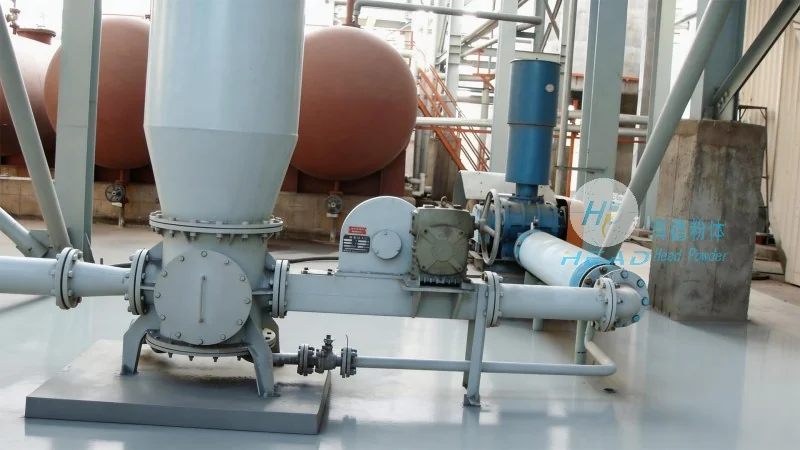
Key Features and Advantages of Phosphate Fertilizer Powder Handling Equipment
Phosphate fertilizer powder handling systems from Shandong HeadPowder Engineering Co., Ltd. (headpowder) offer several advantages that enhance operational efficiency and reliability. The company specializes in designing customized solutions that address the unique needs of phosphate fertilizer production, ensuring that each system is tailored to specific production scales and material characteristics. The equipment incorporates advanced control technologies, such as variable frequency drives (VFDs), which allow for precise speed adjustments to maintain optimal material flow. This not only improves efficiency but also reduces energy consumption, contributing to cost savings for industrial operations. Additionally, the systems are equipped with monitoring and diagnostic tools that provide real-time data on performance, enabling proactive maintenance and reducing unexpected downtime. The use of high-quality materials and rigorous manufacturing processes ensures that the equipment meets international standards for safety and performance, providing long-term value to clients. The working scene characteristics of these systems are further enhanced by their adaptability to different production environments, making them suitable for both large-scale industrial applications and smaller-scale operations.