

Principles and Working Scene Characteristics of Capsule Powder Pneumatic Conveying
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a professional enterprise dedicated to the research, development, and application of advanced powder handling technologies. With its headquarters located in Shandong, China, the company specializes in providing innovative solutions for the efficient and reliable transportation of powder materials, particularly through pneumatic conveying systems. HeadPowder's expertise lies in optimizing material flow, ensuring product integrity, and enhancing operational efficiency for various industrial applications.
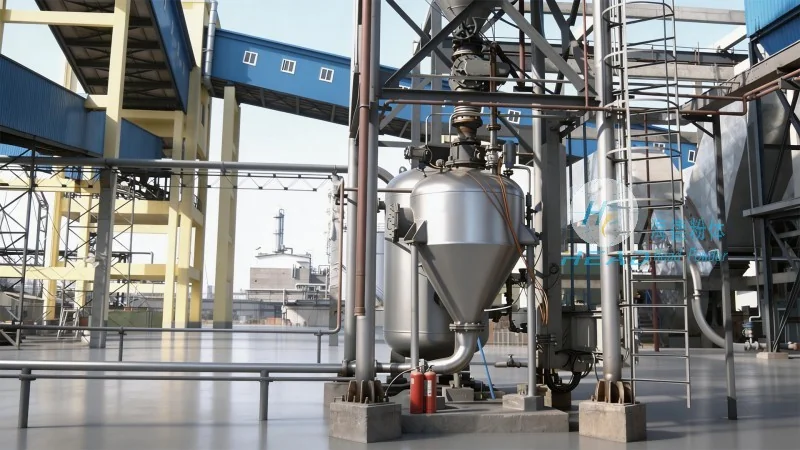
Principles of Capsule Powder Pneumatic Conveying
Capsule powder pneumatic conveying is a sophisticated method of transporting dry powder materials using compressed air or other gas streams. The core principle involves the creation of a low-pressure or high-pressure environment that draws or pushes the powder particles through a pipeline system. In this process, the powder is typically enclosed within a "capsule" or a controlled flow structure, which helps maintain uniform particle distribution and prevents segregation or agglomeration. The system operates by generating a pressure differential between the inlet and outlet of the conveying line, allowing the powder to be moved from the source to the destination. Key components include the feed hopper, air compressor, conveying line, and discharge equipment, each playing a critical role in ensuring smooth and consistent material transport. The technology leverages the principles of fluidization and gas-solid interaction to achieve efficient conveying, with the capsule design enhancing the stability and reliability of the process.
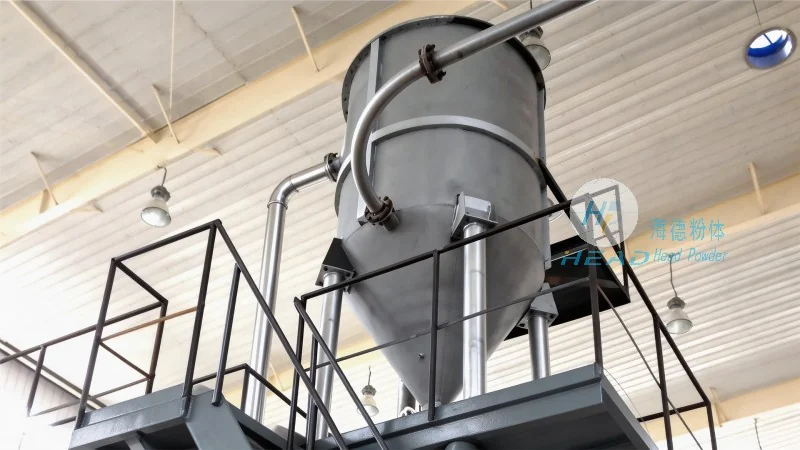
Working Scene Characteristics of Capsule Powder Pneumatic Conveying
The working scene characteristics of capsule powder pneumatic conveying are tailored to meet the diverse needs of industrial applications, offering several distinct advantages over traditional conveying methods. One of the primary characteristics is its ability to handle a wide range of powder types, including fine, cohesive, or abrasive materials, which are often challenging to transport using conventional systems. The capsule design minimizes particle degradation and maintains product quality, making it suitable for sensitive or high-value powders such as pharmaceuticals, food ingredients, and specialty chemicals. Another key characteristic is the system's flexibility in terms of layout and integration. It can be adapted to various plant configurations, from compact installations in small-scale operations to extensive networks in large industrial facilities. The conveying process is also highly customizable, allowing for adjustments in flow rate, pressure, and particle size to optimize performance. Additionally, the system provides real-time monitoring and control capabilities, enabling operators to track material flow, detect blockages, and adjust parameters dynamically. This adaptability and control make capsule powder pneumatic conveying an ideal solution for applications requiring precise material handling and consistent product quality.
Typical Working Scenarios
HeadPowder's capsule powder pneumatic conveying systems are widely used in various industrial sectors, demonstrating their versatility and effectiveness in real-world applications. In the pharmaceutical industry, for example, the system is employed to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the powders remain sterile and free from contamination. The capsule design helps maintain the integrity of these sensitive materials, while the controlled conveying process minimizes the risk of particle agglomeration or degradation. In the food and beverage sector, the technology is utilized for handling powders like cocoa, milk powder, and flavorings, where maintaining product freshness and preventing caking is crucial. The system's ability to handle cohesive powders without causing clumping makes it suitable for food processing plants. Similarly, in the chemical industry, capsule powder pneumatic conveying is used for transporting fine chemicals, pigments, and catalysts, where the need for consistent particle size and purity is paramount. The system's robust design and ability to handle abrasive materials ensure long-term operational reliability, reducing maintenance costs and downtime. These examples illustrate how the working scene characteristics of capsule powder pneumatic conveying align with the specific requirements of different industries, providing tailored solutions that enhance productivity and product quality.
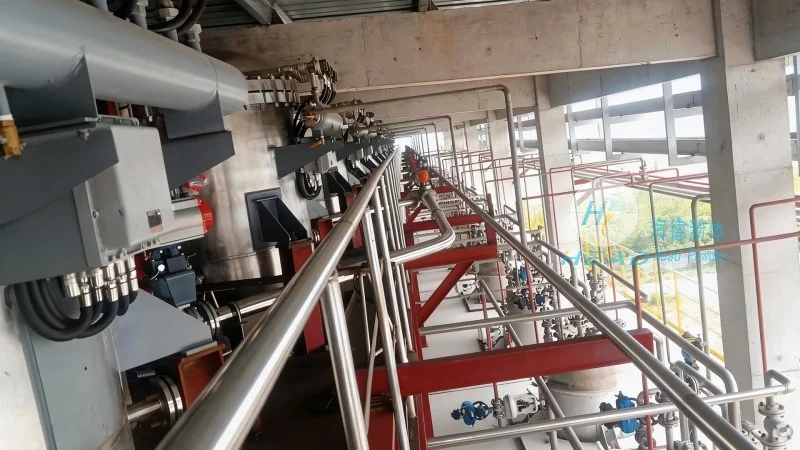
Advantages in Practical Applications
When considering the practical implementation of capsule powder pneumatic conveying, several key advantages emerge that make it a preferred choice for many industries. Firstly, the system offers high efficiency in material transport, with the ability to move large quantities of powder over long distances with minimal energy consumption compared to other methods like bulk handling or manual transfer. The capsule design optimizes the flow of powder, reducing pressure losses and improving overall system performance. Secondly, the technology provides excellent product protection, as the enclosed capsule prevents exposure to external contaminants and maintains the original properties of the powder. This is particularly important for applications where product quality is non-negotiable, such as in pharmaceutical and food industries. Thirdly, the system is highly adaptable and scalable, allowing it to be integrated into existing production lines or expanded to accommodate growing production needs. The modular design of the components enables easy installation and maintenance, reducing the overall operational complexity. Additionally, the real-time monitoring and control features enhance operational safety and reliability, allowing operators to quickly address any issues that may arise during the conveying process. These advantages collectively contribute to improved productivity, reduced costs, and enhanced product quality, making capsule powder pneumatic conveying a reliable and efficient solution for modern industrial applications.