

Principles and Application Scenarios of Fully Automatic Powder Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced powder handling solutions. Among their portfolio is the fully automatic powder pneumatic conveying system, a technology that revolutionizes the efficient and safe transport of bulk powders in various industrial settings. This system integrates cutting-edge automation and control technologies to ensure reliable, high-performance material transfer while minimizing operational risks and downtime.
Principles of Operation for the Fully Automatic Powder Pneumatic Conveying System
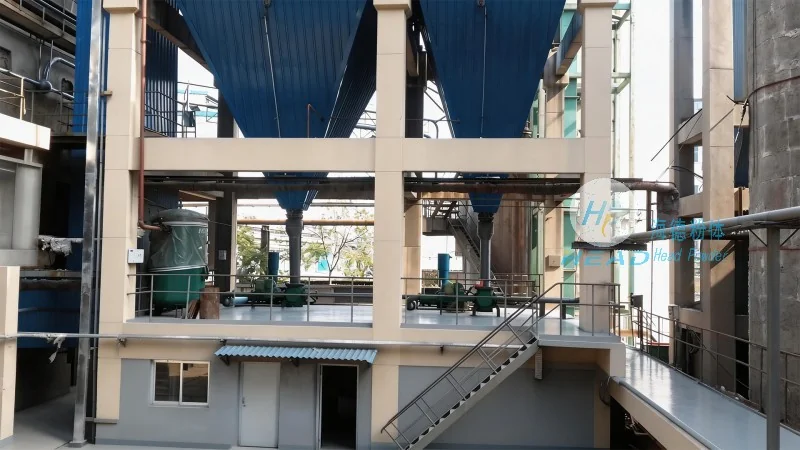
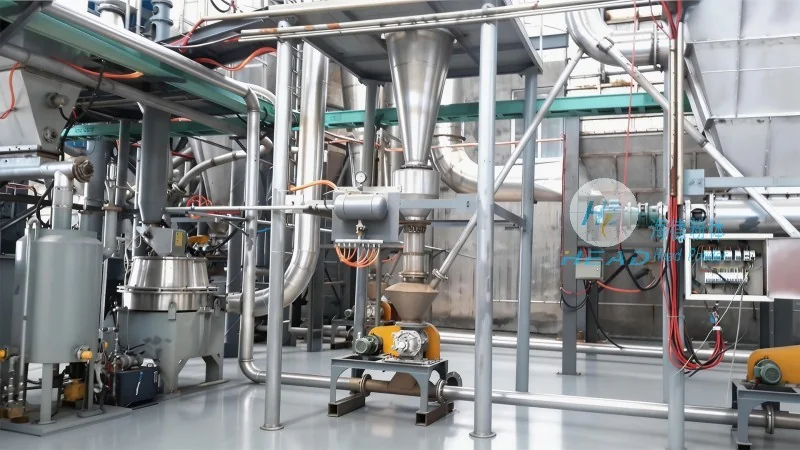
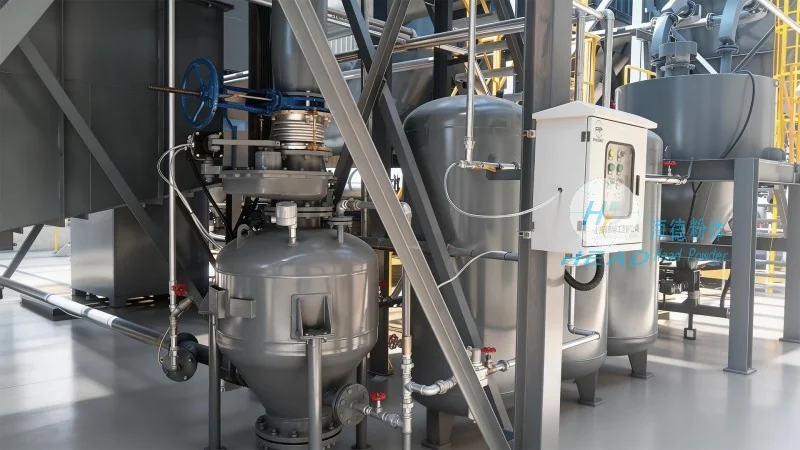
The core principle of the fully automatic powder pneumatic conveying system lies in the use of compressed air to move dry powders through a network of pipes and components. The system operates by creating a pressure differential between the inlet and outlet points, which propels the powder particles along the conveying line. Key components include a hopper for material storage, a rotary valve for controlled discharge, a compressor to generate the necessary air pressure, and a filter system to maintain air quality and prevent dust contamination. The automation aspect is achieved through programmable logic controllers (PLCs) and sensors that monitor flow rates, pressure, and particle density in real-time, adjusting system parameters to optimize performance and ensure consistent material transport.
Key Features and Advantages of the System
One of the standout features of this system is its fully automated operation, which eliminates the need for manual intervention during the conveying process. This not only enhances operational efficiency but also reduces labor costs and human error. The system is designed with robust materials to withstand the abrasive nature of many powders, ensuring long-term durability and minimal maintenance requirements. Additionally, the integration of advanced sensors allows for real-time monitoring and data logging, enabling predictive maintenance and proactive troubleshooting. The compact design of the system makes it suitable for installation in various industrial environments, from manufacturing plants to food processing facilities, without requiring extensive space or infrastructure modifications.
Application Scenarios and Industry Use Cases
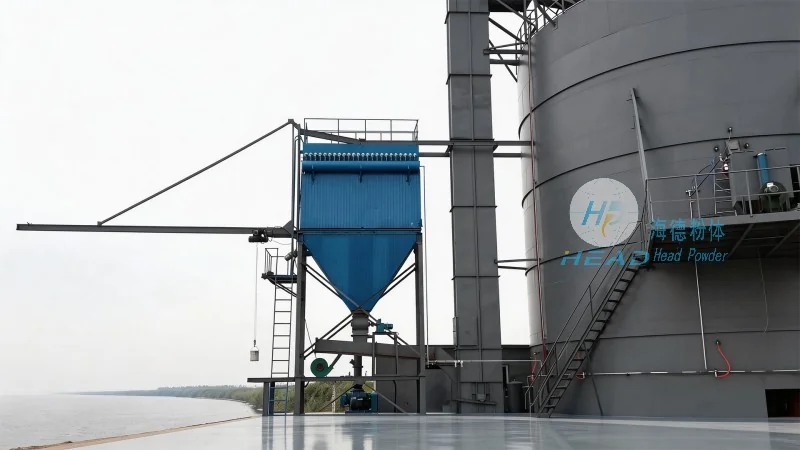
The fully automatic powder pneumatic conveying system is versatile and can be applied across a wide range of industries where bulk powder handling is critical. In the pharmaceutical industry, for example, the system ensures sterile and contamination-free transport of active pharmaceutical ingredients (APIs) and excipients, adhering to stringent regulatory standards. In the food and beverage sector, it facilitates the efficient movement of powders such as flour, sugar, and cocoa, maintaining product quality and hygiene. The chemical industry benefits from the system's ability to handle abrasive and corrosive powders, while the mining sector utilizes it for transporting ore and mineral powders from processing plants to storage or further processing facilities. Each application leverages the system's ability to maintain consistent flow rates, control particle size distribution, and minimize material degradation during transport.
Customization and Integration Capabilities
HeadPowder understands that each industrial operation has unique requirements, and thus offers customizable solutions tailored to specific needs. The fully automatic powder pneumatic conveying system can be integrated with existing production lines or designed as a standalone unit, depending on the client's infrastructure and operational goals. The company's engineering team works closely with clients to assess their material characteristics, conveying distances, and throughput requirements, then develops a system configuration that maximizes efficiency and cost-effectiveness. This includes selecting appropriate pipe diameters, air pressure levels, and component materials to match the specific powder being handled. Furthermore, the system can be equipped with additional features such as dust collection systems, material weighing scales, and remote monitoring capabilities to enhance overall operational control and safety.
Conclusion and Future Outlook
As industries continue to demand more efficient and reliable powder handling solutions, the fully automatic powder pneumatic conveying system from HeadPowder stands out as a cutting-edge technology that addresses these needs. By combining advanced automation, robust engineering, and versatile application capabilities, the system provides a sustainable and cost-effective solution for transporting bulk powders in various industrial applications. With its headquarters in Shandong, China, HeadPowder remains committed to delivering high-quality engineering services and innovative solutions that meet the evolving demands of modern industry, ensuring that their fully automatic powder pneumatic conveying systems remain at the forefront of powder handling technology.