

Principle and Working Scene Characteristics of Air-Driven Conveyor for Sponge Sand Materials
HeadPowder, a leading provider in material handling solutions, specializes in air-driven conveyor systems designed for the efficient transport of sponge sand and similar granular materials. These systems leverage pneumatic technology to move bulk materials through pipelines using compressed air, offering a versatile and reliable method for industrial applications. The air-driven conveyor for sponge sand materials is engineered to handle the unique properties of sponge sand, such as its light weight, irregular shape, and potential for dust generation, ensuring optimal performance in various operational environments.
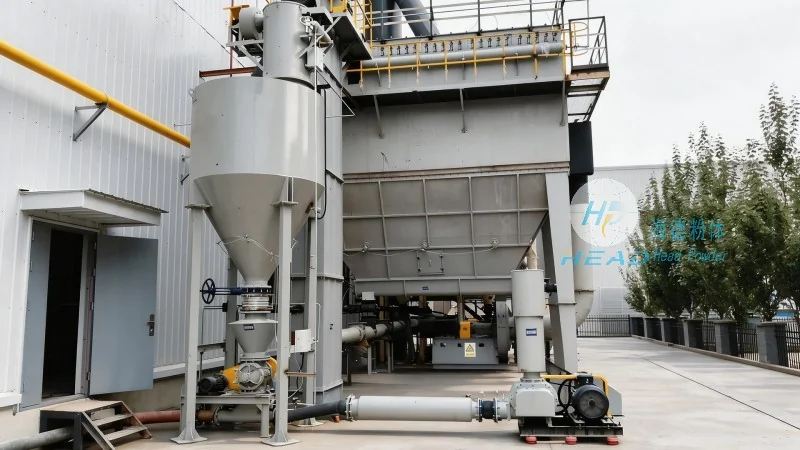
The Principle of Air-Driven Conveying for Sponge Sand
The core principle of air-driven conveying for sponge sand materials involves the use of a positive pressure or negative pressure system to transport particles through a sealed pipeline. In a positive pressure system, compressed air is introduced at the inlet, creating a pressure differential that propels the material forward. The sponge sand particles are suspended in the air stream, moving from the loading point to the discharge point. This method is particularly effective for short to medium-distance transport and can handle a wide range of material types, including those with high moisture content or abrasive characteristics. The negative pressure system, on the other hand, draws material into the pipeline using a vacuum at the discharge end, which is useful for applications requiring material to be collected from multiple points and transported to a central location.
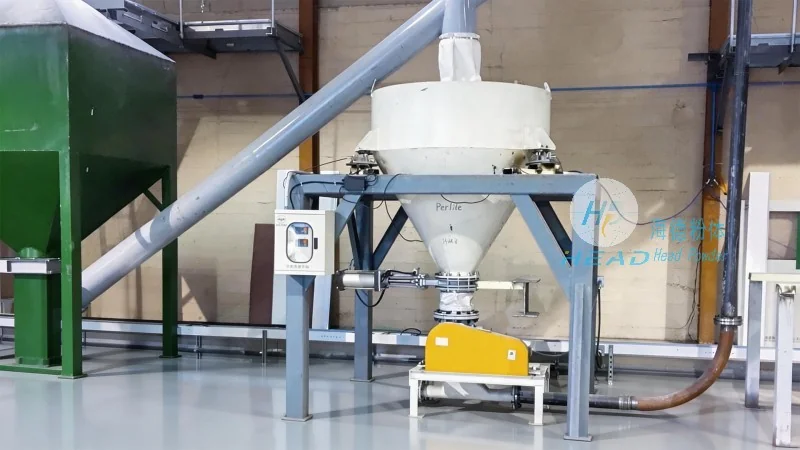
Key Working Scene Characteristics of the System
The air-driven conveyor for sponge sand materials exhibits several distinct working scene characteristics that make it suitable for diverse industrial settings. Firstly, its ability to operate in a dust-free environment is a significant advantage, as sponge sand is often prone to generating fine particles that can cause respiratory issues or equipment wear. The sealed pipeline design minimizes dust dispersion, enhancing workplace safety and compliance with environmental regulations. Secondly, the system's flexibility in layout is notable; it can be installed in straight or curved configurations, allowing for integration into existing production lines without extensive modifications. This adaptability is crucial for facilities with limited space or complex material flow requirements. Thirdly, the energy efficiency of the air-driven conveyor is a key operational characteristic. By using compressed air as the primary power source, the system reduces the need for mechanical components like belts or chains, which can wear out over time and require frequent maintenance. This results in lower operational costs and increased uptime for the equipment.
Applications and Operational Benefits
The air-driven conveyor for sponge sand materials is widely used in various industrial sectors, including construction, foundries, and manufacturing plants. In construction, it is employed to transport sand and other aggregates from storage silos to mixing stations, ensuring a consistent supply of materials for concrete production. The system's ability to handle large volumes of material at a steady rate enhances production efficiency and reduces downtime. In foundries, the conveyor is used to move molten metal or sand molds, where precision and speed are critical. The positive pressure system is often preferred in these applications due to its ability to maintain a consistent flow rate, preventing material blockages or uneven distribution. Additionally, the system's low maintenance requirements make it ideal for high-volume operations, as it reduces the need for regular servicing and repairs.
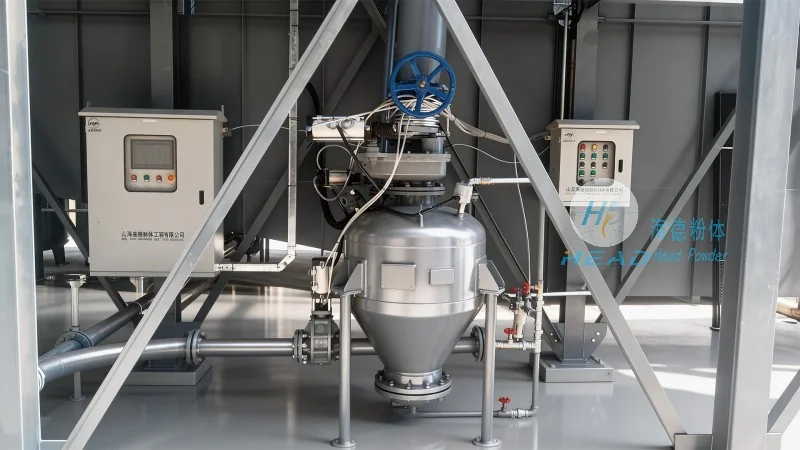
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the manufacturer of the air-driven conveyor for sponge sand materials, is a reputable company based in Shandong, China. With years of experience in the material handling industry, HeadPowder has developed a range of products tailored to meet the specific needs of its clients. The company's commitment to quality and innovation is reflected in its state-of-the-art manufacturing facilities and rigorous quality control processes. HeadPowder's air-driven conveyor systems are designed to be durable, efficient, and easy to maintain, ensuring long-term performance and customer satisfaction. The company's location in Shandong provides easy access to major transportation networks, facilitating the delivery of products to clients across the region and beyond.