

Introduction to Powder Explosive Pneumatic Conveying System Equipment and Structural Principles
Headpowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer based in Shandong, China. The company specializes in the development and production of pneumatic conveying systems, particularly for handling powder explosive materials. With a strong focus on safety and efficiency, Headpowder has built a reputation for delivering high-quality equipment that meets the demands of various industries, including explosives manufacturing, fireworks production, and chemical processing.
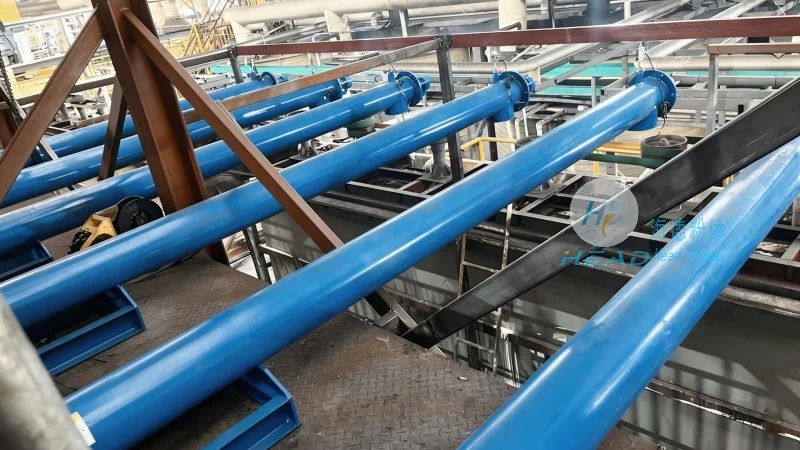
Introduction to Pneumatic Conveying Systems for Powder Explosives
Pneumatic conveying systems are critical for the safe and reliable transportation of powder explosive materials. These systems utilize compressed air or other gases to move powders through a sealed pipeline network, eliminating the need for mechanical components that could introduce sparks or other ignition sources. The equipment is engineered to handle sensitive materials like ammonium nitrate, nitroguanidine, and other pyrotechnic powders, ensuring compliance with strict safety regulations and industry standards. By using pneumatic conveying, companies can reduce the risk of accidents, improve operational efficiency, and maintain a clean working environment.
Key Components and Structural Principles
The fundamental components of a powder explosive pneumatic conveying system include the hopper, feeder, air compressor, pipeline system, and receiver. The hopper serves as the primary storage vessel, providing a controlled space for the powder to be held before transport. The feeder, typically a rotary valve or a screw feeder, regulates the flow of powder into the system, ensuring a consistent and controlled discharge rate. The air compressor generates the necessary pressure to create a high-velocity air stream that propels the powder particles through the pipeline. The pipeline network, constructed from stainless steel or other corrosion-resistant materials, is designed to withstand the pressures and temperatures associated with powder transport. The receiver collects the powder at the destination point, allowing for the separation of the powder from the air stream and the subsequent collection of the material.
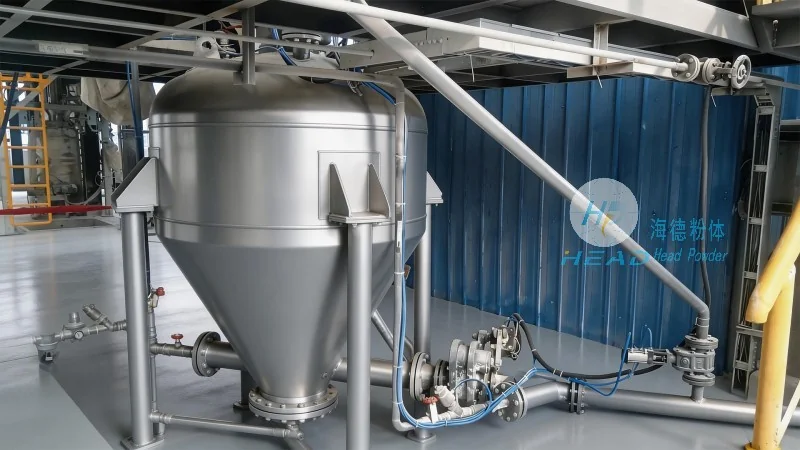
Working Principle of the System
The operation of the pneumatic conveying system begins with the powder being discharged from the hopper into the feeder. The feeder then meters the powder at a predetermined rate, ensuring a steady flow into the pipeline. Simultaneously, the air compressor produces a high-pressure air stream, which is introduced into the pipeline. This air stream creates a flow that carries the powder particles, forming a mixture known as a slurry. The slurry travels through the pipeline to the receiver, where the air is separated from the powder. The powder is collected in a container, while the air is either discharged or recycled back into the system for further use. The entire process is controlled by a series of valves and sensors that monitor pressure, flow rate, and other critical parameters to ensure optimal performance and safety.
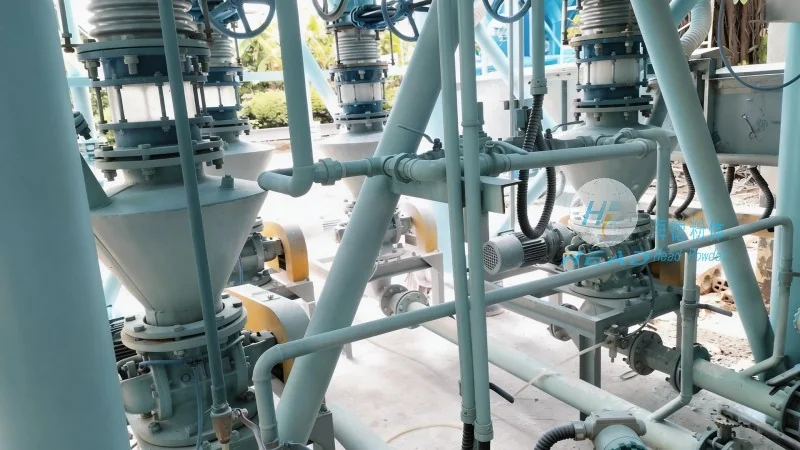
Advantages of Pneumatic Conveying for Powder Explosives
Implementing pneumatic conveying systems for powder explosives offers several key advantages. Firstly, it significantly enhances safety by eliminating the risk of mechanical friction or impact that could lead to ignition. The sealed pipeline system prevents dust from escaping into the environment, reducing the risk of dust explosions. Secondly, the system provides precise control over the flow rate and pressure, allowing for consistent and reliable material transport. This precision is crucial for maintaining the quality of the final product and ensuring that production processes run smoothly. Thirdly, the equipment is compact and can be customized to fit the specific layout and space constraints of a facility, making it suitable for both new installations and retrofitting existing systems. Additionally, the systems are designed for easy maintenance and operation, reducing downtime and increasing overall productivity.
Applications and Industry Standards
Powder explosive pneumatic conveying systems are widely utilized in the manufacturing of commercial explosives, industrial fireworks, and other pyrotechnic products. The systems are essential for moving raw materials such as nitrate-based powders and other reactive substances from storage to processing areas without compromising safety. Headpowder's equipment adheres to international safety standards, including ATEX for equipment used in potentially explosive atmospheres and ISO certifications for quality management. The company also provides comprehensive technical support, including system design, installation, and maintenance services, to ensure that clients can operate their systems safely and efficiently. By partnering with Headpowder, companies can enhance their operational safety, improve production efficiency, and meet the stringent regulatory requirements of the industry.