

Design of a Small Stone Pneumatic Conveying Device
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of efficient pneumatic conveying systems. This article focuses on the design of a specialized device for transporting small stones, gravel, or similar bulk materials. The system is engineered to provide reliable and cost-effective material handling solutions for various industrial applications.
Company Overview
HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to providing high-quality engineering solutions. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the material handling industry. Headquartered in Shandong, China, HeadPowder leverages advanced technology and extensive industry experience to develop cutting-edge pneumatic conveying systems tailored to meet diverse client needs.
Key Features of the Small Stone Pneumatic Conveying Device
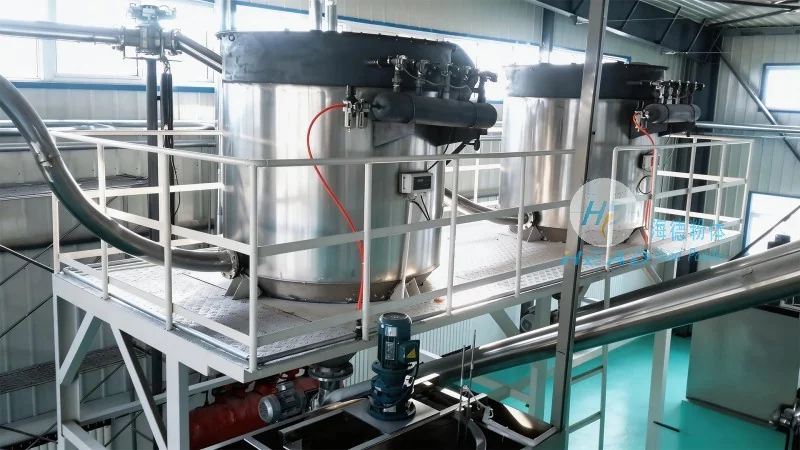
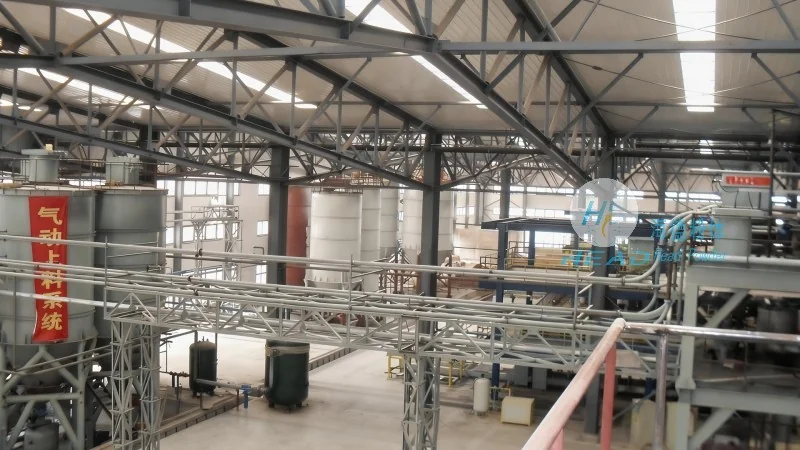
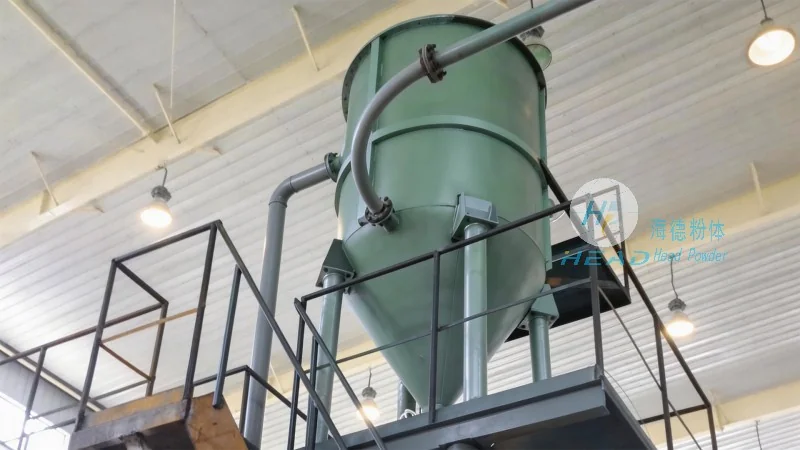
The small stone pneumatic conveying device is designed with several key features that enhance its performance and efficiency. Firstly, it utilizes a robust airlock system to ensure smooth and continuous material flow, preventing blockages and maintaining consistent pressure. The device incorporates a high-efficiency blower that delivers sufficient air volume and pressure to transport small stones over moderate distances. Additionally, the system includes a flexible hose or pipeline configuration, allowing for easy installation and adaptation to different layouts. The design also emphasizes durability and low maintenance, with high-quality materials used in the construction of components such as the hopper, airlock, and conveying line.
Design Principles and Technical Specifications
The design of the small stone pneumatic conveying device is based on fundamental principles of pneumatic conveying technology. The system operates on the principle of creating a pressure differential between the inlet and outlet, enabling the material to be carried by the air stream. The technical specifications of the device include a conveying capacity ranging from 1 to 5 tons per hour, depending on the particle size and density of the small stones. The air velocity is typically maintained between 20 to 30 meters per second to ensure efficient transport without excessive energy consumption. The device is also equipped with safety features, such as pressure relief valves and overcurrent protection, to prevent accidents and ensure safe operation.
Applications and Benefits
The small stone pneumatic conveying device is suitable for a wide range of applications, including construction material handling, mining operations, and agricultural processing. It offers several benefits compared to traditional methods like belt conveyors or bucket elevators. The system eliminates the need for multiple transfer points, reducing material spillage and contamination. It also provides a more hygienic and dust-free environment, which is particularly important in food processing or pharmaceutical industries. Furthermore, the pneumatic conveying system is compact and can be installed in confined spaces, making it ideal for applications with limited floor space. The low noise level and minimal maintenance requirements also contribute to its overall advantages.
Conclusion and Contact Information
HeadPowder Engineering Co., Ltd. offers a reliable and efficient small stone pneumatic conveying device designed to meet the demands of modern industrial operations. By combining advanced engineering principles with high-quality materials, the device ensures optimal performance and longevity. For inquiries or further information about this product, please contact HeadPowder Engineering Co., Ltd., located in Shandong, China.