

What is an Automatic Quantitative Bulk Material Pneumatic Conveying Machine? What is its Design Prin
When it comes to efficient and reliable material handling in industrial settings, the automatic quantitative bulk material pneumatic conveying machine stands out as a critical solution. This equipment is designed to transport bulk powders and granules with precision, ensuring consistent flow rates and accurate material delivery. The following article explores the functionality, design principles, and key features of such machines, highlighting their importance in modern industrial operations.
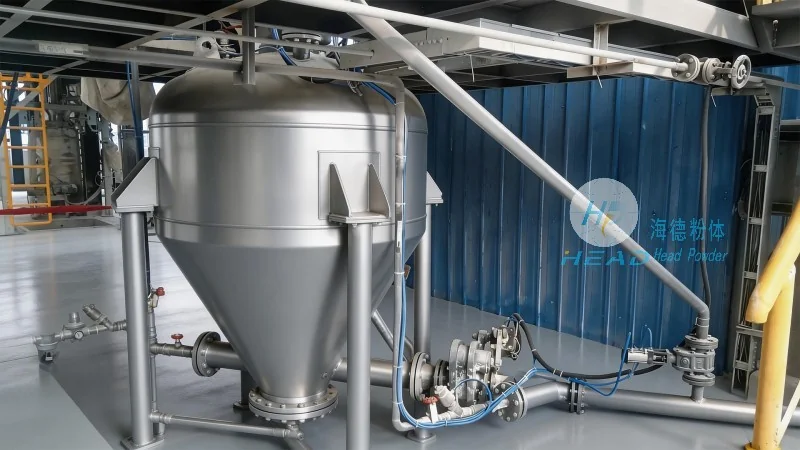
Understanding the Role of Pneumatic Conveying Systems
Pneumatic conveying machines utilize air or gas to move bulk materials from one location to another. Unlike traditional mechanical conveyors, these systems offer flexibility in layout and can handle a wide range of materials, including fine powders, coarse granules, and even abrasive substances. The automatic quantitative variant enhances this capability by integrating advanced control mechanisms that regulate the flow rate and quantity of material being transported. This precision is crucial in applications where exact dosing and consistent material supply are non-negotiable, such as in pharmaceutical manufacturing, food processing, and chemical production.
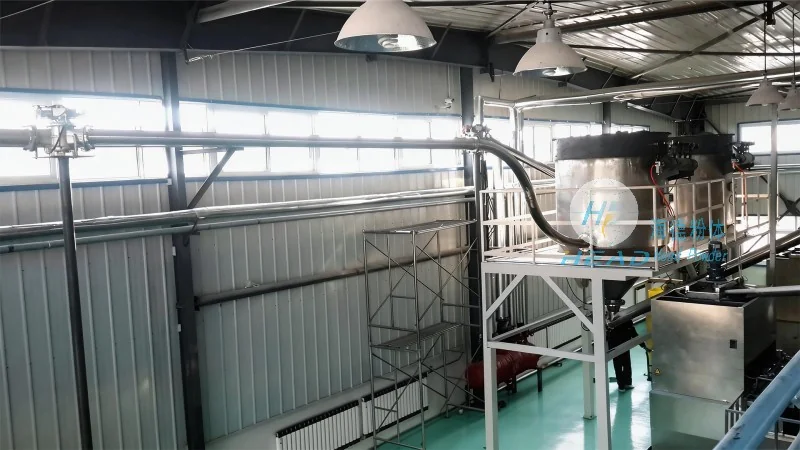
The Core Design Principles of Automatic Quantitative Pneumatic Conveying Machines
The design of an automatic quantitative bulk material pneumatic conveying machine is built on several fundamental principles aimed at optimizing performance and reliability. First, the system relies on a combination of pressure and vacuum to move materials through a network of pipes. The machine typically includes a hopper for material storage, a feeder to control the flow rate, and a conveying line that transports the material to the discharge point. The quantitative aspect is achieved through sophisticated control systems, often incorporating sensors and feedback mechanisms that adjust the feeder speed based on real-time conditions. This ensures that the material is delivered in precise, pre-set quantities, minimizing waste and enhancing process efficiency.
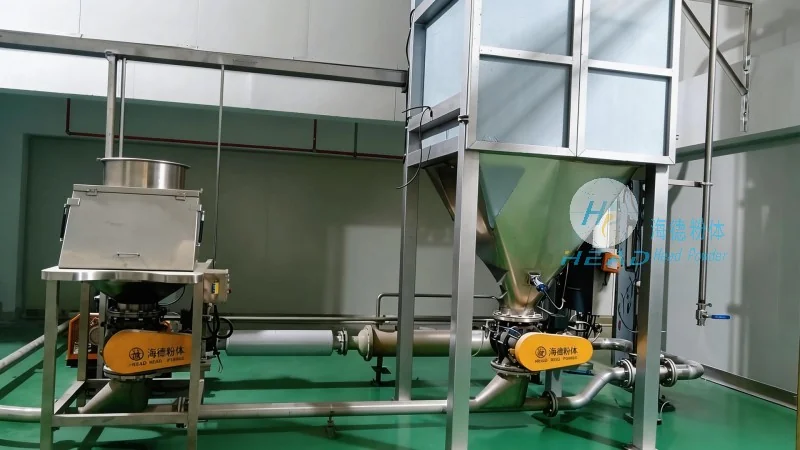
Key Components and Their Functions
Several key components work in tandem to ensure the smooth operation of an automatic quantitative pneumatic conveying machine. The hopper serves as the storage container, holding the bulk material and providing a consistent feed to the feeder. The feeder, which can be a rotary valve or a screw feeder, regulates the material flow rate, ensuring that the correct amount is introduced into the conveying line. The conveying line itself is made of durable materials, such as stainless steel or plastic, to withstand the abrasive nature of many bulk materials. The control system, which may include a PLC (Programmable Logic Controller), monitors the entire process, adjusting parameters like air pressure and feeder speed to maintain the desired flow rate. Additionally, the system may include a filter or cyclone to separate the material from the air, preventing dust accumulation and maintaining air quality.
Applications and Benefits in Industrial Settings
The automatic quantitative bulk material pneumatic conveying machine finds applications across various industries, where precise material handling is essential. In the pharmaceutical industry, for example, these machines are used to transport active pharmaceutical ingredients (APIs) and excipients with high accuracy, ensuring compliance with stringent quality standards. In food processing, they handle ingredients like flour, sugar, and spices, maintaining hygiene and preventing contamination. The chemical industry benefits from the ability to transport hazardous or sensitive materials safely and efficiently. The primary benefits of these machines include improved process control, reduced labor costs, minimized material loss, and enhanced safety due to the enclosed system that prevents dust exposure and spillage.
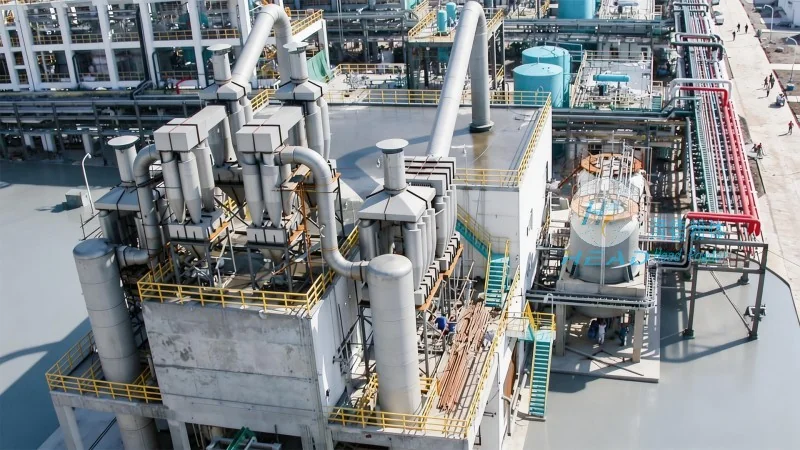
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of industrial material handling equipment. With a focus on innovation and quality, the company specializes in designing and producing pneumatic conveying systems tailored to the needs of various industries. HeadPowder's commitment to customer satisfaction and technological advancement has established it as a trusted partner in the material handling sector. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge solutions for global markets. By combining years of experience with modern engineering techniques, HeadPowder ensures that its products meet the highest standards of performance, reliability, and durability, providing customers with long-term value and operational efficiency.