

Design of a Coffee Bean Pneumatic Conveying Device
Efficient and reliable material handling is a critical aspect of modern coffee processing operations. Among the various technologies available, pneumatic conveying systems have emerged as a preferred solution for transporting coffee beans due to their ability to maintain product quality while ensuring seamless operation. This article provides an in-depth look at the design considerations and key features of a specialized coffee bean pneumatic conveying device, developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
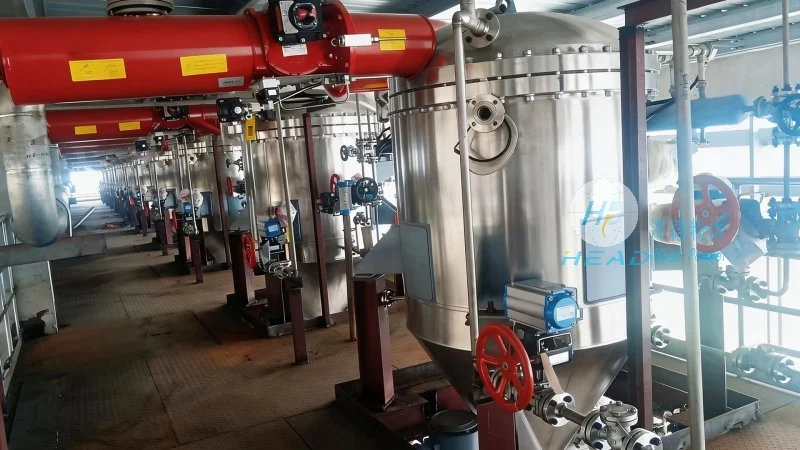
Company Profile and Background
Shandong HeadPowder Engineering Co., Ltd. is a reputable company based in Shandong, China, dedicated to providing high-quality engineering solutions for material handling and processing industries. With years of experience and a commitment to innovation, the company has established itself as a trusted partner for businesses seeking efficient and durable equipment. The company's headquarters and main operations are located in Shandong, China, where it maintains a strong presence in the domestic and international markets.
Overview of the Coffee Bean Pneumatic Conveying Device
The coffee bean pneumatic conveying device designed by HeadPowder is engineered to handle the unique characteristics of coffee beans, ensuring minimal damage and optimal flow during transportation. This system utilizes a combination of air pressure and specialized components to move coffee beans from one location to another within a processing facility. The design incorporates advanced materials and precision engineering to meet the demanding requirements of coffee processing plants.
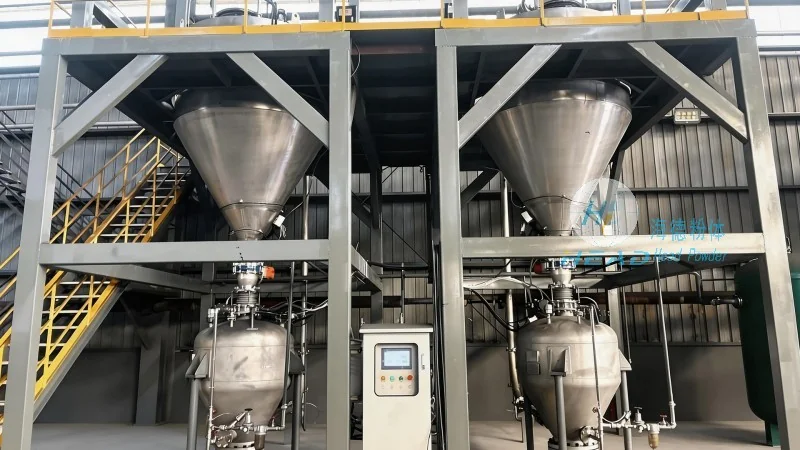
Key Design Features and Technical Specifications
The pneumatic conveying system for coffee beans includes several key components that contribute to its effectiveness. These components include a hopper for material storage, a rotary valve for controlled discharge, a pipeline system with appropriate diameter and material, and a dust collection unit to maintain air quality. The system operates on a pressure or vacuum principle, depending on the specific application requirements. The design ensures that coffee beans are conveyed gently, preventing breakage and maintaining their quality attributes such as aroma and flavor. The system is also equipped with monitoring and control features to ensure consistent performance and ease of operation.
Advantages of the Pneumatic Conveying Solution
Implementing a pneumatic conveying system for coffee bean transport offers several advantages over traditional methods. Firstly, it eliminates the need for mechanical components like conveyors or elevators, reducing the risk of product contamination and damage. Secondly, the system provides a closed environment, which helps in maintaining hygiene standards and preventing dust exposure. Thirdly, the design allows for flexible layout configurations, enabling easy integration into existing processing facilities. Additionally, the system offers energy efficiency and low maintenance requirements, contributing to long-term cost savings for coffee processing businesses.
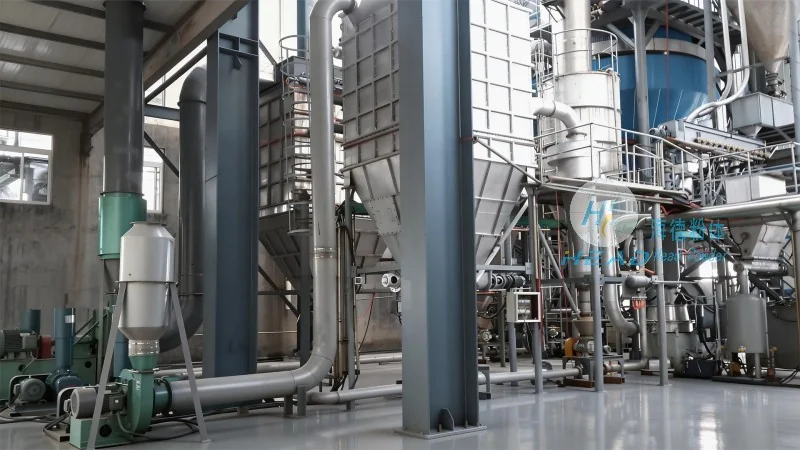
Application in Coffee Processing Facilities
The coffee bean pneumatic conveying device is widely used in various stages of coffee processing, from raw bean reception to roasting and packaging. In the reception area, the system efficiently transports incoming coffee beans from storage silos or trucks to processing areas. During the roasting process, the device can be used to move roasted beans to cooling and packaging sections. The system's ability to handle different types of coffee beans, including green, roasted, and ground varieties, makes it a versatile solution for diverse processing needs. Its gentle handling characteristics are particularly beneficial for specialty coffee beans, which require careful handling to preserve their unique characteristics.
Conclusion and Future Developments
Shandong HeadPowder Engineering Co., Ltd.'s coffee bean pneumatic conveying device represents a significant advancement in material handling technology for the coffee industry. By combining innovative design with robust engineering, the system addresses the specific challenges of coffee bean transport, ensuring efficiency, quality, and reliability. As the coffee industry continues to grow and evolve, such specialized equipment will play an increasingly important role in optimizing processing operations. HeadPowder remains committed to developing cutting-edge solutions that meet the changing needs of the industry, providing customers with reliable and efficient equipment for their coffee processing requirements.