

Working Principle and Features of a Coal Fly Ash Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, production, and installation of advanced pneumatic conveying systems for industrial applications. The company's core product, the coal fly ash pneumatic conveying line, is engineered to efficiently transport coal fly ash, a byproduct of coal combustion, from its source to various processing or disposal locations. This system represents a critical solution for managing coal fly ash, which is often used in construction materials, cement production, or other industrial processes.
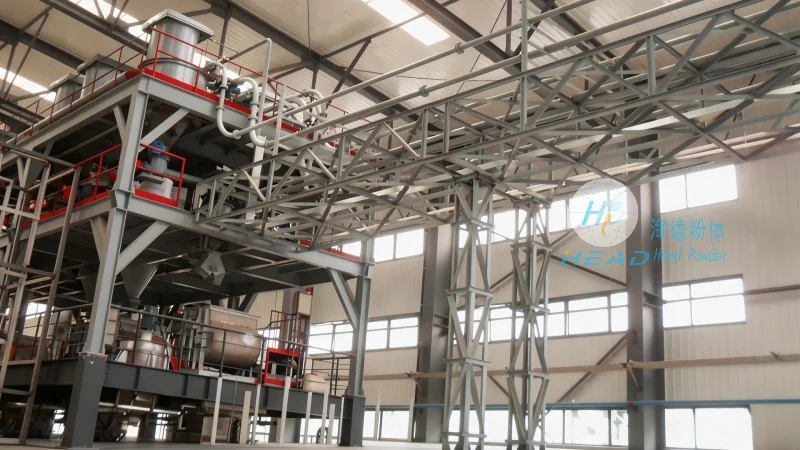
Working Principle of the Coal Fly Ash Pneumatic Conveying System
The coal fly ash pneumatic conveying system operates on the principle of pneumatic transport, utilizing air as the medium to move solid particles through a pipeline. The system typically consists of a dust collector, a conveying pipeline, a control system, and a discharge device. The process begins with the collection of coal fly ash from the source, such as a boiler or storage silo. The ash is then fed into the conveying pipeline via a feeder, which may be a rotary valve or a screw feeder. Compressed air, generated by a blower or a fan, is introduced into the pipeline, creating a flow that carries the ash particles forward. The air velocity within the pipeline is maintained at a level sufficient to keep the ash in suspension, preventing clogging and ensuring smooth transport. The conveying line may include bends, vertical sections, and horizontal runs, with appropriate fittings and valves to control the flow direction and pressure. At the destination, the ash is discharged through a receiver or a silo, where the air is separated from the solid particles using a cyclone or a filter. The separated air is then returned to the system or released to the atmosphere, while the ash is collected for further use or disposal.
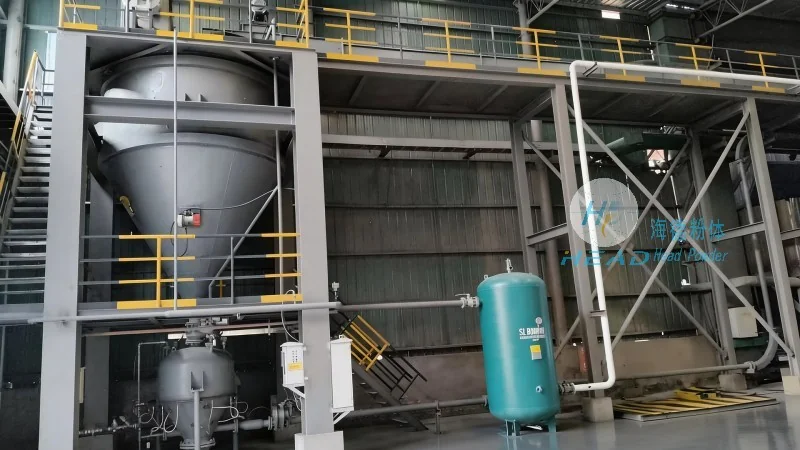
Key Features of the Coal Fly Ash Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd.'s coal fly ash pneumatic conveying line is designed with several notable features that enhance its performance and reliability. First, the system offers high efficiency in ash transport, with the ability to handle large volumes of coal fly ash over long distances. The use of compressed air ensures a consistent and controlled flow, minimizing the risk of blockages and ensuring that the ash reaches its destination without degradation. Second, the system is equipped with advanced control systems that allow for real-time monitoring and adjustment of the conveying parameters. This includes pressure monitoring, flow rate control, and alarm systems that alert operators to any issues, such as pressure drops or air leaks. Third, the equipment is constructed from high-quality materials, such as stainless steel or corrosion-resistant alloys, to withstand the abrasive nature of coal fly ash and the harsh operating conditions. This ensures a long service life and minimal maintenance requirements. Fourth, the system is designed for flexibility, allowing for easy integration with existing industrial facilities and the ability to adapt to varying ash feed rates. Additionally, the system is energy-efficient, with optimized air consumption and minimal power usage, reducing operational costs for the end-user. Finally, the company provides comprehensive after-sales support, including installation, commissioning, and maintenance services, ensuring that the system operates at peak performance throughout its lifecycle.
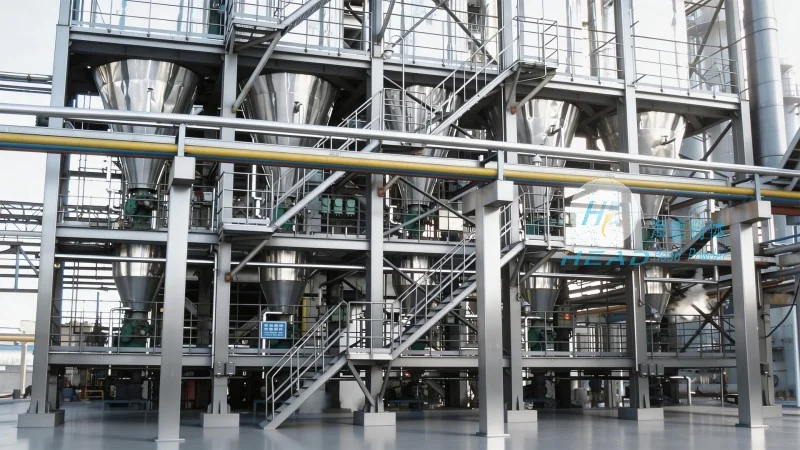
Applications and Benefits of the Coal Fly Ash Pneumatic Conveying System
The coal fly ash pneumatic conveying system is widely used in various industrial sectors, including power plants, cement factories, and construction material manufacturers. In power plants, the system is used to transport ash from the boiler to storage silos or to other processing units, where it can be used as a raw material for cement production. In cement factories, the ash is often blended with clinker to produce high-quality cement, reducing the need for natural raw materials and lowering production costs. The system also finds applications in the production of lightweight aggregates, insulation materials, and other construction products. The benefits of using this system include improved safety, as it eliminates the need for manual handling of ash, which can be hazardous. It also reduces environmental impact by preventing dust emissions and ensuring that the ash is transported in a controlled manner. Furthermore, the system enhances operational efficiency by automating the ash transport process, reducing labor costs and increasing production throughput. The reliability and durability of the system ensure consistent performance, minimizing downtime and maintenance expenses. Overall, the coal fly ash pneumatic conveying line from Shandong HeadPowder Engineering Co., Ltd. provides a cost-effective and environmentally friendly solution for managing coal fly ash, supporting sustainable industrial practices.