

Introduction to High Temperature Fly Ash Pneumatic Conveying Systems: Structure and Working Principl
High temperature fly ash pneumatic conveying systems are specialized industrial equipment designed to handle and transport high-temperature fly ash from power plants and other industrial facilities. These systems are crucial for efficient and safe material transport, especially in environments where traditional methods may pose challenges due to the temperature and abrasive nature of the ash. The technology behind these systems combines pneumatic conveying principles with robust engineering to ensure reliable operation under demanding conditions.
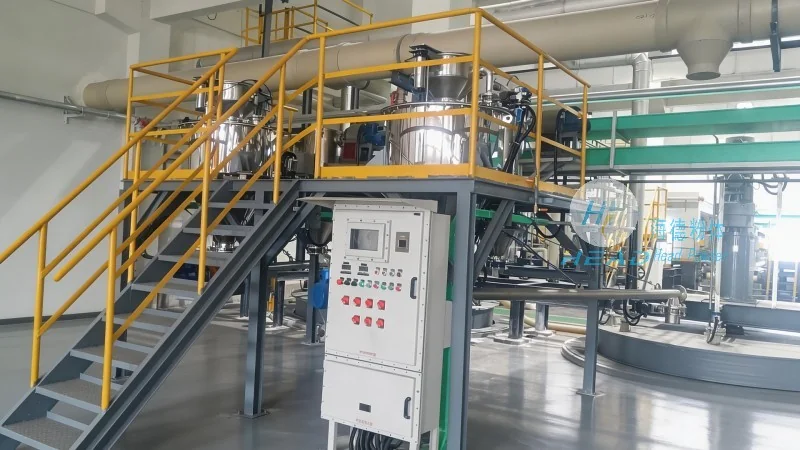
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer behind these advanced systems, is a leading engineering company based in Shandong, China. With a strong focus on industrial solutions, HeadPowder specializes in the design, manufacturing, and installation of pneumatic conveying equipment tailored to the needs of the power generation and environmental sectors. The company's commitment to quality and innovation has established it as a trusted partner for clients seeking reliable and efficient fly ash handling solutions.
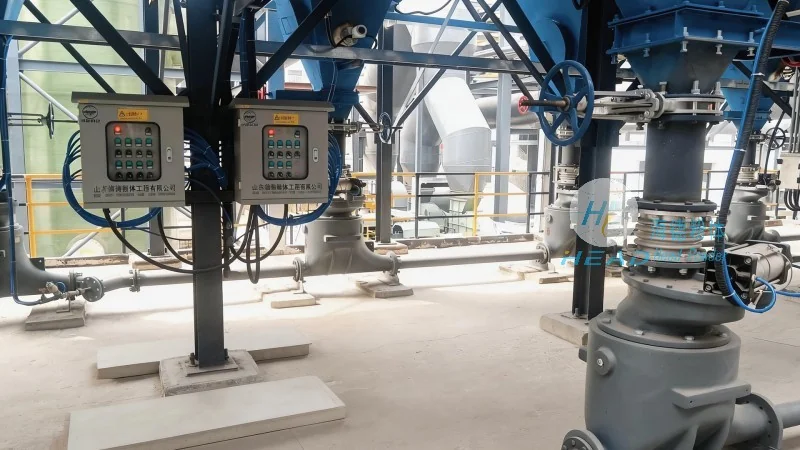
Key Components and Structure of the Pneumatic Conveying System
The high temperature fly ash pneumatic conveying system consists of several critical components that work in tandem to ensure effective material transport. The main parts include the ash collection hopper, the conveying pipeline, the air compressor or blower unit, and the control system. The ash collection hopper is designed to safely receive the high-temperature fly ash from the boiler or other sources, often equipped with insulation and temperature-resistant materials to prevent heat loss and equipment damage. The conveying pipeline is typically made of corrosion-resistant materials such as stainless steel or special alloys to withstand the abrasive and high-temperature conditions of the fly ash. The air compressor or blower provides the necessary pressure and airflow to move the ash through the pipeline, while the control system monitors and regulates the operation to maintain optimal performance and safety.
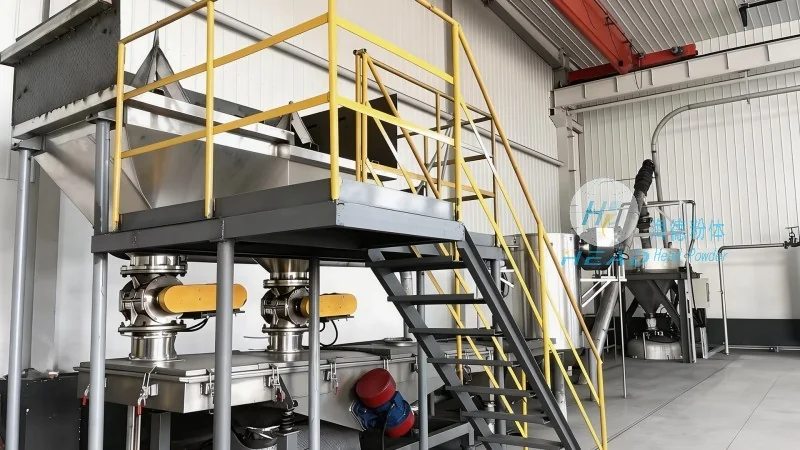
Working Principle of the High Temperature Pneumatic Conveying System
The operation of the high temperature fly ash pneumatic conveying system is based on the principle of pneumatic transport, where the material is carried by a stream of air under pressure. The process begins with the ash being discharged from the collection hopper into the conveying pipeline. The air compressor then generates a high-pressure air flow that propels the ash particles through the pipeline. As the ash travels, it is continuously mixed with the air, ensuring uniform transport and preventing blockages. The system is equipped with pressure sensors and flow meters to monitor the air pressure and material flow, allowing for real-time adjustments to maintain consistent performance. The discharge end of the system typically includes a filter or separator to remove any remaining ash particles from the air before it is released into the environment, ensuring compliance with environmental regulations.
Advantages and Applications of the System
High temperature fly ash pneumatic conveying systems offer several advantages over traditional methods, such as mechanical conveyors or gravity systems. These systems provide a more flexible and space-saving solution, as they can transport materials over long distances without the need for multiple transfer points. The pneumatic transport also reduces the risk of dust emissions and improves safety in the workplace, as the ash is contained within the pipeline. Additionally, the system is capable of handling high-temperature materials, making it suitable for power plants and other industrial facilities where the ash temperature can reach several hundred degrees Celsius. The applications of these systems are widespread, including the transport of fly ash from coal-fired power plants, industrial boilers, and waste incineration facilities. They are also used in the production of cement and other building materials, where the fly ash is a valuable byproduct that needs to be efficiently processed and utilized.
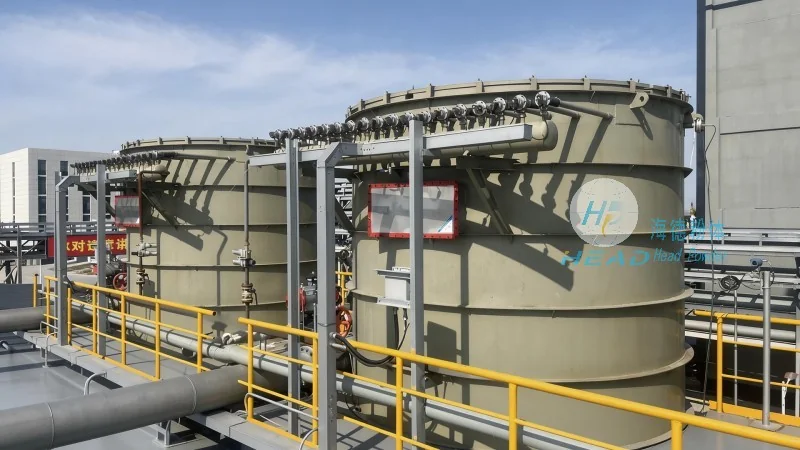
Quality Assurance and Technical Support from HeadPowder
HeadPowder places a strong emphasis on quality assurance throughout the design, manufacturing, and installation of its high temperature fly ash pneumatic conveying systems. The company adheres to international standards and uses advanced manufacturing techniques to ensure that each system meets the highest quality and performance requirements. The systems are rigorously tested under various conditions to verify their reliability and efficiency. Additionally, HeadPowder provides comprehensive technical support to its clients, including installation guidance, maintenance services, and troubleshooting assistance. The company's team of experienced engineers and technicians is available to address any concerns and ensure that the system operates at its optimal level. This commitment to quality and support has made HeadPowder a preferred choice for clients seeking reliable and efficient fly ash handling solutions.