

Working Principle and Features of High-Calcium Powder Material Pneumatic Conveying System
High-calcium powder, a critical component in numerous industrial sectors including cement manufacturing, construction materials, and chemical processing, demands efficient and precise material handling solutions. The high-calcium powder pneumatic conveying system represents a sophisticated approach to transporting these fine powders, ensuring minimal loss, contamination, and operational downtime. This system leverages pneumatic technology to move high-calcium powder from storage silos or hoppers to processing units, packaging lines, or other destinations with precision and reliability. The enclosed design of the system is particularly advantageous for industries where dust control and environmental compliance are paramount, making it a preferred choice for handling high-calcium powders in various applications.
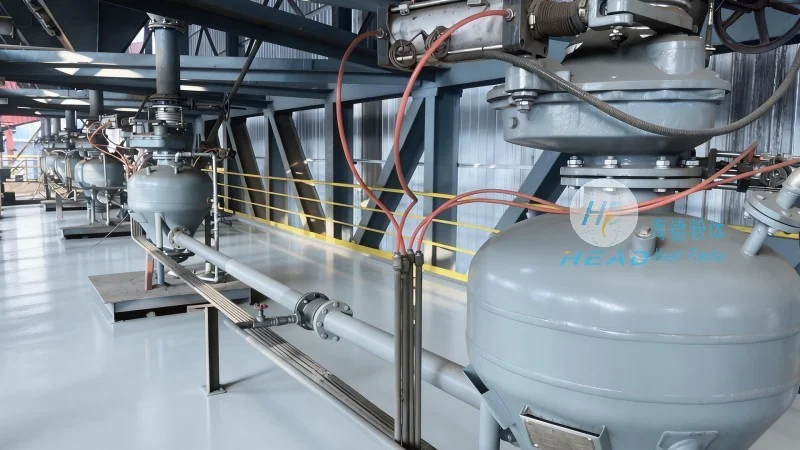
Working Principle of the High-Calcium Powder Pneumatic Conveying System
The operational mechanism of the high-calcium powder pneumatic conveying system is centered on the interaction between air and powder particles. The system comprises several key components: a material hopper for storage, a rotary valve or feeder to regulate the powder flow, a high-pressure air compressor to generate the conveying air, a pipeline network to transport the mixture, and a receiver or cyclone separator to separate the air from the powder. The process initiates when the high-calcium powder is discharged from the hopper into the feeder. The feeder then controls the flow rate, ensuring a consistent feed into the conveying pipe. Simultaneously, the air compressor produces high-pressure air, which is introduced into the pipeline. As the air travels through the pipe, it creates a low-pressure environment that draws the powder particles into the air stream, forming a dense phase or dilute phase conveying flow depending on the system design. The mixture of air and powder moves through the pipeline to the receiving hopper. At the receiver, a cyclone separator or a filter unit is employed to separate the air from the powder. The air, now free of powder particles, is directed back to the air compressor for recycling, while the high-calcium powder is collected in the receiver. This continuous cycle allows for uninterrupted material transport, with the system capable of handling varying powder quantities and distances efficiently.
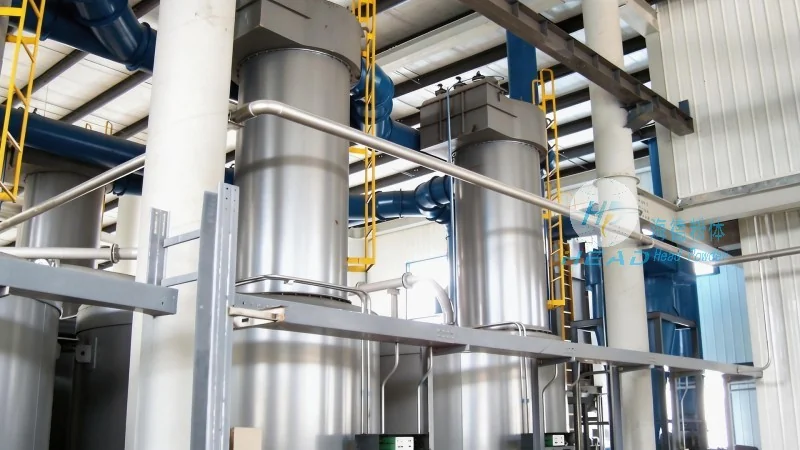
Key Features of the High-Calcium Powder Pneumatic Conveying System
The high-calcium powder pneumatic conveying system offers several distinct advantages that make it an ideal choice for handling fine powders. Firstly, its enclosed design provides a dust-free environment, preventing contamination of the powder and reducing the risk of environmental pollution. This is particularly important for high-calcium powders used in food, pharmaceutical, or construction industries where product purity is critical. Secondly, the system achieves high transport efficiency, with the ability to move large volumes of powder over long distances with minimal energy consumption. The use of air as the conveying medium allows for a compact and flexible system layout, reducing the need for extensive infrastructure and space. Thirdly, the system is highly adaptable, allowing for adjustments in conveying capacity, distance, or route without significant modifications. This flexibility is beneficial for industries that may experience changes in production volume or process requirements. Additionally, the system is designed for low maintenance, with components such as the hopper, feeder, and air compressor built to withstand the abrasive nature of high-calcium powder, ensuring long service life and reduced downtime. Finally, the system ensures product integrity by minimizing material degradation, such as agglomeration or degradation due to friction, and preventing cross-contamination between different batches of high-calcium powder.
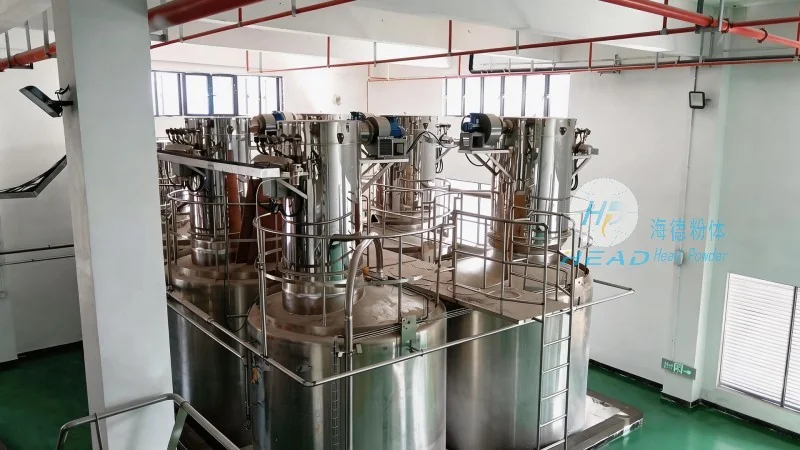
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer and supplier of advanced material handling systems, specializing in pneumatic conveying solutions for high-calcium powders and other fine materials. HeadPowder has established itself as a trusted partner in the industry, providing customized solutions that meet the unique demands of various clients. The company's headquarters and primary operations are located in Shandong, China, where it leverages its local expertise and resources to deliver high-quality products and services. HeadPowder's team of engineers and technicians is dedicated to innovation, continuously developing and improving its systems to enhance efficiency, reliability, and cost-effectiveness. The company adheres to strict quality control standards, ensuring that all products meet or exceed industry specifications and customer expectations. With a focus on customer satisfaction and long-term partnerships, HeadPowder is committed to supporting its clients in optimizing their material handling processes and achieving their operational goals.