

Working Principle and Features of a Potassium Carbonate Fertilizer Material Pneumatic Conveying Syst
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier specializing in the design, development, and production of advanced pneumatic conveying systems for various industrial applications. With a focus on high-efficiency and reliable material handling solutions, the company has established itself as a trusted partner in the chemical and fertilizer sectors.
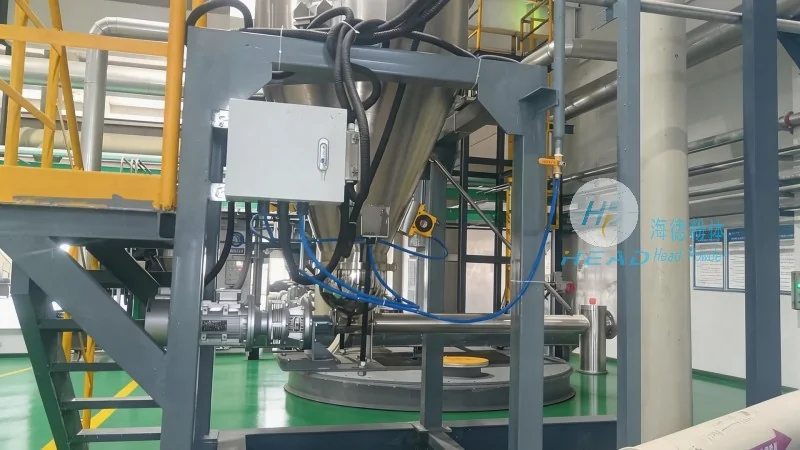
Overview of the Potassium Carbonate Fertilizer Pneumatic Conveying System
This system is engineered to efficiently transport potassium carbonate fertilizer, a critical component in modern agricultural practices. The system integrates advanced pneumatic conveying technology to ensure safe, dust-free, and continuous material transfer from storage silos or production lines to processing or packaging units. By leveraging air as the primary conveying medium, the system minimizes the need for mechanical components, reducing maintenance requirements and operational costs.
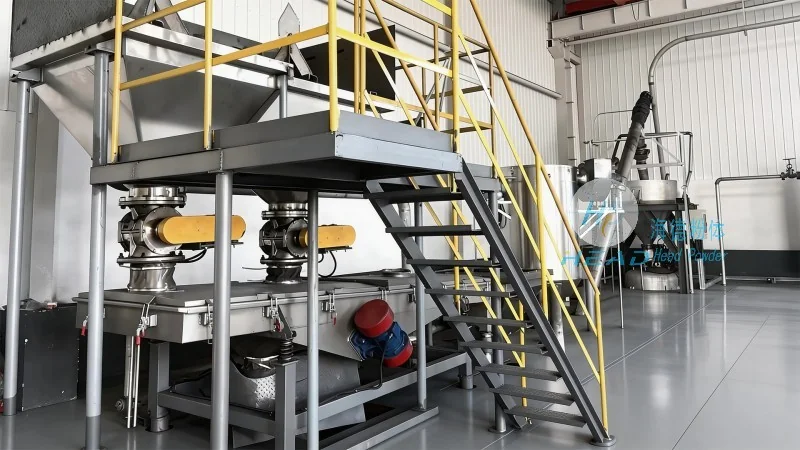
Working Principle of the Pneumatic Conveying System
The core mechanism of the system involves the use of a positive or negative pressure air stream to move the potassium carbonate fertilizer particles through a network of pipes. In a typical positive pressure system, a blower or compressor generates high-pressure air that forces the material along the pipeline. The material is suspended in the air stream, allowing it to travel through vertical, horizontal, or inclined sections without the need for additional mechanical equipment. The system includes components such as a feeder, airlock, and receiver to control the flow and ensure consistent material delivery. The design optimizes air flow and particle velocity to maintain a stable conveying rate, preventing blockages and ensuring efficient operation.
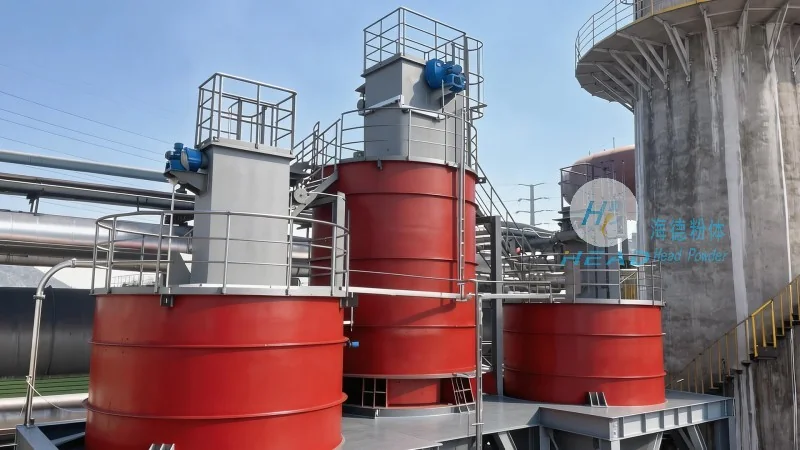
Key Features and Advantages
The potassium carbonate fertilizer pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several distinct advantages that enhance operational efficiency and product quality. One of the primary features is its ability to handle fine or abrasive materials like potassium carbonate without causing wear or damage to the system components. The system is designed with corrosion-resistant materials, such as stainless steel, to withstand the chemical properties of the fertilizer and ensure long-term durability. Additionally, the system incorporates advanced control systems that allow for real-time monitoring of flow rates, pressure, and material levels, enabling operators to adjust parameters dynamically for optimal performance. The dust-free operation is a significant benefit, as it reduces environmental contamination and improves workplace safety by eliminating the need for manual handling of powders.
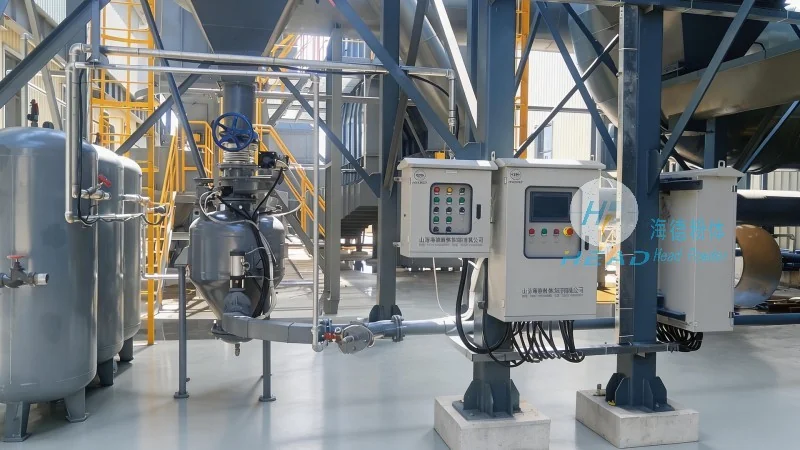
Application Benefits and Performance
Implementing this pneumatic conveying system in fertilizer production facilities provides several practical benefits. The continuous and automated material transfer reduces labor costs and minimizes the risk of human error associated with manual handling. The system's ability to handle large volumes of potassium carbonate efficiently supports high production throughput, making it suitable for both small-scale and large-scale fertilizer operations. Furthermore, the system's compact design allows for flexible installation in existing facilities, minimizing the need for extensive infrastructure modifications. The reliability of the system, with its low maintenance requirements and high uptime, ensures consistent production output and reduces downtime, which is crucial for meeting market demands. Overall, the system enhances the safety, efficiency, and sustainability of fertilizer processing, aligning with modern industrial standards.