

Principle and Working Scene Characteristics of Chicken Essence Material Handling Systems
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and implementation of efficient systems tailored for the chicken essence industry. Based in Shandong, China, the company leverages advanced engineering and industry expertise to deliver reliable and customized material handling solutions that meet the unique demands of modern food processing operations. This article explores the fundamental principles underlying chicken essence material handling systems and highlights the key characteristics of their operational environments.
Core Principles of Chicken Essence Material Handling Systems
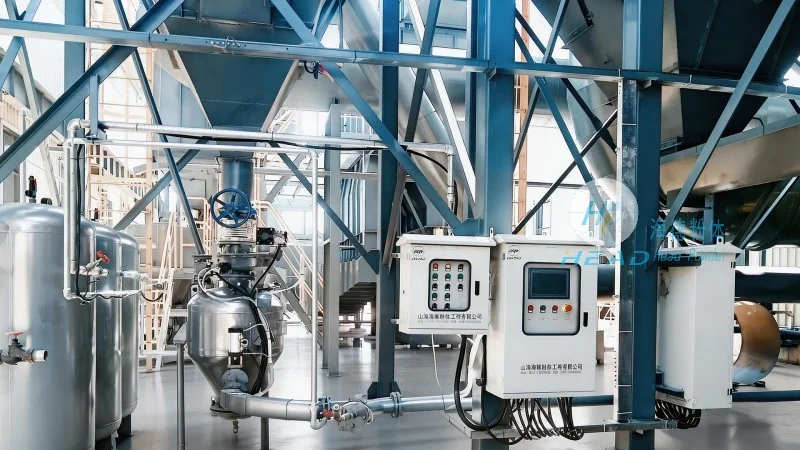
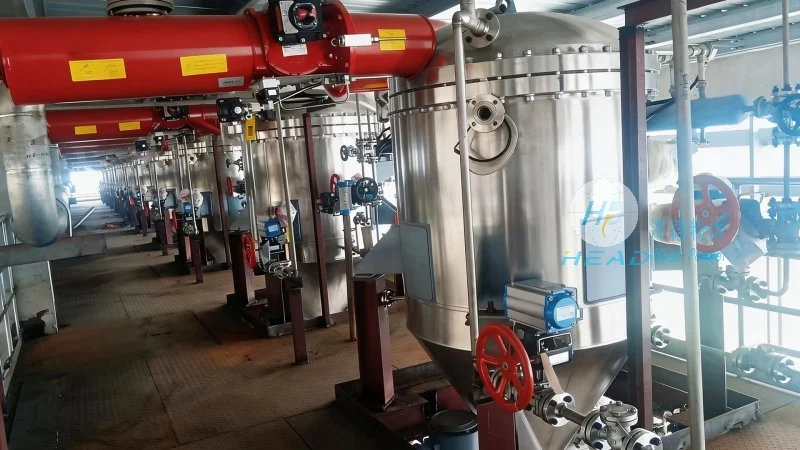
The operation of chicken essence material handling systems is built upon several core principles that ensure efficiency, safety, and product integrity. These systems are engineered to handle various forms of chicken essence products, including liquid extracts, powdered concentrates, and semi-solid formulations, with precision and minimal loss. A primary principle is the integration of automated control mechanisms that optimize material flow, reduce human intervention, and enhance operational consistency. This is achieved through the use of sensors, programmable logic controllers (PLCs), and advanced software that monitor and adjust the system's performance in real-time. Another critical principle is the emphasis on hygienic design, which is essential for maintaining the high standards required in food processing environments. Components such as stainless steel construction, easy-to-clean surfaces, and sealed joints are standard features to prevent contamination and ensure compliance with regulatory requirements. Additionally, energy efficiency is a key consideration, with systems incorporating variable frequency drives (VFDs) and optimized motor controls to reduce power consumption while maintaining performance.
Working Scene Characteristics of Chicken Essence Material Handling Systems
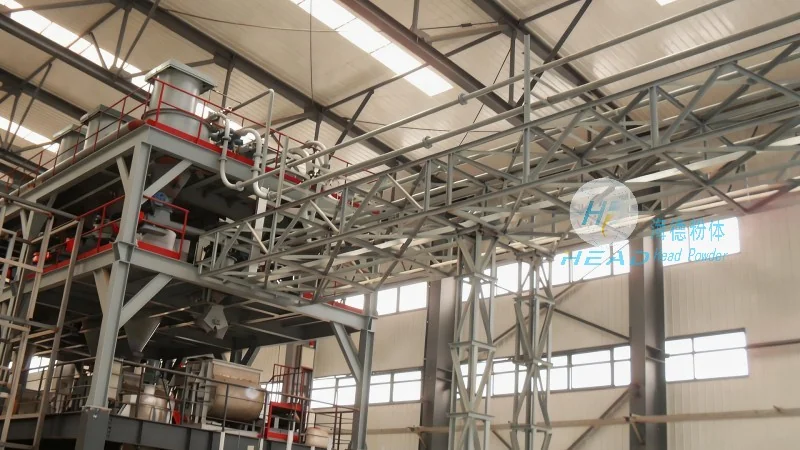
The working environments where chicken essence material handling systems are deployed exhibit distinct characteristics that influence system design and functionality. These systems are typically found in large-scale food processing plants, where high throughput and consistent product quality are paramount. The operational scenes often involve multiple stages of material handling, from raw ingredient reception and storage to processing, packaging, and distribution. In such settings, the systems must operate continuously for extended periods, often around the clock, to support the high production demands of the chicken essence industry. The working environment may also include varying temperatures and humidity levels, which necessitates robust equipment capable of withstanding these conditions without compromising performance. Furthermore, the systems are designed to handle different product viscosities and densities, requiring flexible conveyor systems, pumps, and storage tanks that can adapt to the specific properties of chicken essence products. The working scenes also emphasize safety, with features like emergency stop buttons, safety interlocks, and protective enclosures to protect operators and prevent accidents. Additionally, the systems are integrated with quality control measures, such as weighing scales and sampling devices, to ensure that each batch of chicken essence meets the required specifications before it is released for further processing or packaging.
Key Features and Benefits of the Systems
Chicken essence material handling systems from Shandong HeadPowder Engineering Co., Ltd. offer a range of features that address the specific needs of the industry. These systems are designed to enhance productivity by streamlining material flow and reducing downtime. The use of automated controls and sensors allows for precise monitoring and adjustment of the system's parameters, leading to improved efficiency and reduced waste. The hygienic design of the equipment ensures that the chicken essence products remain uncontaminated throughout the handling process, which is crucial for maintaining product quality and meeting regulatory standards. Energy-efficient components, such as VFDs, contribute to lower operational costs and a smaller environmental footprint. The systems are also modular, allowing for easy expansion or modification as production needs change. This flexibility makes them suitable for both new installations and upgrades to existing facilities. Furthermore, the systems are backed by comprehensive support services, including installation, training, and maintenance, to ensure that clients can maximize the benefits of their investment and minimize operational disruptions.
Conclusion
Chicken essence material handling systems from Shandong HeadPowder Engineering Co., Ltd. represent a sophisticated solution for the modern food processing industry. By adhering to the core principles of efficiency, hygiene, and safety, these systems provide reliable and effective material handling capabilities for chicken essence products. The working scene characteristics, such as high throughput and continuous operation, are well-suited to the demands of large-scale production, while the advanced features and benefits enhance overall operational performance. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and deliver tailored solutions that meet the evolving needs of the chicken essence industry, ensuring that clients can achieve their production goals with confidence and reliability.