

Sulfur Powder Pneumatic Conveying: A Solution for Material Transport Beyond Distance Limits
Sulfur powder, a critical raw material in various industrial applications, often poses challenges during transportation due to its fine particle size and tendency to agglomerate. Traditional methods like belt conveyors or bucket elevators may struggle with long-distance transport, leading to material loss, contamination, and operational inefficiencies. Pneumatic conveying offers a sophisticated solution to overcome these limitations, enabling efficient and reliable movement of sulfur powder over extended distances. This article explores the advantages of pneumatic conveying systems tailored for sulfur powder, highlighting how they enhance process reliability and operational performance.
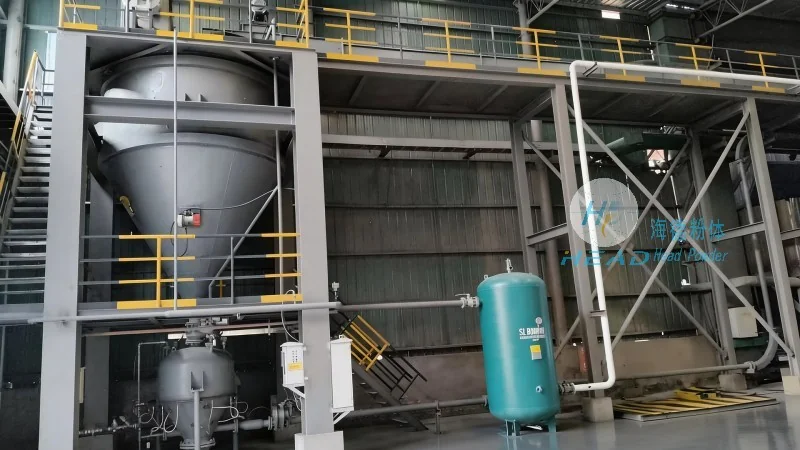
HeadPowder Engineering: Expertise in Sulfur Powder Handling
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized material handling solutions, with a focus on pneumatic conveying systems for challenging powders like sulfur. With years of experience in the industry, HeadPowder has developed advanced technologies and customized solutions to address the unique requirements of sulfur powder transport. The company’s expertise lies in designing systems that ensure minimal product degradation, consistent flow rates, and compliance with safety and environmental standards. HeadPowder’s commitment to innovation and customer satisfaction has established it as a trusted partner for industries relying on sulfur powder in their production processes.
Key Advantages of Pneumatic Conveying for Sulfur Powder
Pneumatic conveying systems for sulfur powder offer several key advantages that make them superior to conventional transport methods. First, they eliminate the need for physical contact between the material and the conveyor, reducing the risk of contamination and product degradation. This is particularly important for sulfur powder, which can be sensitive to moisture and temperature changes. Second, pneumatic systems can transport sulfur powder over long distances with minimal loss, as the material is carried by a stream of air rather than being subjected to mechanical stress. Third, these systems provide precise control over flow rates and pressure, allowing for smooth and consistent material delivery to processing units. Additionally, pneumatic conveying can integrate with existing industrial infrastructure, reducing installation and operational costs compared to alternative solutions.
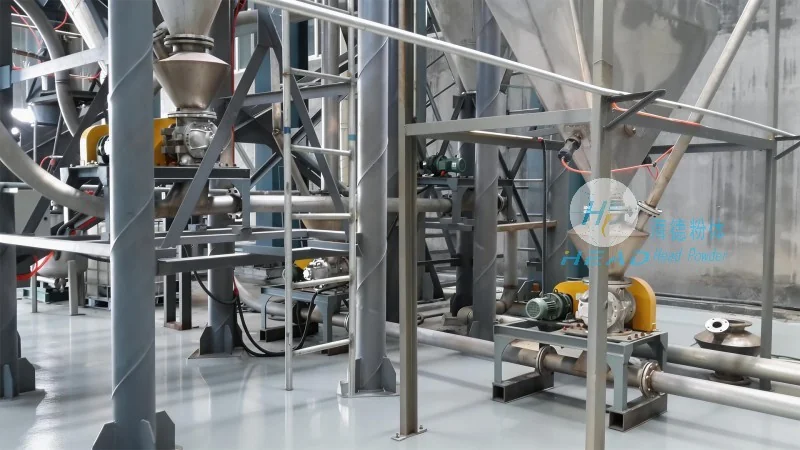
Customized Solutions for Diverse Sulfur Powder Applications
HeadPowder understands that sulfur powder is used in a wide range of applications, from chemical manufacturing to agricultural and industrial processes. To meet these diverse needs, the company offers customized pneumatic conveying solutions tailored to specific operational requirements. For example, in chemical plants, sulfur powder may need to be transported from storage silos to reactors, requiring high-pressure systems with precise control. In contrast, agricultural applications might involve lower-pressure systems for bulk handling. HeadPowder’s engineers work closely with clients to assess their specific needs, including the type of sulfur powder, distance of transport, and required flow rates, to design a system that optimizes performance and efficiency. The company’s solutions often incorporate advanced features such as cyclone separators, dust collectors, and automated control systems to ensure safe and efficient operation.
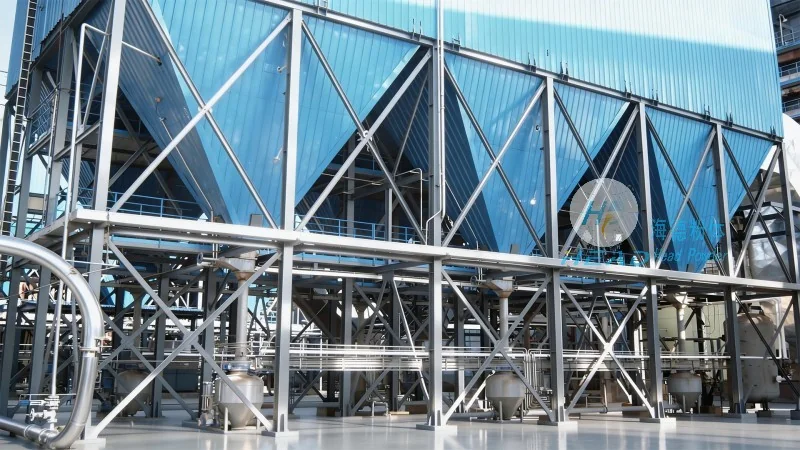
Ensuring Safety and Compliance in Sulfur Powder Handling
Safety is a top priority when handling sulfur powder, as it can be a hazardous material under certain conditions. Pneumatic conveying systems designed by HeadPowder incorporate multiple safety features to mitigate risks. These include explosion-proof components, pressure relief valves, and monitoring systems that detect abnormal conditions and trigger shutdowns. Additionally, the systems are engineered to minimize dust emissions, reducing the risk of respiratory issues for operators and preventing environmental contamination. Compliance with local regulations and industry standards is also a key consideration, and HeadPowder ensures that all its systems meet or exceed relevant safety and environmental requirements. By prioritizing safety and compliance, HeadPowder provides peace of mind to clients operating with sulfur powder, knowing that their material handling processes are secure and responsible.
Conclusion: Enhancing Efficiency with Pneumatic Conveying
In conclusion, pneumatic conveying of sulfur powder is a highly effective solution for overcoming distance limitations and ensuring efficient material transport. With its ability to minimize product loss, maintain quality, and provide precise control, this technology is essential for industries relying on sulfur powder. HeadPowder Engineering, with its expertise and customized solutions, plays a crucial role in enabling these benefits, helping clients improve their operational efficiency and productivity. By leveraging advanced pneumatic conveying systems, businesses can streamline their sulfur powder handling processes, reduce costs, and enhance overall process reliability. As the demand for efficient material transport continues to grow, pneumatic conveying remains a vital technology, and companies like HeadPowder are at the forefront of providing innovative solutions to meet these challenges.