

Introduction to Equipment and Structural Principles of Coal Particle Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced coal particle pneumatic conveying systems. These systems are engineered to efficiently transport coal particles through a pneumatic process, offering a reliable solution for various industrial applications. The equipment is tailored to meet the specific needs of clients, ensuring optimal performance and durability in demanding environments.
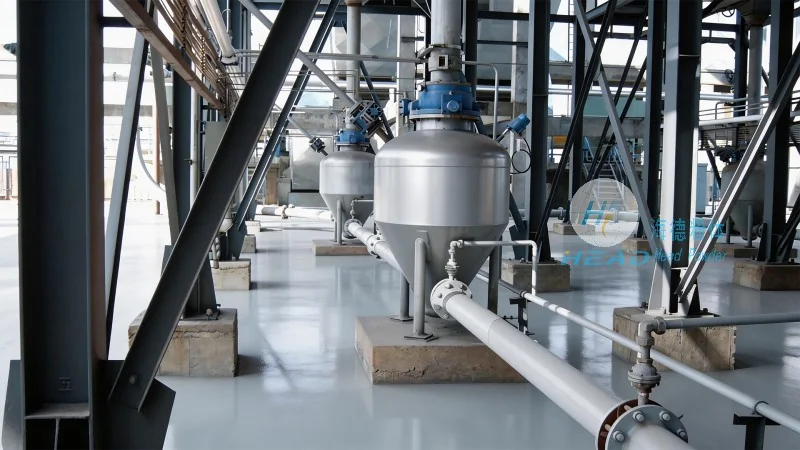
Structural Principles of the Pneumatic Conveying System
The core of the coal particle pneumatic conveying system lies in its integrated components, which work in harmony to facilitate the movement of coal particles. The system typically includes a feeding device, a conveying pipeline, a pressure vessel or receiver, and a control system. The feeding device ensures a consistent flow of coal particles into the pipeline, while the conveying pipeline, often made of high-quality materials such as stainless steel or special alloys, withstands the pressure and friction associated with particle transport. The pressure vessel or receiver collects the conveyed coal particles and regulates the system's pressure. The control system monitors and adjusts the operation parameters, such as air pressure and flow rate, to maintain stable and efficient conveying.
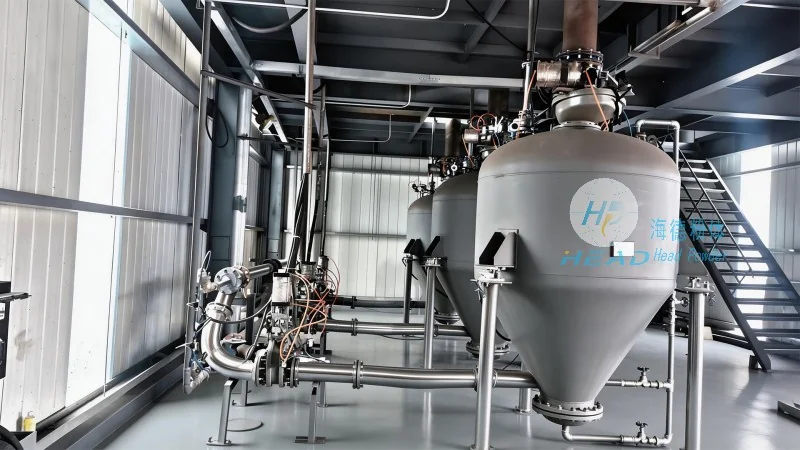
Key Components and Their Functions
Each component of the coal particle pneumatic conveying system plays a critical role in its overall functionality. The feeding device, which may include a hopper or a rotary valve, controls the rate at which coal particles enter the system, preventing blockages and ensuring a smooth flow. The conveying pipeline is designed with appropriate bends and fittings to minimize pressure loss and maintain the integrity of the coal particles. The pressure vessel or receiver is equipped with a dust collection system to capture any airborne particles, enhancing safety and compliance with environmental regulations. The control system integrates sensors and actuators to provide real-time monitoring and automated adjustments, optimizing the system's performance and reducing operational costs.
Advantages of the Pneumatic Conveying System
Implementing a coal particle pneumatic conveying system offers several advantages over traditional methods like belt conveyors or bucket elevators. Firstly, it eliminates the need for physical contact between the coal particles and the conveying equipment, reducing wear and tear and extending the lifespan of the system. Secondly, the system is highly flexible, allowing for changes in the conveying route and capacity without significant modifications. Thirdly, it provides a dust-free and clean operation environment, improving workplace safety and reducing the risk of fire hazards. Additionally, the pneumatic conveying system can handle a wide range of coal particle sizes and moisture content, making it suitable for diverse industrial applications.
Application Scenarios and Industrial Use
The coal particle pneumatic conveying system is widely used in various industries, including power generation, coal processing, and chemical manufacturing. In power plants, it efficiently transports coal from storage areas to boilers, ensuring a continuous and reliable fuel supply. In coal processing facilities, the system aids in the transportation of raw coal to processing units, such as crushers and grinders. In chemical plants, it facilitates the movement of coal-derived products, such as coal tar and coke, to different processing stages. The system's adaptability and efficiency make it an essential component in modern industrial operations, contributing to improved productivity and operational efficiency.
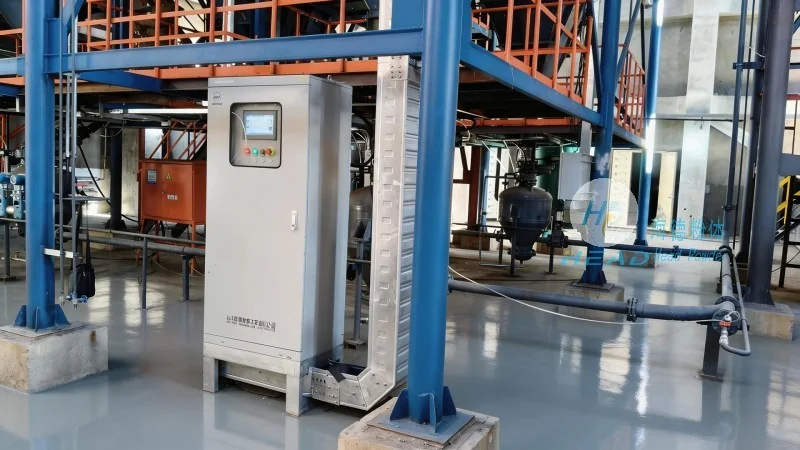
Quality Assurance and Technical Support
HeadPowder places a strong emphasis on quality assurance throughout the design, manufacturing, and installation of its coal particle pneumatic conveying systems. The company adheres to international standards and employs rigorous testing procedures to ensure that each system meets the highest performance and safety requirements. Additionally, HeadPowder provides comprehensive technical support and after-sales services to its clients. This includes installation guidance, maintenance training, and prompt technical assistance for any issues that may arise. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the industry, delivering reliable and efficient solutions for coal particle transportation needs.