

Pneumatic Conveying in Bulk Transport of Bio-Enzymes
Bio-enzymes are essential components in various industrial processes, including pharmaceuticals, food processing, and biofuel production. These enzymes are often sensitive to environmental factors such as temperature, humidity, and physical stress. Traditional bulk transport methods like trucks or conveyor belts may introduce contamination or degrade the enzyme's activity. Pneumatic conveying offers a solution by providing a closed system that minimizes exposure to external elements and ensures gentle handling of the product.
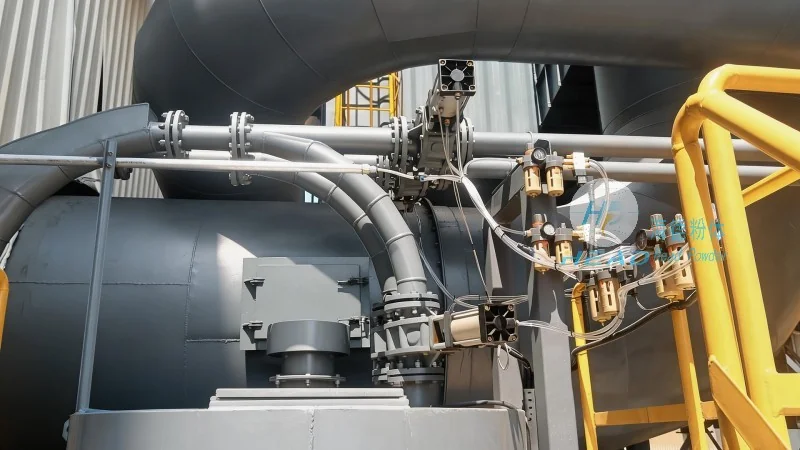
The Advantages of Pneumatic Conveying for Bio-Enzyme Transport
One of the primary benefits of using pneumatic conveying for bio-enzyme transport is the ability to maintain product integrity. The enclosed system prevents contamination from dust, moisture, or other particles, which is crucial for maintaining the enzyme's efficacy. Additionally, the gentle movement of the material within the system reduces mechanical stress, preserving the enzyme's structure and activity levels. This is particularly important for enzymes used in sensitive applications like pharmaceutical manufacturing, where even minor degradation can impact product quality.
Key Features of HeadPowder's Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the unique needs of bio-enzyme transport. Our systems are engineered with precision to handle the delicate nature of bio-enzymes while ensuring efficient and reliable transport. Key features include:
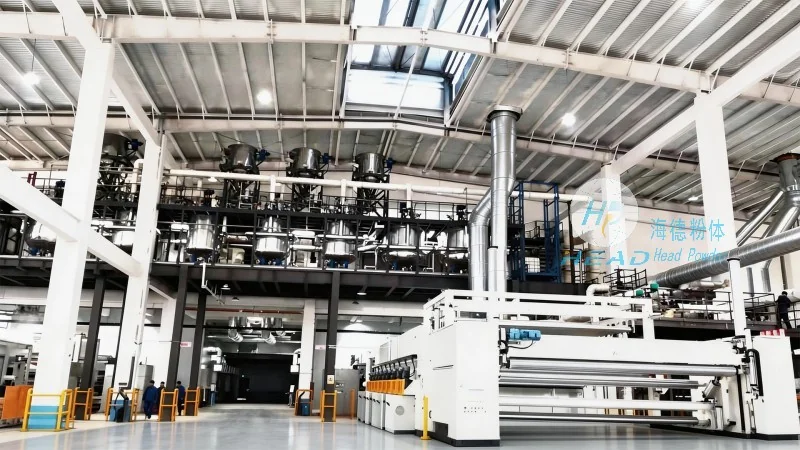
- Customizable system designs to accommodate varying enzyme types and production volumes.
- Highly efficient air flow management to minimize energy consumption and operational costs.
- Advanced filtration and cleaning systems to maintain a sterile environment and prevent cross-contamination.
- Robust materials of construction, such as stainless steel, to ensure durability and compliance with industry standards like GMP (Good Manufacturing Practice).
Applications in the Bio-Enzyme Industry
HeadPowder's pneumatic conveying systems are widely used in the bio-enzyme industry for applications including:
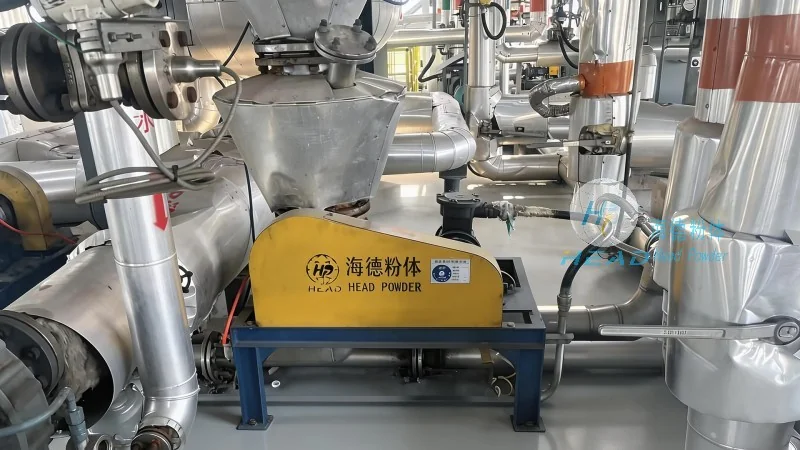
- Transporting enzymes from production reactors to storage tanks or packaging lines.
- Transferring enzymes between different processing stages, such as from fermentation to purification.
- Supplying enzymes to downstream processes like blending or formulation.
Ensuring Compliance and Quality
For industries dealing with bio-enzymes, regulatory compliance is paramount. HeadPowder's systems are designed to meet stringent quality and safety standards. Our equipment is constructed from materials that are easy to clean and maintain, reducing the risk of microbial growth. Additionally, our systems can be integrated with monitoring and control technologies to ensure consistent performance and product quality throughout the transport process.
Conclusion
For businesses in the bio-enzyme industry, choosing the right transport method is critical to maintaining product quality and operational efficiency. Pneumatic conveying, with its ability to handle delicate materials while ensuring safety and compliance, is an excellent choice. Shandong HeadPowder Engineering Co., Ltd. provides reliable and effective pneumatic conveying solutions that meet the specific requirements of bio-enzyme transport, helping companies achieve their production goals while upholding the highest standards of quality and safety.