

Working Principle and Features of Furfural Residue Pneumatic Conveying System
For industrial applications involving the handling of furfural residue, efficient and reliable material transport is crucial. The furfural residue pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution to address the challenges associated with transporting this specific type of waste material. This system is designed to ensure safe, effective, and environmentally compliant material handling, making it an essential component in modern industrial processes.
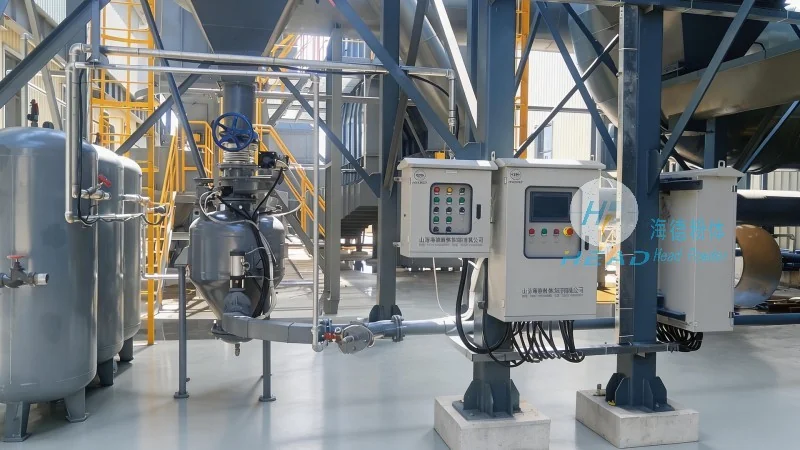
Company Overview: HeadPowder
As a leading engineering firm in China, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced material handling systems. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted provider of pneumatic conveying solutions for various industrial sectors. The company's expertise in mechanical engineering and material science enables it to deliver customized systems that meet the unique requirements of clients, ensuring optimal performance and durability.
Working Principle of the Furfural Residue Pneumatic Conveying System
The core of the furfural residue pneumatic conveying system lies in its pneumatic transport mechanism, which utilizes air as the primary medium to move the material. The system operates by creating a pressure differential between the material source and the destination, allowing the material to be carried through a pipeline network. The process typically involves several key components: a material feeder, a blower or air compressor, a conveying pipeline, and a discharge unit. The material is first fed into the system, where it is mixed with air and then transported through the pipeline. The air pressure and velocity are carefully controlled to ensure the material is conveyed without clogging or degradation. The system may also include additional components such as cyclones, filters, and dust collectors to manage the air and material flow, ensuring that the conveying process is efficient and clean.
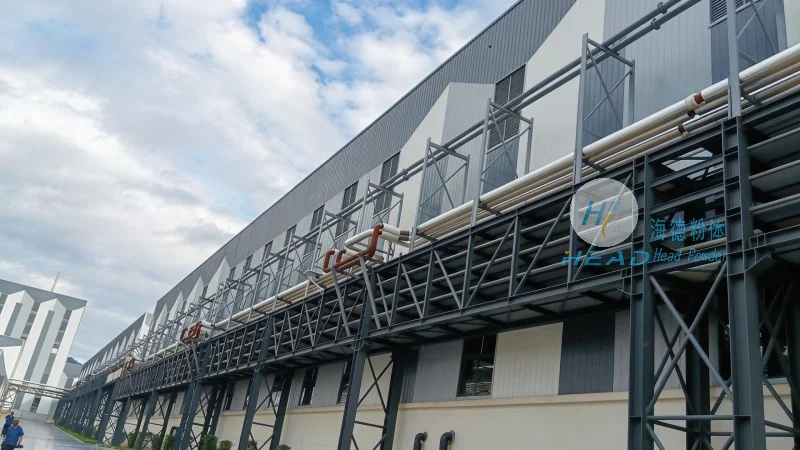
Key Features and Advantages
The furfural residue pneumatic conveying system from HeadPowder offers several distinct features and advantages that make it a superior choice for industrial applications. Firstly, it provides a highly efficient and continuous material transport solution, reducing the need for manual handling and minimizing labor costs. The system is designed to handle a wide range of material characteristics, including varying particle sizes and moisture content, ensuring consistent performance. Secondly, the pneumatic conveying method is highly flexible, allowing for easy integration into existing industrial setups and the ability to transport materials over long distances without the need for intermediate storage or transfer points. Thirdly, the system is equipped with advanced control systems that allow for precise regulation of air flow and pressure, ensuring optimal material transport and minimizing energy consumption. Additionally, the system is designed with safety and environmental considerations in mind, incorporating features such as dust suppression and air filtration to comply with regulatory standards and protect the environment. The use of pneumatic conveying also reduces the risk of material contamination and degradation, preserving the quality of the furfural residue during transport.
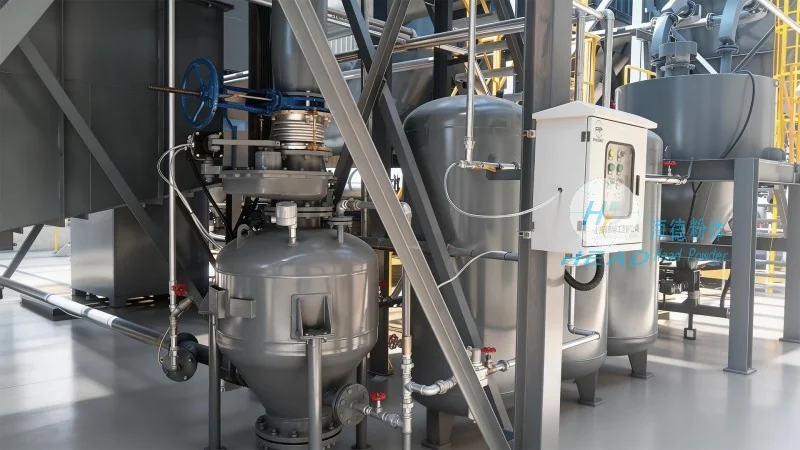
Technical Specifications and Customization Options
HeadPowder's furfural residue pneumatic conveying system is available in various configurations to suit different industrial needs. The system can be customized to handle different material volumes and pipeline lengths, with options for both positive and negative pressure conveying. The blower or air compressor used in the system can be selected based on the specific requirements of the application, with options ranging from low to high pressure systems. The conveying pipeline is typically made of durable materials such as stainless steel or plastic, which are resistant to corrosion and wear from the furfural residue. The system may also include additional features such as automatic control systems, which allow for remote monitoring and adjustment of the conveying process. These customization options enable clients to tailor the system to their specific operational needs, ensuring maximum efficiency and cost-effectiveness.
Application Scenarios and Industry Benefits
The furfural residue pneumatic conveying system is widely used in various industrial sectors, including the chemical, pharmaceutical, and food processing industries. In the chemical industry, it is commonly used to transport furfural residue from reactors to storage facilities or for further processing. In the pharmaceutical industry, the system is used to handle waste materials from production processes, ensuring that they are disposed of in an environmentally friendly manner. In the food processing industry, the system is used to transport byproducts from furfural production, which can be used as animal feed or for other industrial applications. The use of this system provides several benefits to these industries, including improved operational efficiency, reduced labor costs, and enhanced environmental compliance. By eliminating the need for manual handling and reducing the risk of material contamination, the system helps to improve overall productivity and product quality.