

The Working Principle and Features of Stabilizer Powder Pneumatic Conveying Equipment
Stabilizer powder pneumatic conveying equipment is a specialized device used in industrial processes to transport fine powders, such as those used in chemical, pharmaceutical, and food industries. This equipment is particularly important for materials like stabilizers, which require precise handling to maintain their quality and prevent agglomeration or degradation during transport. The following sections will explore the working principle and key features of this equipment, providing a comprehensive understanding of its functionality and benefits.
Company Introduction
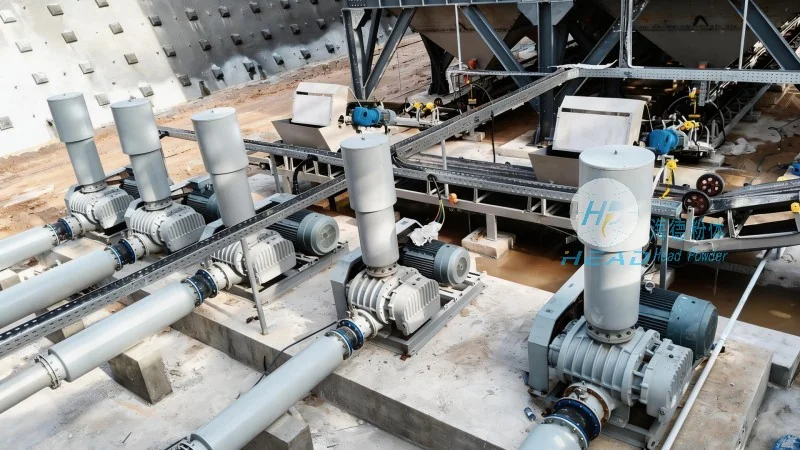
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer in the field of pneumatic conveying systems. With a base in Shandong, China, the company specializes in designing, manufacturing, and supplying high-quality equipment tailored to the needs of various industries. HeadPowder's commitment to innovation and quality ensures that their products meet the stringent requirements of modern industrial applications, particularly for handling sensitive materials like stabilizer powders.
Working Principle of Stabilizer Powder Pneumatic Conveying Equipment
The core working principle of stabilizer powder pneumatic conveying equipment involves the use of compressed air to move powder particles through a pipeline system. This process typically operates under negative pressure, where the air is drawn into the system to create a vacuum that pulls the powder from the source container into the conveying line. The equipment consists of several key components, including a hopper, a rotary valve, a filter, and a venturi or pressure drop device. The hopper holds the stabilizer powder, and the rotary valve controls the flow of powder into the conveying line. As the compressed air enters the system, it creates a flow that entrains the powder particles, transporting them to the destination point. The filter is crucial for maintaining air quality and preventing dust from escaping into the environment, while the venturi or pressure drop device helps to regulate the air flow and ensure efficient transport.
Key Features of Stabilizer Powder Pneumatic Conveying Equipment
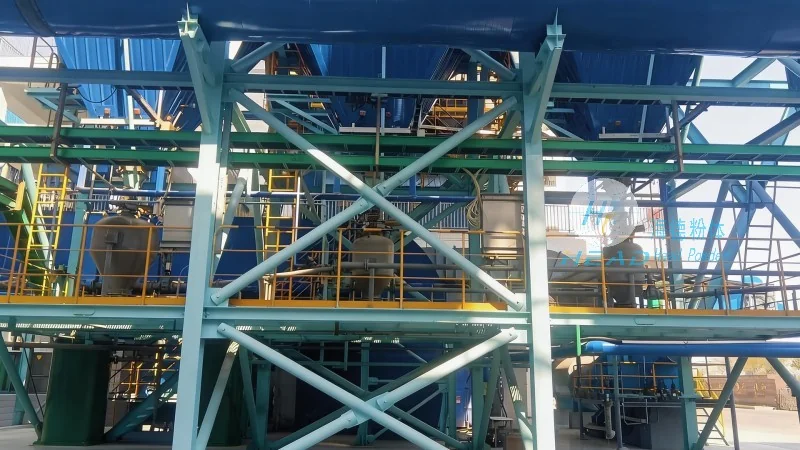
Stabilizer powder pneumatic conveying equipment offers several advantages that make it an ideal choice for industrial applications. One of the primary features is its ability to handle fine, abrasive, or sensitive powders without causing degradation or contamination. The equipment is designed to minimize particle breakage and maintain the integrity of the stabilizer powder, which is critical for its performance in downstream processes. Another key feature is the flexibility of the system, which can be adapted to various conveying distances and heights, making it suitable for both short and long-distance transport. The equipment also provides a dust-free operation, which enhances workplace safety and compliance with environmental regulations. Additionally, the system is easy to clean and maintain, reducing downtime and operational costs. The use of compressed air as the conveying medium allows for a closed system, preventing product contamination and protecting the environment from dust emissions. Overall, the features of this equipment contribute to improved efficiency, product quality, and operational safety in industrial settings.
Application and Benefits in Industrial Processes
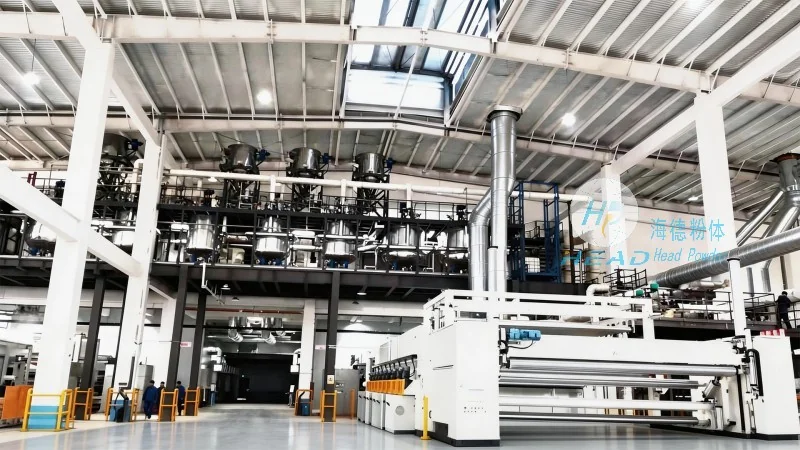
Stabilizer powder pneumatic conveying equipment is widely used in industries where the consistent and reliable transport of fine powders is essential. In the chemical industry, it is used to transport stabilizers for polymer production, ensuring that the powders are delivered to reactors without loss or degradation. In the pharmaceutical industry, the equipment is employed to handle active ingredients and excipients, maintaining the purity and stability of the products. The food industry also benefits from this equipment when transporting stabilizers for food products, as it ensures that the powders are handled hygienically and without contamination. The benefits of using this equipment include increased production efficiency, reduced material waste, and improved product quality. By eliminating the need for manual handling and traditional bulk transport methods, the equipment streamlines operations and reduces the risk of human error. Furthermore, the closed system design minimizes environmental impact, making it a sustainable choice for modern industrial applications.
Conclusion
In summary, stabilizer powder pneumatic conveying equipment is a sophisticated and efficient solution for transporting fine powders in various industrial applications. The working principle, which relies on compressed air to move particles through a pipeline system, ensures precise and controlled transport. The key features, including its ability to handle sensitive materials, flexibility, and dust-free operation, make it a preferred choice for industries requiring high-quality and reliable powder transport. With a strong presence in the market, HeadPowder Engineering Co., Ltd. continues to provide innovative solutions that meet the evolving needs of industrial processes, particularly for stabilizer powders. The equipment's benefits, such as improved efficiency, product quality, and environmental compliance, highlight its importance in modern industrial operations.