

Working Principle and Features of Cement Aggregate Material Pneumatic Conveying Systems
For industrial applications requiring efficient and reliable material handling, pneumatic conveying systems have emerged as a critical solution for transporting cement, aggregates, and other bulk materials. This article explores the working principle and key features of such systems, highlighting their advantages in modern material handling operations.
Working Principle of Pneumatic Conveying Systems
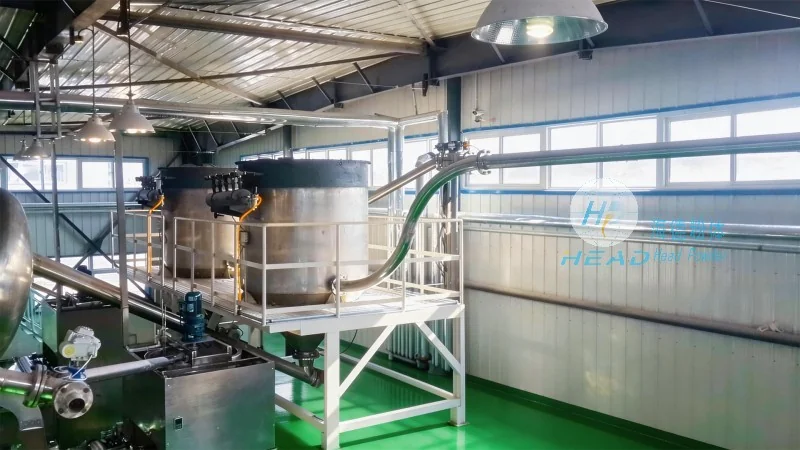
Pneumatic conveying systems operate by using compressed air or gas to transport bulk materials through a pipeline. The process typically involves a hopper or feeder that feeds the material into a duct, where it is entrained by the moving air stream. The air and material mixture travels through the pipeline to the discharge point, where the material is separated from the air and collected. The system can be either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out), depending on the application requirements. The headpowder engineering team has optimized these systems to ensure efficient material flow and minimal pressure drop, which is crucial for maintaining system performance and energy efficiency.
Key Features and Advantages
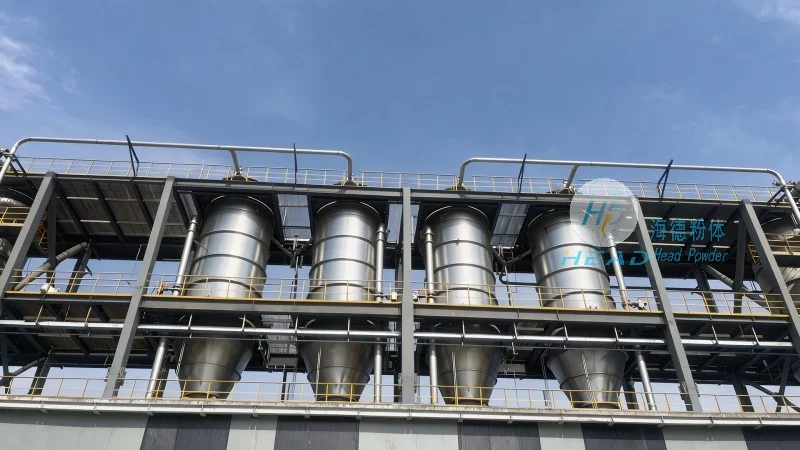
HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in designing and manufacturing advanced pneumatic conveying solutions tailored to the needs of the cement and aggregate industries. The systems offered by HeadPowder are characterized by several key features that enhance operational efficiency and reliability. Firstly, the use of high-quality materials and robust construction ensures durability and long service life, reducing maintenance costs and downtime. Secondly, the systems are designed with flexibility in mind, allowing for easy integration into existing production lines and adaptation to varying material types and flow rates. Thirdly, advanced control systems enable precise regulation of air pressure and flow, ensuring consistent material transport and minimizing product degradation. Additionally, the systems are engineered for low energy consumption, contributing to cost savings and environmental sustainability. These features make pneumatic conveying systems an ideal choice for industries seeking to improve material handling efficiency while maintaining high standards of performance and reliability.
Application-Specific Benefits
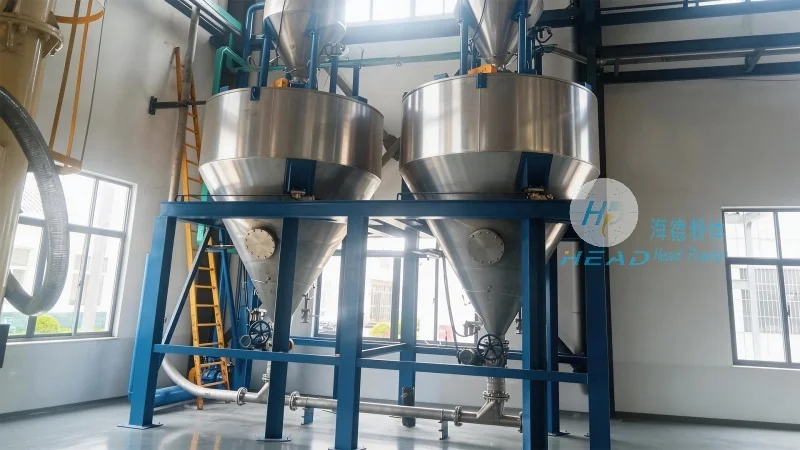
In the cement and aggregate sectors, the efficient transport of raw materials and finished products is essential for maintaining production schedules and meeting quality standards. The pneumatic conveying systems developed by HeadPowder Engineering Co., Ltd. address these needs by providing a seamless and reliable material transport solution. For example, in cement plants, these systems can handle the transport of raw materials such as limestone, clay, and sand from storage silos to the grinding mills, ensuring a continuous supply of feedstock. Similarly, in aggregate processing facilities, the systems facilitate the movement of crushed stone and sand from processing units to storage or packaging areas. The ability to handle abrasive materials without causing wear and tear on the system components is another significant advantage, as it extends the lifespan of the equipment and reduces replacement costs. Furthermore, the systems are designed to minimize dust emissions, contributing to a safer and more environmentally friendly working environment. By leveraging the expertise of HeadPowder Engineering Co., Ltd., industries can achieve improved operational efficiency, reduced downtime, and enhanced product quality through the use of advanced pneumatic conveying technology.
Conclusion
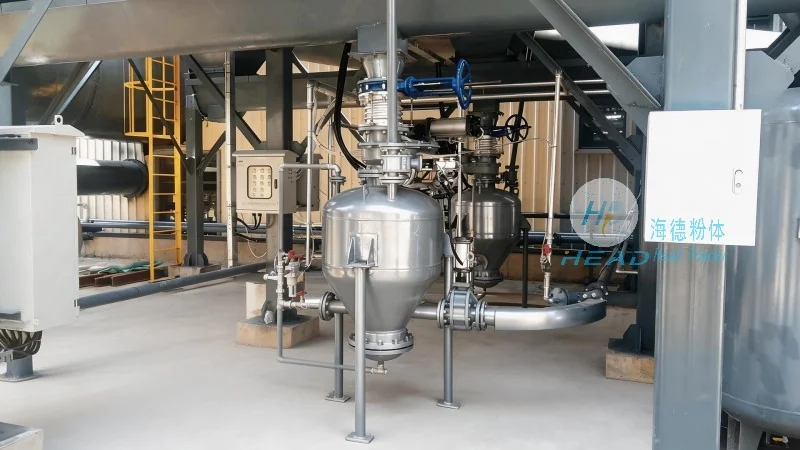
As the demand for efficient material handling solutions continues to grow, pneumatic conveying systems remain a vital component in modern industrial operations. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, has established itself as a leading provider of high-quality pneumatic conveying systems tailored to the specific needs of the cement and aggregate industries. By focusing on the working principles and key features of these systems, HeadPowder ensures that its clients receive reliable, efficient, and cost-effective solutions that enhance their overall operational performance. The combination of robust engineering, advanced control systems, and durable construction makes the pneumatic conveying systems from HeadPowder a preferred choice for industries seeking to optimize their material transport processes and achieve long-term success.