

Working Principle and Features of Sorghum Distillers Grains Material Pneumatic Conveying System
HeadPowder Engineering, a leading provider in material handling solutions, specializes in the design and implementation of pneumatic conveying systems for industrial applications. The system under discussion is specifically tailored for the efficient transport of sorghum distillers grains, a byproduct commonly found in the distillation process of sorghum-based alcoholic beverages. This article will delve into the working principle and key features of such a system, highlighting its operational efficiency and technological advancements.
Working Principle of the Pneumatic Conveying System
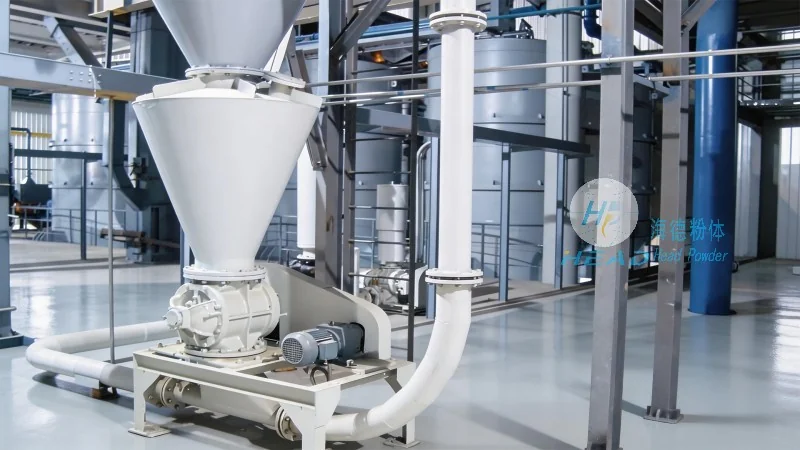
The pneumatic conveying system for sorghum distillers grains operates on the fundamental principle of using air to transport bulk materials through a pipeline network. At its core, the system comprises several critical components that work in tandem to ensure smooth and continuous material movement. The process begins with the material being fed into a hopper or storage silo, where it is then drawn into a conveying line via a rotary valve or feeder. Compressed air, generated by a high-pressure blower or fan, is introduced into the pipeline, creating a flow that propels the material particles forward. The air velocity within the pipeline is carefully controlled to maintain a stable suspension of the material, preventing blockages and ensuring uniform transport. The system typically includes a series of bends, elbows, and expansion joints to accommodate changes in direction and elevation, while maintaining the integrity of the material flow. Upon reaching the destination, such as a storage tank or processing unit, the material is discharged through a control valve, with the air being filtered and recycled back into the system to minimize energy consumption and environmental impact.
Key Features and Advantages of the System
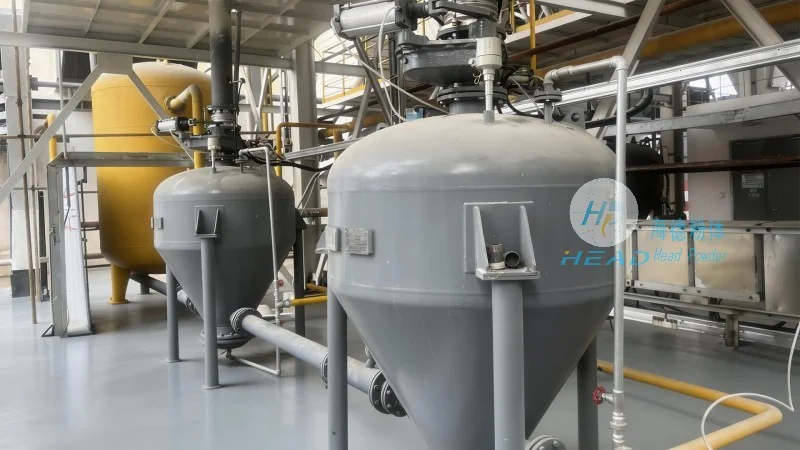
The pneumatic conveying system for sorghum distillers grains offers several distinct advantages that make it an ideal choice for industrial applications. Firstly, it provides a completely enclosed and hygienic transport environment, which is crucial for maintaining the quality and safety of the material, especially in food and beverage processing industries. Unlike traditional mechanical conveyors, which may cause material degradation or contamination due to friction and exposure to the environment, the pneumatic system ensures that the material remains in a controlled state throughout the transport process. Secondly, the system offers high flexibility in terms of layout and integration, allowing for customized designs that can adapt to various plant configurations and operational requirements. This flexibility enables the system to be installed in existing facilities or as part of new plant constructions, with minimal disruption to ongoing operations. Thirdly, the system is highly efficient in terms of energy consumption and operational costs. By utilizing compressed air as the primary transport medium, the system reduces the need for mechanical components such as belts, chains, or buckets, which are prone to wear and maintenance. The recycling of air also contributes to lower energy bills and reduced operational expenses over time. Additionally, the system provides excellent control over material flow rates and pressure, allowing for precise regulation of the conveying process to meet specific production demands. This level of control is particularly beneficial in processes where consistent material delivery is critical, such as in the production of high-quality alcoholic beverages where the quality of the distillers grains directly impacts the final product.
Technical Specifications and Customization Options
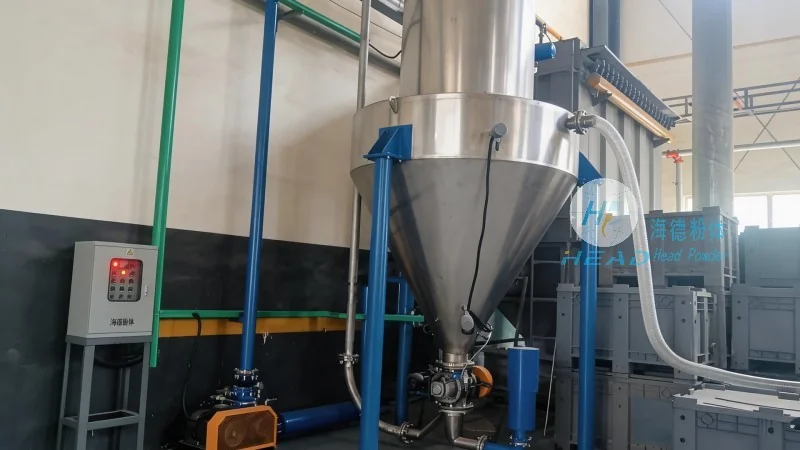
HeadPowder Engineering offers a range of technical specifications and customization options to suit the diverse needs of its clients. The pneumatic conveying system can be configured with different types of air movers, including positive displacement blowers and centrifugal fans, depending on the specific material characteristics and conveying distance. The pipeline design can be tailored to handle varying particle sizes and moisture content, with options for stainless steel, carbon steel, or special alloys to ensure durability and resistance to corrosion. The system also includes advanced control systems that allow for real-time monitoring of pressure, flow rate, and material level, providing operators with comprehensive data for process optimization and troubleshooting. Furthermore, the company provides comprehensive installation and commissioning services, ensuring that the system is properly integrated into the client's existing infrastructure and operates at peak efficiency from day one. The customization options extend to the control panel and automation features, allowing for integration with existing plant control systems and remote monitoring capabilities. This level of customization ensures that the system not only meets but exceeds the client's operational requirements, providing long-term reliability and performance.
Application and Industry Impact
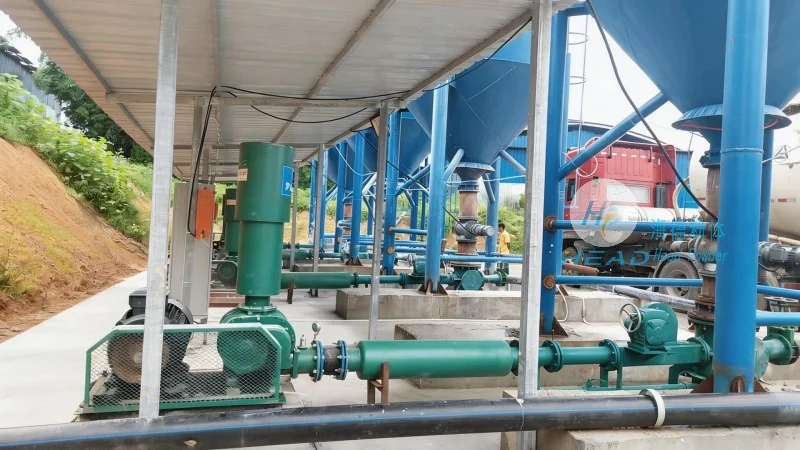
The pneumatic conveying system for sorghum distillers grains has significant applications across various industries, particularly in the food and beverage sector. In the distillery industry, the efficient transport of distillers grains is essential for maintaining the quality of the final alcoholic product and optimizing the overall production process. The system helps in reducing downtime and improving productivity by ensuring a consistent and reliable supply of raw materials to the processing units. Additionally, the enclosed nature of the system helps in maintaining a clean and safe working environment, which is crucial for compliance with industry regulations and standards. The system's ability to handle large volumes of material at high speeds also contributes to cost savings by reducing labor and operational expenses. In summary, the pneumatic conveying system represents a significant advancement in material handling technology, offering a reliable, efficient, and hygienic solution for the transport of sorghum distillers grains. HeadPowder Engineering's expertise in designing and implementing such systems ensures that clients receive a tailored solution that meets their specific needs and enhances their operational performance.