

Principle and Working Scene Characteristics of Ammonium Bicarbonate Material Handling Equipment
Ammonium bicarbonate is a widely used chemical in various industrial applications, and efficient material handling is crucial for its processing and transportation. The equipment designed for handling this specific material plays a vital role in ensuring smooth operations and maintaining product quality. This article explores the underlying principles and operational characteristics of such material handling equipment, providing insights into its design, functionality, and typical application scenarios.
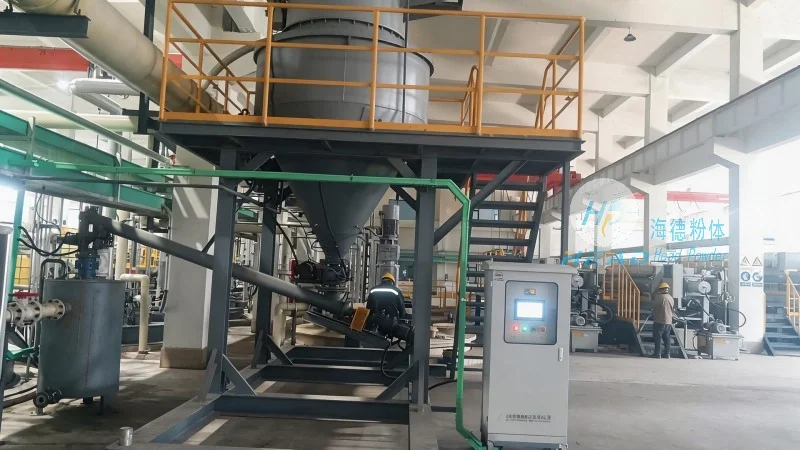
About Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field of chemical processing equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and supplying advanced material handling solutions tailored to the needs of the chemical industry. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses dealing with ammonium bicarbonate and other similar materials. HeadPowder's expertise lies in designing equipment that meets stringent industry standards while optimizing performance and safety.
The Working Principle of Ammonium Bicarbonate Material Handling Equipment
The core of ammonium bicarbonate material handling equipment lies in its ability to transport the material in a controlled and efficient manner. Typically, these systems utilize a combination of mechanical components, such as conveyors, pumps, and storage tanks, to move the material from one location to another. The equipment is engineered to handle the unique properties of ammonium bicarbonate, including its granular or powder form, ensuring minimal degradation or caking during transport. Key components include: conveyor systems that can be customized to different material flow rates, sealable storage vessels to prevent moisture absorption and contamination, and pneumatic or mechanical feeders that regulate the material discharge. The design focuses on maintaining the material's integrity, as ammonium bicarbonate is sensitive to environmental factors like humidity and temperature. By integrating advanced control systems, the equipment can adapt to varying production demands, ensuring consistent output and reducing downtime.
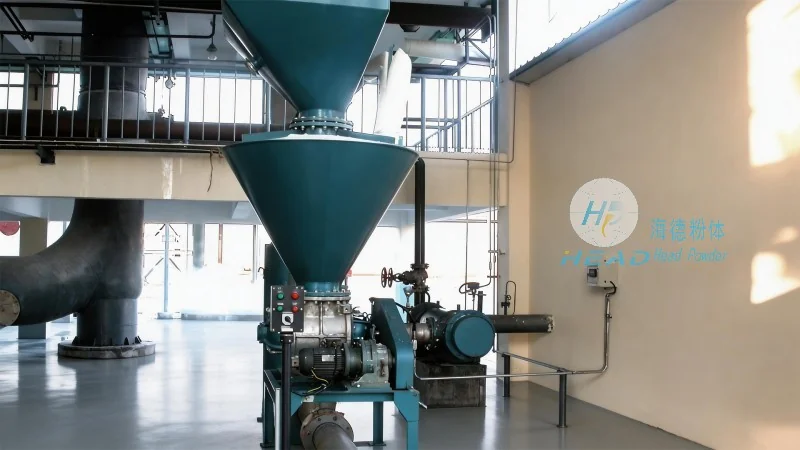
Key Characteristics and Application Scenarios
The operational characteristics of ammonium bicarbonate material handling equipment are tailored to the specific requirements of industrial processes. These characteristics include: high efficiency in material transfer, low maintenance requirements to minimize operational costs, and flexibility to accommodate different production scales. The equipment is commonly used in: chemical manufacturing plants where ammonium bicarbonate is produced or processed, food processing facilities for use in baking and other applications, and agricultural sectors for fertilizer production. In each of these scenarios, the equipment must adhere to strict safety protocols due to the material's potential to release ammonia gas under certain conditions. The design incorporates features like ventilation systems and explosion-proof components to mitigate risks and ensure compliance with safety regulations. Additionally, the equipment is often integrated with automated control systems that allow for real-time monitoring and adjustment, enhancing overall operational efficiency.
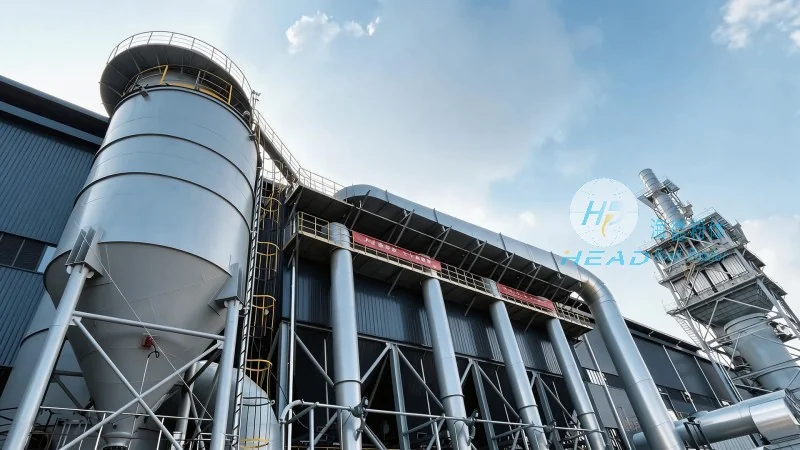
Advantages and Technical Specifications
Ammonium bicarbonate material handling equipment from Shandong HeadPowder offers several advantages that make it a preferred choice for industrial applications. These include: energy efficiency through optimized motor designs and reduced friction, durability with corrosion-resistant materials suitable for chemical environments, and customizability to meet specific client requirements. Technical specifications vary based on the application, but common features include: capacity ranges from small-scale laboratory use to large industrial production, speed control options for precise material flow, and material compatibility with various processing equipment. The equipment is also designed for easy maintenance, with accessible components and standardized parts that simplify repairs and replacements. This focus on reliability and performance ensures that the equipment operates consistently, supporting continuous production cycles and minimizing interruptions.
Conclusion
Ammonium bicarbonate material handling equipment is a critical component in the efficient processing and transportation of this essential chemical. By understanding the underlying principles and operational characteristics, industries can select the most suitable equipment for their specific needs. Shandong HeadPowder Engineering Co., Ltd. provides high-quality solutions that combine advanced technology with practical design, ensuring that clients can achieve optimal performance and safety in their operations. As the demand for ammonium bicarbonate continues to grow, the importance of reliable material handling equipment becomes increasingly evident, making it a key investment for businesses in the chemical and related industries.