

Principles and Application Scenarios of Pneumatic Conveying for Maltodextrin Powders
HeadPowder, a leading provider in the field, specializes in the efficient handling of maltodextrin powders through pneumatic conveying systems. This technology offers a reliable solution for transporting fine powders like maltodextrin, which are commonly used in food, pharmaceutical, and chemical industries. The process involves using air to move the powder particles through a pipeline, ensuring minimal product degradation and contamination.
The Fundamental Principles of Pneumatic Conveying
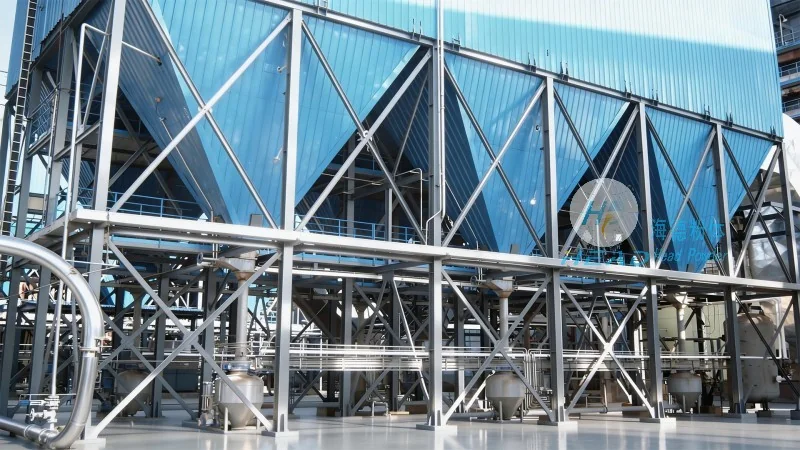
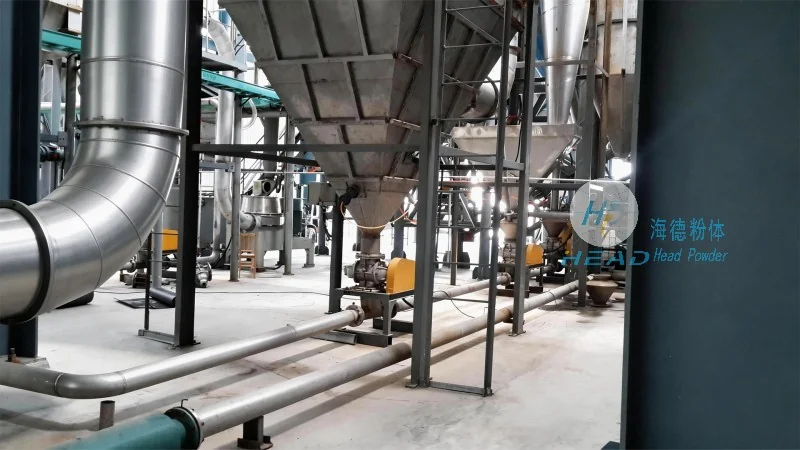
The core principle of pneumatic conveying for maltodextrin powders is the utilization of air pressure to transport the material. There are two main types of systems: dilute-phase and dense-phase. Dilute-phase systems use low air velocity and high air-to-material ratios, suitable for long-distance and high-capacity transport. Dense-phase systems, on the other hand, operate at higher air velocities and lower air-to-material ratios, which are ideal for handling sensitive or abrasive powders. For maltodextrin, a dilute-phase system is often preferred due to its ability to maintain product quality while ensuring efficient transport. The system typically includes a hopper, a rotary valve, a conveyor line, and a receiver. The hopper stores the maltodextrin, the rotary valve controls the flow rate, the conveyor line transports the powder using air, and the receiver collects the material at the destination. This setup ensures a continuous and controlled flow, minimizing the risk of clogging and product loss.
Key Application Scenarios and Advantages
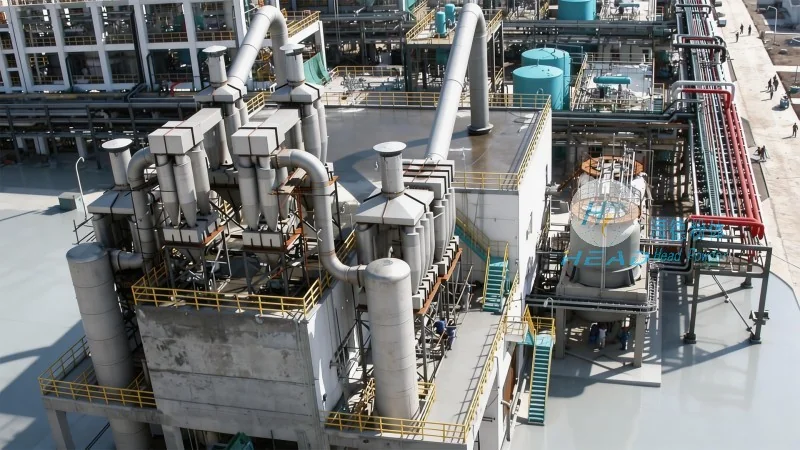
HeadPowder's pneumatic conveying solutions for maltodextrin powders are tailored to various industrial applications. One common scenario is in food processing facilities where maltodextrin is used as a thickening agent or sweetener. The system allows for seamless integration into existing production lines, ensuring that the powder is transported from storage to processing equipment without manual handling. This not only improves operational efficiency but also enhances safety by reducing human exposure to the powder. Another application is in pharmaceutical manufacturing, where the purity and consistency of maltodextrin are critical. Pneumatic conveying minimizes the risk of cross-contamination and maintains the product's quality, which is essential for compliance with regulatory standards. In chemical industries, maltodextrin is used as a raw material in various processes, and the conveying system provides a reliable method to move it from storage to reactors or other processing units. The advantages of this technology include reduced labor costs, improved product quality, and enhanced safety. Additionally, the system can be customized to meet specific operational requirements, such as varying flow rates or distances, making it versatile for different industrial settings.
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a specialized company dedicated to providing advanced powder handling solutions. With years of experience in the industry, HeadPowder has developed expertise in designing and implementing pneumatic conveying systems for a wide range of powders, including maltodextrin. The company's commitment to quality and innovation has enabled it to serve clients across various sectors, from food and pharmaceuticals to chemicals. HeadPowder's team of engineers and technicians works closely with clients to understand their specific needs and provide tailored solutions that meet their operational goals. The company's facilities in Shandong are equipped with state-of-the-art equipment and technology, ensuring that the products and services offered are of the highest quality. By leveraging its expertise and experience, HeadPowder continues to be a trusted partner in the powder handling industry, helping clients optimize their processes and improve overall efficiency.