

Principle and Working Scene Characteristics of Pneumatic Conveying Equipment for Organic Fertilizer
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment tailored for the handling of organic fertilizer granular materials. This article delves into the fundamental principles behind such equipment and highlights the key characteristics of its operational scenarios.
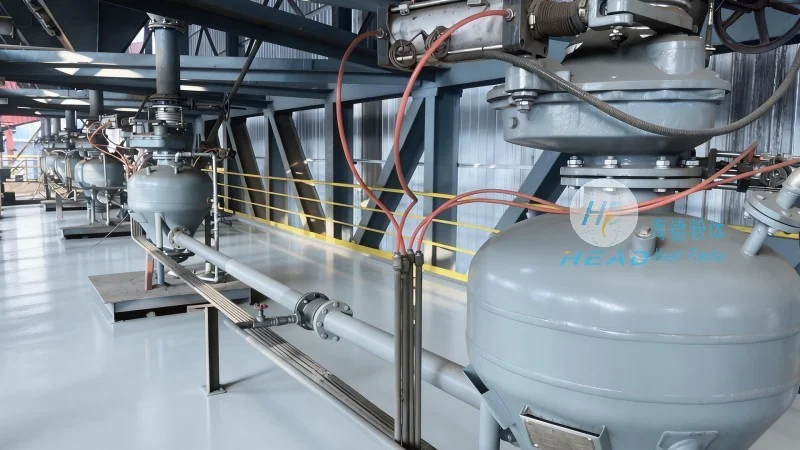
Overview of Pneumatic Conveying Equipment for Organic Fertilizer Granular Materials
Pneumatic conveying systems are essential in the fertilizer industry for efficiently transporting organic fertilizer granules from production sites to storage or processing facilities. These systems utilize air or gas as the conveying medium to move bulk materials through a pipeline network. The core components typically include a material feed hopper, a conveying pipeline, a pressure or vacuum source, and a discharge mechanism. The equipment is engineered to handle the specific physical properties of organic fertilizer granules, such as their size, density, and moisture content, ensuring reliable and low-loss transportation.
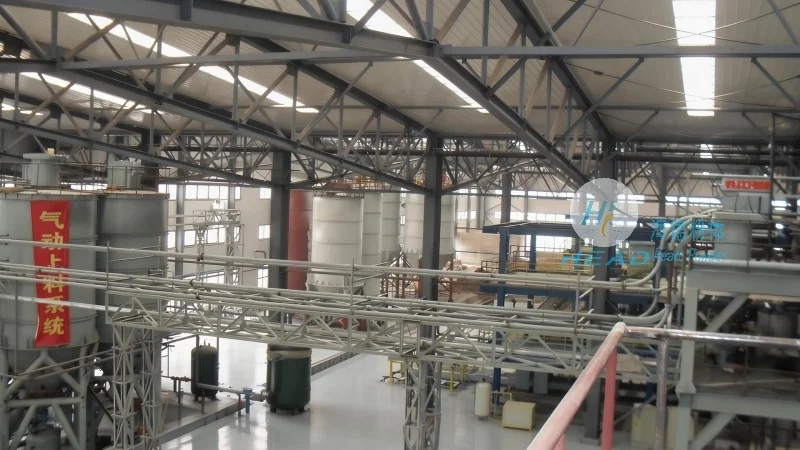
The Working Principle of Pneumatic Conveying Equipment
The operation of pneumatic conveying equipment for organic fertilizer granular materials is based on the principle of fluidization and suspension. When air is introduced into the conveying pipeline at a sufficient velocity, it creates a flow that lifts and transports the granular material. This process involves several key steps: material feeding, air induction, material suspension, and discharge. The feed hopper ensures a consistent supply of granules, while the air source (either positive pressure or negative pressure) generates the necessary airflow to move the material. The conveying pipeline is designed with appropriate diameters and bends to minimize pressure drop and maintain efficient flow. The discharge mechanism, often a rotary valve or a venturi, controls the release of the fertilizer at the destination point.
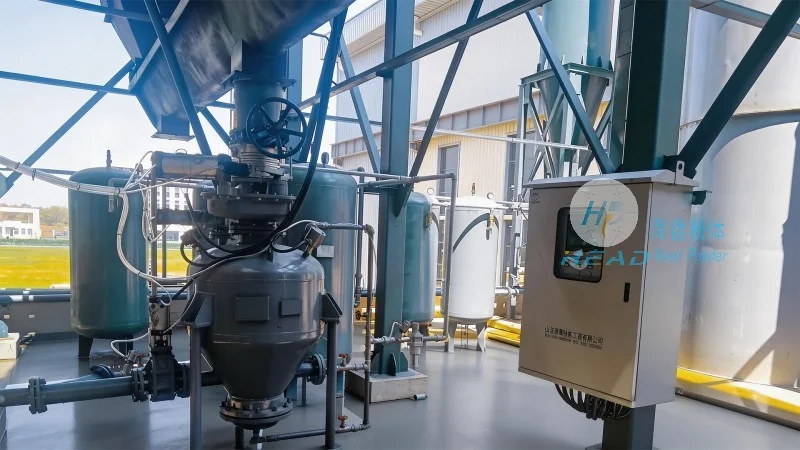
Key Characteristics of Working Scenes for Pneumatic Conveying Equipment
The working scenes of pneumatic conveying equipment for organic fertilizer granular materials are characterized by several factors that influence system performance and efficiency. First, the system must be capable of handling varying particle sizes and shapes, as organic fertilizers often consist of irregularly shaped granules. The equipment is designed with adjustable air velocities and pipeline configurations to accommodate these variations. Second, the moisture content of the fertilizer is a critical factor, as excessive moisture can lead to caking or blockages in the pipeline. The system incorporates moisture control measures, such as pre-drying or moisture-resistant materials, to prevent operational issues. Third, the system is typically integrated into larger production lines, requiring seamless coordination with other equipment like mixers, granulators, and storage silos. The equipment is engineered for high reliability and low maintenance, ensuring continuous operation in industrial settings.
Application Scenarios and Operational Benefits
Pneumatic conveying equipment for organic fertilizer granular materials is widely used in various operational scenarios within the fertilizer industry. One common application is the transfer of granular organic fertilizer from the production line to storage silos or packaging lines. This process requires efficient and hygienic handling to maintain product quality and prevent contamination. The equipment is also utilized in bulk handling operations, where large quantities of fertilizer need to be transported over short or medium distances. The operational benefits of using pneumatic conveying systems include reduced labor costs, minimized material loss, and improved safety compared to traditional methods like manual handling or truck transport. Additionally, the systems are designed to be energy-efficient, with optimized air flow and pressure control to minimize energy consumption.
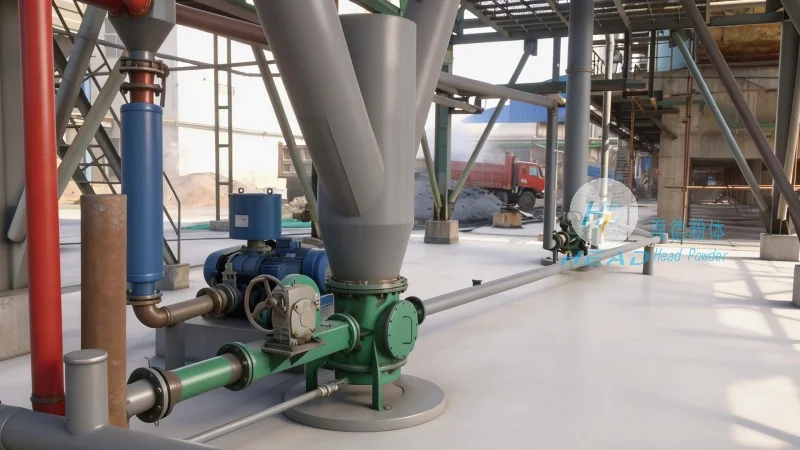
Conclusion and Company Expertise
Shandong HeadPowder Engineering Co., Ltd. has extensive experience in developing and manufacturing pneumatic conveying equipment tailored to the specific needs of the organic fertilizer industry. The company's expertise lies in understanding the unique challenges of handling organic fertilizer granular materials and designing systems that address these challenges effectively. By leveraging advanced engineering and material science, HeadPowder provides reliable and efficient solutions that enhance the productivity and profitability of fertilizer production facilities. The principles and working scene characteristics discussed in this article underscore the importance of specialized equipment in optimizing the handling of organic fertilizers, ensuring that operations run smoothly and efficiently.