

Operation Process and Working Principle of Tonne Bag Unloading Material Conveying System
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling systems. The tonne bag unloading material conveying system is a critical component in various industrial applications, particularly in sectors requiring efficient bulk material transfer from large bags. This system is engineered to streamline the process of unloading, conveying, and processing materials, ensuring high throughput and minimal downtime. By integrating robust mechanical and control technologies, the system enhances operational efficiency and reduces labor costs associated with manual handling of tonne bags.
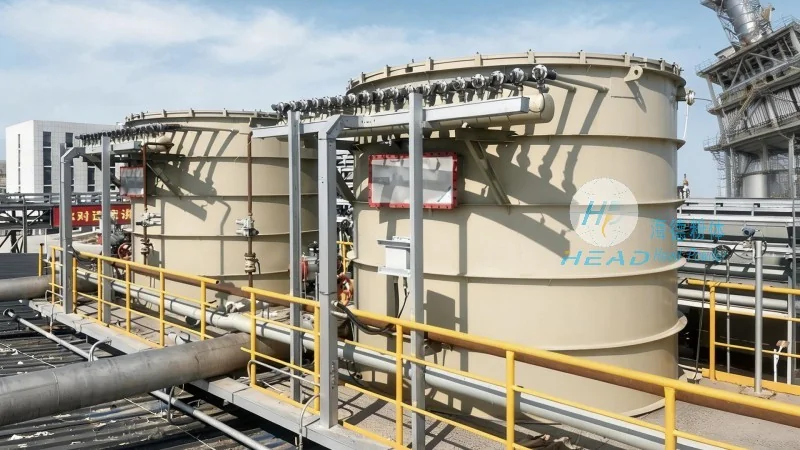
Working Principle of the Tonne Bag Unloading System
The tonne bag unloading material conveying system operates through a series of integrated components that work in tandem to achieve efficient material handling. The process begins with the placement of a tonne bag onto the unloading station. A mechanical or hydraulic mechanism then opens the bag, allowing the contents to flow into a hopper or storage tank. Simultaneously, a conveyor system, typically equipped with a belt or screw mechanism, transports the material from the hopper to the next processing stage. The system may include features such as vibration feeders to regulate the flow rate and prevent blockages, ensuring consistent and controlled material movement. Additionally, the design incorporates safety features to protect operators and equipment from potential hazards, such as overloading or material spillage. Sensors and control units monitor the entire process, providing real-time feedback to maintain optimal performance.
Operation Process of the Material Conveying System
The operation of the tonne bag unloading material conveying system follows a systematic sequence that maximizes efficiency and reliability. First, the tonne bag is positioned on the unloading platform, aligning it with the opening mechanism. The system then activates the bag opening device, which may involve a cutting blade or a pneumatic actuator to release the material. As the bag empties, the material falls into the hopper, where a feeder or conveyor starts to transport it to the subsequent stage. The speed of the conveyor can be adjusted based on the material characteristics and processing requirements, allowing for flexible operation. The system also includes monitoring and control features, such as sensors to detect bag presence or material level, ensuring that the process runs smoothly without interruptions. In the event of an issue, such as a blockage or low material level, the system can automatically pause or alert operators, facilitating quick resolution and minimizing production delays. The integration of automated controls ensures consistent performance, reducing the need for manual intervention and improving overall productivity.
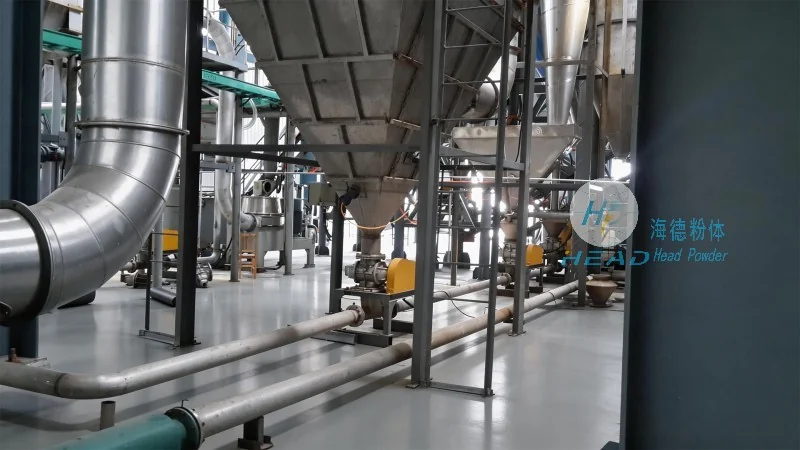
Key Components and Their Functions
The tonne bag unloading material conveying system comprises several key components, each playing a vital role in the overall operation. The bag opening mechanism is responsible for accessing the material inside the tonne bag, while the hopper collects the discharged material. The conveyor system, which may be a belt conveyor or a screw conveyor, transports the material to the next processing stage. Vibration feeders are used to regulate the flow rate, preventing overfilling or blockages. Control panels and sensors monitor the system's operation, providing real-time data and alerts for any issues. The system is designed with durability and ease of maintenance in mind, ensuring long-term reliability and low operational costs.
Application and Industry Use Cases
The tonne bag unloading material conveying system is widely used in industries that handle bulk materials, including chemicals, food processing, and mining. In chemical plants, the system efficiently transfers raw materials from tonne bags to storage tanks, ensuring a continuous supply for production processes. In food processing facilities, the system maintains hygiene standards by handling materials in a controlled environment, reducing contamination risks. Mining operations also benefit from the system's ability to handle large volumes of ore or minerals, improving material handling efficiency and reducing labor requirements. The system's adaptability allows it to be customized for specific industry needs, making it a versatile solution for various material handling challenges.
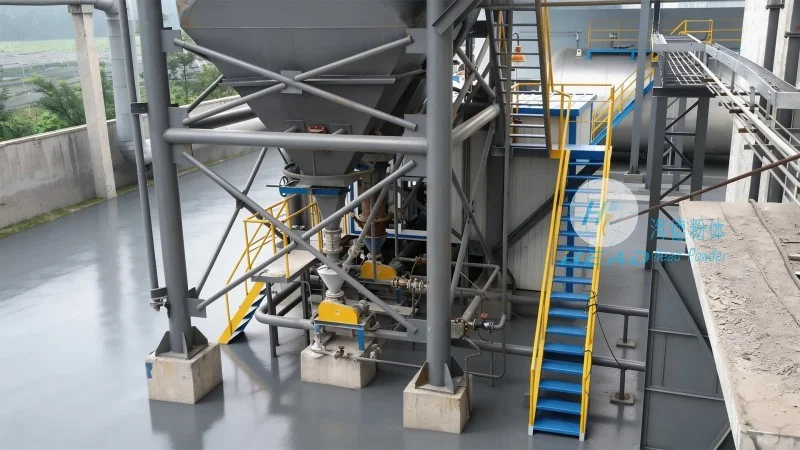
Advantages and Benefits
Implementing the tonne bag unloading material conveying system offers several advantages for industrial operations. The system significantly reduces manual labor, as the process of unloading and conveying materials is automated. This leads to increased productivity and lower labor costs. The system also minimizes material loss and spillage, improving safety and environmental compliance. Additionally, the automated control features ensure consistent material flow, reducing the risk of process interruptions or quality issues. The robust design of the system ensures long-term reliability, with minimal maintenance requirements, resulting in lower operational costs over time. The system's flexibility allows it to be integrated with existing production lines, making it a cost-effective solution for upgrading material handling capabilities.
Conclusion
HeadPowder's tonne bag unloading material conveying system is a sophisticated and efficient solution for bulk material handling in various industrial applications. By combining advanced mechanical design with automated control technologies, the system streamlines the process of unloading, conveying, and processing materials, enhancing operational efficiency and reducing downtime. With its robust construction and flexible operation, the system is well-suited for industries requiring high throughput and reliable material handling. As a leading provider of engineering solutions, HeadPowder continues to innovate and improve its systems to meet the evolving needs of industrial clients, ensuring that their material handling processes remain efficient, safe, and cost-effective.