

Analysis of Sugar Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the sugar industry. This article provides an in-depth analysis of these systems, highlighting their operational principles, benefits, and the technical expertise of Shandong HeadPowder Engineering Co., Ltd.
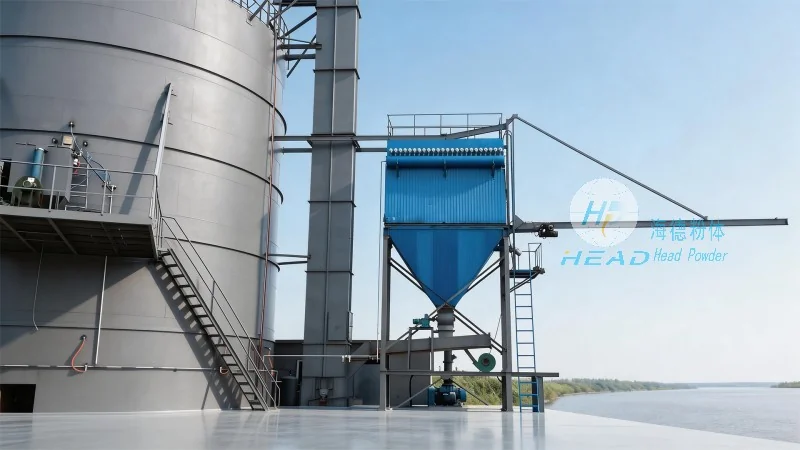
Understanding Pneumatic Conveying in Sugar Processing
Pneumatic conveying systems are widely used in the sugar industry to transport raw sugar, refined sugar, and other sugar-related products from one processing stage to another. These systems utilize air or other gases to move bulk materials through a pipeline network, eliminating the need for traditional mechanical conveyors such as belts or buckets. The technology offers several advantages, including reduced labor costs, minimized product contamination, and enhanced process efficiency.
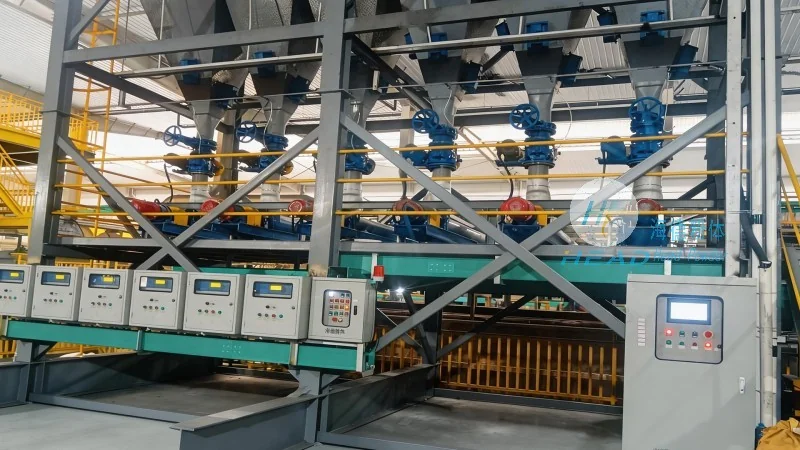
Key Components of a Sugar Pneumatic Conveying System
A typical sugar pneumatic conveying system consists of several critical components that work in tandem to ensure smooth material transport. These include the feed hopper, which holds the sugar and regulates the flow into the system; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying line, which is usually made of stainless steel to prevent corrosion and maintain hygiene standards; and the discharge hopper or silo, where the sugar is collected at the end of the process. Additionally, control systems and monitoring equipment are integrated to optimize performance and ensure safety.
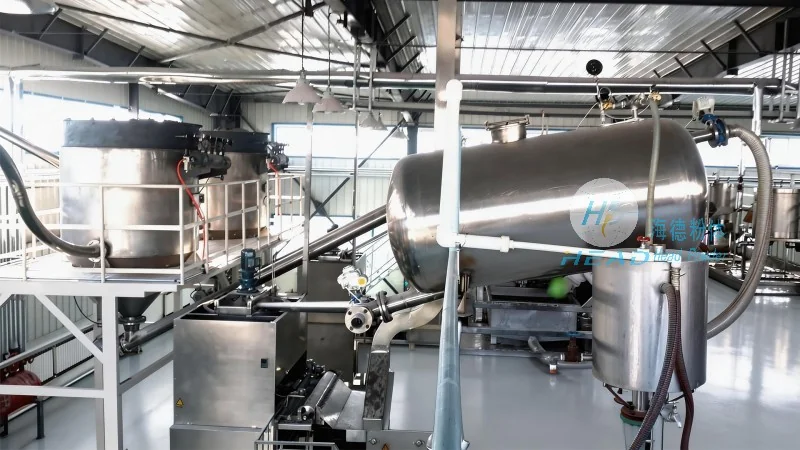
Advantages of Pneumatic Conveying for Sugar Handling
Implementing pneumatic conveying systems in sugar processing facilities offers numerous benefits. First, it significantly reduces the risk of product contamination, as the material is enclosed within the pipeline, preventing exposure to dust, moisture, or other external factors. Second, the system minimizes labor requirements by automating the material transport process, allowing workers to focus on other critical tasks. Third, it enhances process efficiency by enabling faster and more consistent material movement, which is crucial for maintaining production schedules and meeting quality standards. Furthermore, pneumatic conveying systems are flexible and can be easily adapted to accommodate changes in production volume or product types.
Technical Expertise of Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, brings extensive experience and technical expertise to the design and installation of sugar pneumatic conveying systems. The company’s engineers leverage advanced engineering principles and industry best practices to develop customized solutions that meet the specific needs of each client. By focusing on material flow analysis, system sizing, and equipment selection, HeadPowder ensures that its systems are optimized for performance, reliability, and cost-effectiveness. The company also provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure the long-term operation of the conveying systems.
Conclusion and Application Scope
In conclusion, pneumatic conveying systems represent a highly effective and efficient solution for transporting sugar and related products in processing facilities. The technology offers significant advantages over traditional methods, including improved hygiene, reduced labor costs, and enhanced operational flexibility. With its commitment to quality and technical excellence, Shandong HeadPowder Engineering Co., Ltd. is well-positioned to provide reliable and customized pneumatic conveying solutions for the sugar industry. Whether for new installations or system upgrades, HeadPowder’s expertise ensures that clients achieve optimal performance and productivity in their sugar processing operations.