

Analysis of Silica Fume Pneumatic Conveying Systems
Silica fume, also known as microsilica, is a fine powder derived from the production of silicon metal or ferrosilicon alloys. It is characterized by its high surface area and unique chemical properties, making it a valuable additive in concrete, refractory materials, and other industrial applications. The efficient handling and transportation of silica fume are critical for maintaining product quality and operational efficiency in industrial processes. Pneumatic conveying systems have become a preferred method for transporting this fine powder due to their ability to handle abrasive materials and minimize dust emissions.
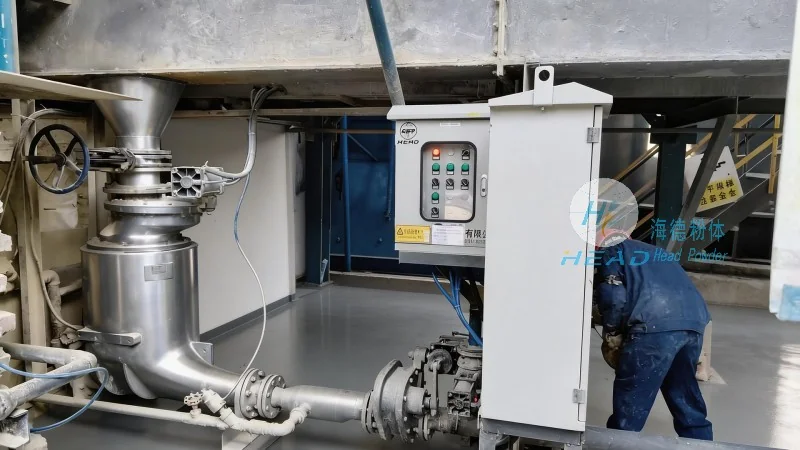
HeadPowder: A Leading Provider of Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a specialized engineering company headquartered in Shandong, China. With decades of experience in material handling and conveying systems, HeadPowder has established itself as a trusted provider of pneumatic conveying solutions tailored to the specific needs of silica fume and other fine powders. The company’s commitment to quality, innovation, and customer satisfaction has positioned it as a key player in the industry, offering customized systems that enhance operational performance and ensure compliance with industry standards.
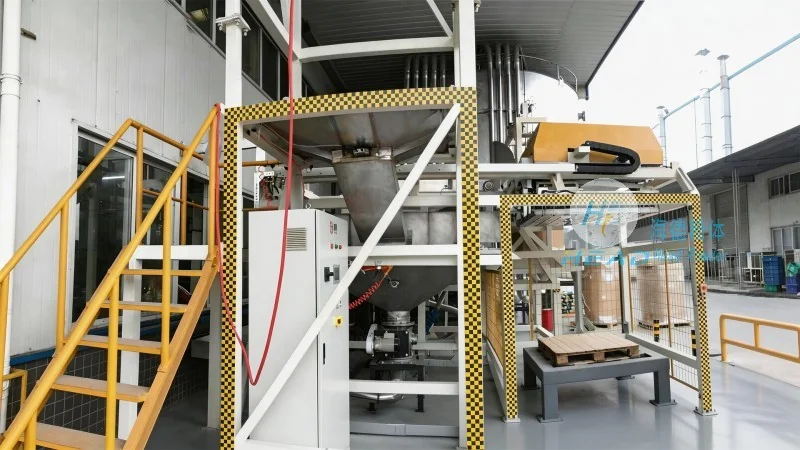
Key Components and Operational Principles
The pneumatic conveying system for silica fume typically comprises several essential components, including a hopper for material storage, a feeder to control the flow rate, an air compressor to generate the conveying air, a pipeline network to transport the material, and a receiver for the final product. The system operates by using compressed air to create a flow that propels the silica fume particles through the pipeline. Key operational principles include:
- Pressure-Driven Conveying: Systems can be designed for either low-pressure (around 0.5 to 1 bar) or high-pressure (5 to 10 bar) operation, depending on the distance between the source and destination and the material’s characteristics.
- Abrasion Resistance: Critical components such as hoppers, pipelines, and valves are constructed from durable materials like stainless steel, polyurethane, or specialized alloys to withstand the abrasive nature of silica fume and extend the system’s lifespan.
- Dust Control: Advanced filtration systems and sealed designs are integrated to minimize dust emissions, ensuring a safe working environment and compliance with environmental regulations.
- Customization: HeadPowder offers tailored solutions to accommodate varying production capacities, conveying distances, and integration with existing industrial facilities.
Applications and Benefits in Industrial Settings
Silica fume pneumatic conveying systems are widely utilized across various industries, including construction, refractory manufacturing, and chemical processing. The benefits of implementing such systems include:
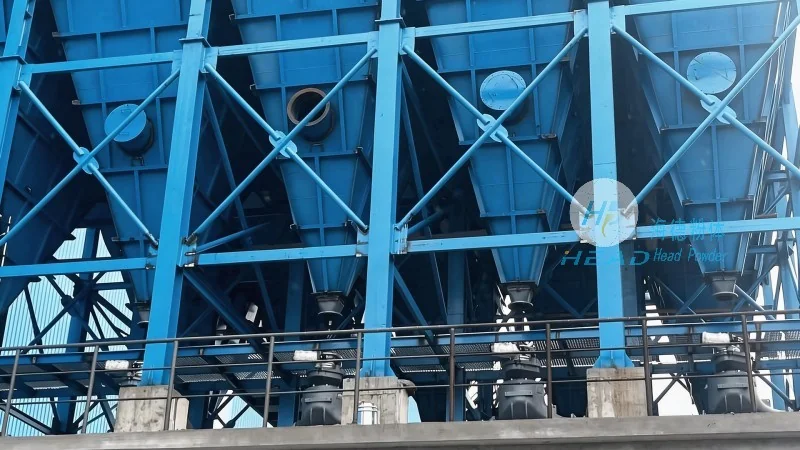
- Preservation of Product Quality: By preventing material degradation, contamination, or agglomeration, the system ensures that the silica fume delivered to processing plants retains its high-quality attributes, which are essential for optimal performance in end products.
- Increased Operational Efficiency: Automated and continuous operation reduces labor costs, minimizes downtime, and enhances overall productivity, allowing companies to meet production targets more effectively.
- Reduced Maintenance Costs: Well-designed systems with robust components require less frequent maintenance, leading to lower long-term operational expenses and higher system reliability.
- Environmental Compliance: Effective dust control measures help companies avoid environmental penalties and maintain a positive corporate image by adhering to environmental regulations.
Conclusion
For industries that rely on silica fume, the selection of an efficient pneumatic conveying system is paramount to maintaining product integrity and operational efficiency. HeadPowder, with its expertise in engineering and manufacturing, provides reliable and customized solutions that meet the demanding requirements of silica fume handling. By leveraging advanced technology and high-quality materials, these systems ensure safe, clean, and efficient transport of silica fume, supporting the success and sustainability of industrial operations worldwide.