

Introduction to Phosphate Iron Transport Systems and the Advantages of Phosphate Iron Pneumatic Conv
Phosphate iron, a vital raw material in numerous industrial sectors, demands efficient and dependable transport solutions to support seamless production workflows. Shandong HeadPowder Engineering Co., Ltd., a leading entity in the field, specializes in designing and implementing advanced phosphate iron transport systems. This article offers an overview of these systems, detailing their components, operational principles, and the key benefits they provide for handling phosphate iron.
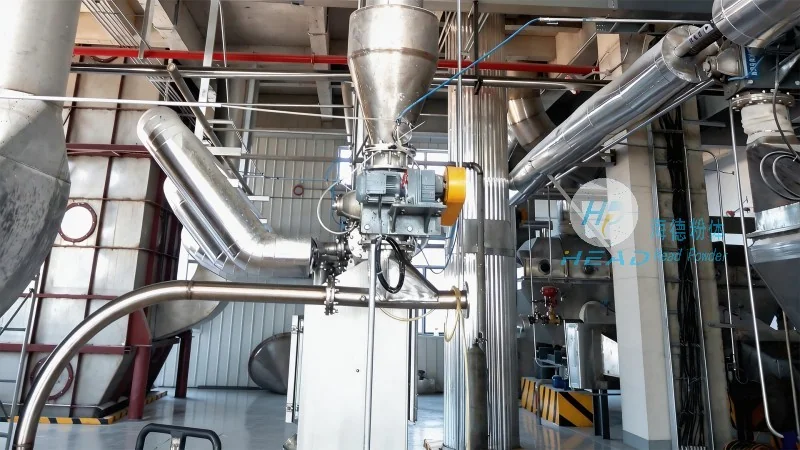
Core Components of Phosphate Iron Transport Systems
Phosphate iron transport systems typically comprise several essential elements that collaborate to move material. The primary components include feed hoppers, pneumatic conveying lines, control valves, and receiving silos. Feed hoppers are engineered to store and meter phosphate iron, ensuring a consistent flow into the conveying system. Pneumatic conveying lines, often equipped with airlocks and cyclones, utilize compressed air to transport the material through the system. Control valves regulate air flow and material discharge, while receiving silos store the transported phosphate iron for subsequent processing. Each component is constructed to endure the abrasive nature of phosphate iron, ensuring long-term durability and minimal maintenance.
The Advantages of Pneumatic Conveying for Phosphate Iron
Compared to conventional bulk material handling methods, pneumatic conveying offers distinct advantages for transporting phosphate iron. One of the most significant benefits is its capability to handle fine and dusty materials without mechanical components that can cause wear and tear, reducing maintenance costs and extending operational life. Additionally, pneumatic conveying systems are highly flexible, allowing easy integration into existing production lines and modifications to accommodate changing production volumes. The enclosed system design minimizes dust emissions, enhancing workplace safety and environmental compliance. Furthermore, these systems can transport phosphate iron over extended distances with minimal loss, making them ideal for large-scale industrial applications.
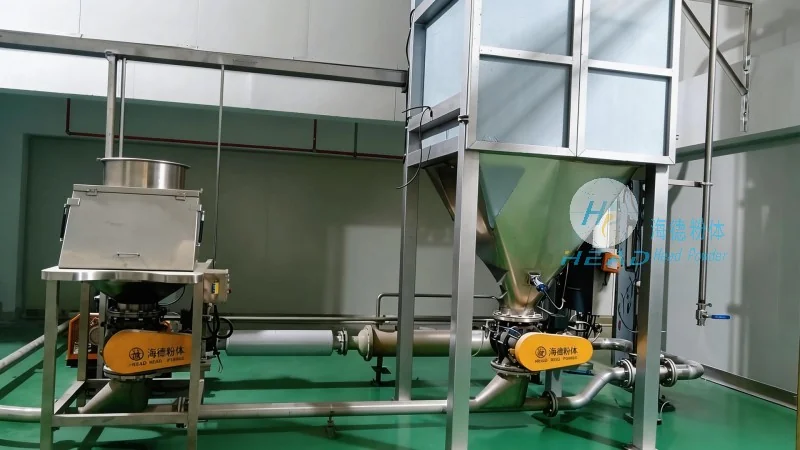
Operational Efficiency and Cost-Effectiveness
Efficiency and cost-effectiveness are critical in industrial operations, and phosphate iron transport systems from Shandong HeadPowder Engineering Co., Ltd. excel in these areas. The pneumatic conveying technology ensures a continuous and reliable material flow, reducing downtime and increasing overall productivity. By minimizing manual handling and material loss, the systems lower operational costs over time. The robust design of components like feed hoppers and conveying lines allows high-capacity operation without compromising performance. This efficiency is particularly beneficial for high-volume phosphate iron operations, enabling consistent production rates and optimized resource utilization.
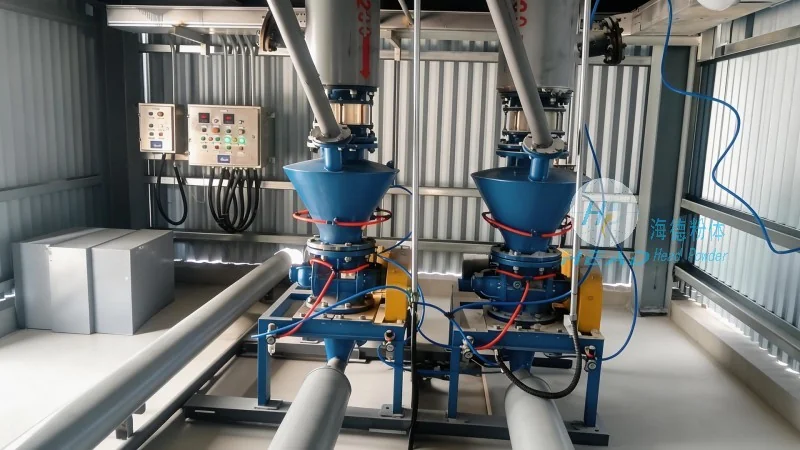
Customization and Scalability
Every industrial facility has unique requirements, and Shandong HeadPowder Engineering Co., Ltd. emphasizes customization in delivering effective transport solutions. The company offers tailored phosphate iron transport systems scaled to meet specific application needs—whether small-scale or large industrial plants. The modular component design allows easy expansion or modification as production evolves. This scalability ensures long-term relevance and return on investment, justifying initial costs.
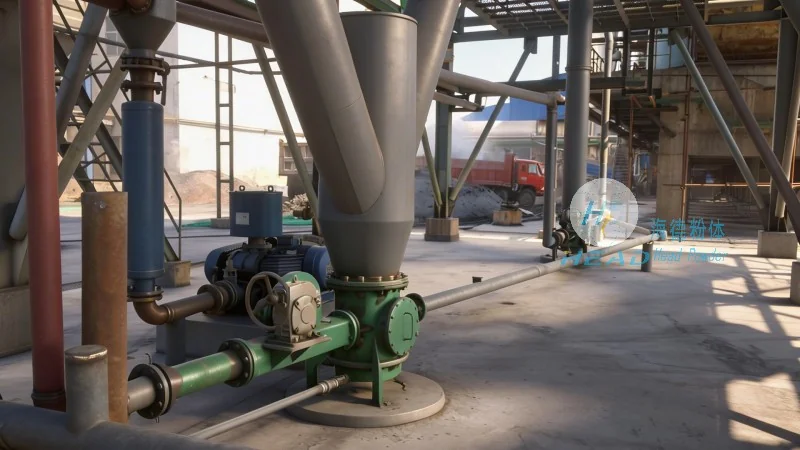
Reliability and Maintenance
Reliability is paramount in industrial systems, and phosphate iron transport systems from Shandong HeadPowder Engineering Co., Ltd. are built for consistent performance. High-quality materials and precision engineering withstand harsh phosphate iron handling conditions. Features like self-cleaning airlocks and low-wear components minimize regular maintenance. The company provides comprehensive maintenance services and spare parts support to keep systems operational. This reliability is essential for maintaining production schedules and avoiding supply chain disruptions.
Conclusion
Phosphate iron transport systems, especially those using pneumatic conveying, offer significant benefits for handling this critical raw material. Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider, combining advanced engineering with practical application to meet diverse industry needs. By focusing on efficiency, reliability, and customization, the company ensures clients achieve optimal performance in phosphate iron handling. For businesses seeking enhanced material transport capabilities, the phosphate iron transport systems from Shandong HeadPowder Engineering Co., Ltd. represent a reliable and effective solution.