

Introduction to Aggregate Conveying Systems and the Advantages of Pneumatic Conveying for Aggregates
Aggregate conveying systems are essential in industries like construction and mining, where the efficient movement of bulk materials such as sand, gravel, and crushed stone is critical for operational success. These systems are designed to transport materials from storage areas to processing facilities or other work sites, streamlining material handling processes and reducing downtime. The technology behind these systems has advanced significantly, with pneumatic conveying emerging as a preferred method due to its efficiency and adaptability.
Components and Functionality of Aggregate Conveying Systems
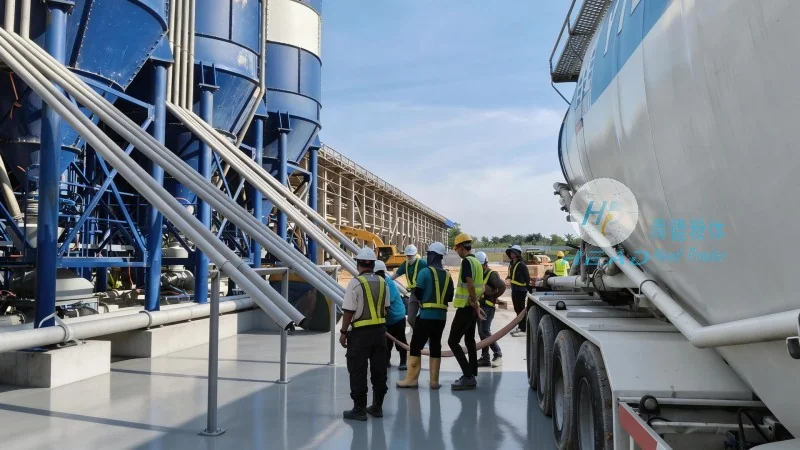
Aggregate conveying systems typically consist of several key components that work together to facilitate material transport. The primary components include hoppers, which store and feed the material; feeders, which control the flow rate; pipelines, which transport the material; and control systems, which regulate the operation. Hoppers are designed to hold large quantities of material and ensure a consistent feed to the feeder. Feeders, such as rotary valves or vibratory feeders, regulate the material flow into the pipeline, preventing overloading and ensuring smooth operation. The pipelines, often made of stainless steel or other corrosion-resistant materials, are designed to withstand the pressure and friction of the material being conveyed. Control systems, including sensors and valves, monitor and adjust the system's operation to maintain optimal performance. Together, these components create a seamless material handling process that minimizes manual intervention and maximizes efficiency.
Pneumatic Conveying: A Superior Method for Aggregate Transport
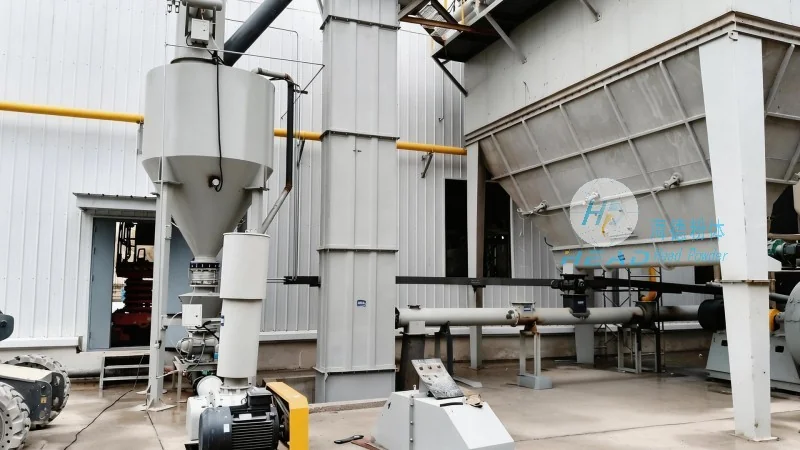
Pneumatic conveying, or air conveying, is a technology that uses compressed air to transport dry bulk materials through a pipeline. This method offers several advantages over traditional mechanical conveying systems, such as belt conveyors or bucket elevators. One of the main benefits is the ability to handle a wide range of materials, including fine powders and coarse aggregates, without causing segregation or degradation. Unlike mechanical systems, which can cause material breakdown or separation, pneumatic conveying maintains the integrity of the aggregates, ensuring consistent quality. Another advantage is the reduced risk of dust exposure. The sealed pipeline system prevents dust from escaping into the environment, improving workplace safety and compliance with environmental regulations. Additionally, pneumatic conveyors can transport materials over long distances with minimal energy consumption, making them more cost-effective compared to other methods. The flexibility of pneumatic systems also allows for easy integration with other processing equipment, such as mixers or classifiers, creating a seamless workflow that enhances overall productivity.
Advantages of Pneumatic Conveying in Aggregate Handling
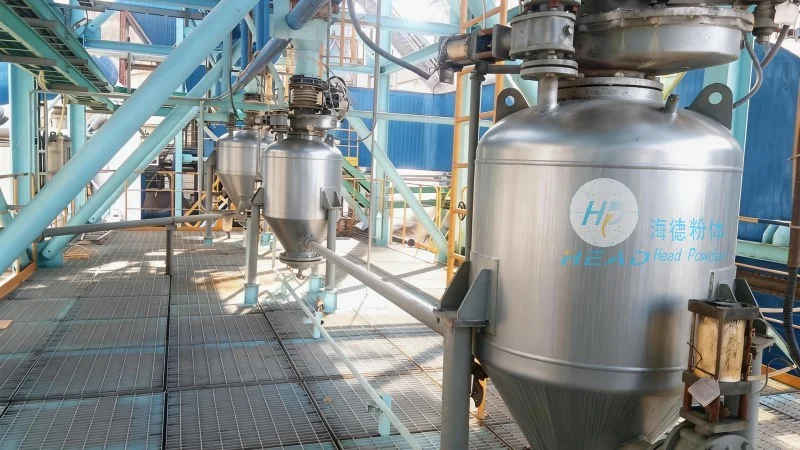
When evaluating pneumatic conveying for aggregate handling, several key advantages stand out. Firstly, the system's ability to transport materials in a closed environment reduces the risk of contamination and ensures the quality of the aggregates remains intact. This is particularly important in applications where material purity is critical, such as in concrete production or mining operations. Secondly, pneumatic conveyors are generally more energy-efficient than mechanical systems. By utilizing existing compressed air infrastructure, businesses can reduce energy costs and lower their carbon footprint. Thirdly, the system's scalability allows for easy expansion or reconfiguration as operational needs change. This flexibility is valuable for growing businesses or those with fluctuating material volumes. Furthermore, pneumatic conveying systems are less prone to maintenance issues compared to mechanical systems, as they have fewer moving parts and require less frequent servicing. This leads to lower maintenance costs and increased system reliability over time.
HeadPowder Engineering: Delivering Customized Aggregate Conveying Solutions
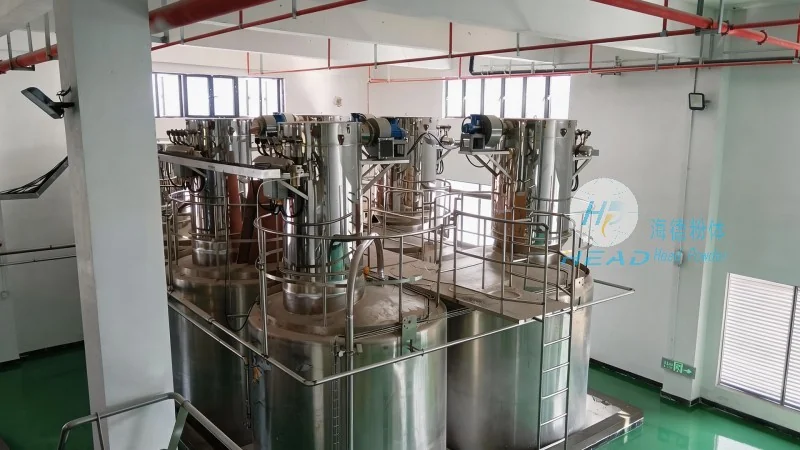
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of engineering solutions specializing in aggregate conveying systems. With a strong presence in China, HeadPowder has built a reputation for delivering high-quality, reliable systems tailored to the unique needs of its clients. The company's team of experienced engineers and technicians leverages advanced technology and industry expertise to design and manufacture customized pneumatic conveying solutions. HeadPowder's commitment to quality is evident in its rigorous testing and quality control processes, ensuring that every system meets or exceeds industry standards. The company also provides comprehensive after-sales support, including installation, maintenance, and training, to help clients maximize the performance and lifespan of their equipment. By partnering with HeadPowder, businesses can benefit from expert guidance in system selection, design, and implementation, ensuring that their material handling operations are optimized for efficiency and productivity. HeadPowder's focus on customer satisfaction and long-term partnerships has made it a trusted name in the industry, helping clients achieve their operational goals and stay competitive in their respective markets.