

Introduction to Nanoparticle Calcium Carbonate Conveying Systems: Advantages and Features of Pneumat
For industries dealing with nanoparticle calcium carbonate, the efficient and reliable transportation of this fine material is crucial. The choice of a suitable conveying system can significantly impact production efficiency, material quality, and operational costs. This article introduces the nanoparticle calcium carbonate conveying system, highlighting the advantages and key features of pneumatic conveying technology as a preferred solution.
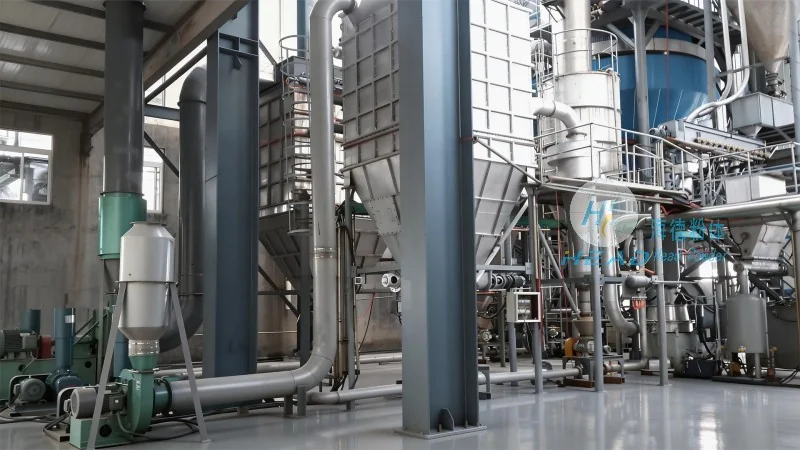
Overview of the Nanoparticle Calcium Carbonate Conveying System
The nanoparticle calcium carbonate conveying system is a specialized setup designed to handle the unique properties of nanoscale calcium carbonate particles. These particles, with their small size and high surface area, present challenges in traditional bulk material handling, such as dust generation, caking, and blockage in pipelines. The system addresses these challenges by integrating advanced pneumatic conveying technology, ensuring smooth and safe material transport from storage to processing units.
Key Components of the Conveying System
The conveying system typically consists of several critical components that work in tandem to achieve efficient material transport. These include a hopper or storage silo for material storage, a feeder to control the flow rate, a conveying line (often with multiple sections), and a receiver or discharge unit. The system may also incorporate auxiliary equipment like filters, dust collectors, and pressure regulators to maintain optimal operating conditions and ensure environmental compliance.
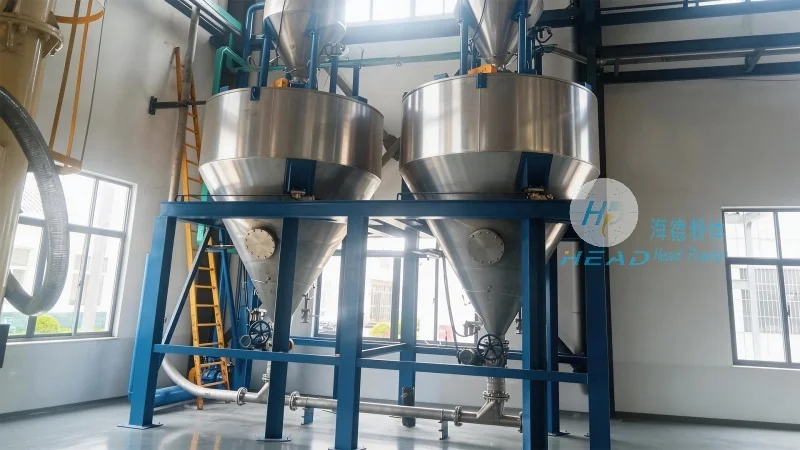
Advantages of Pneumatic Conveying for Nanocalcium Carbonate
Pneumatic conveying, particularly in the form of dense-phase or dilute-phase systems, offers several advantages for transporting nanoparticle calcium carbonate. One of the primary benefits is the ability to handle fine powders without the need for mechanical components that could cause particle degradation or blockage. The system minimizes material loss and contamination, as the material is enclosed within the conveying line, reducing exposure to external elements. Additionally, pneumatic conveying allows for flexible routing, enabling the material to be transported to multiple destinations from a single source, enhancing operational flexibility.
Enhanced Material Handling Efficiency
The nanoparticle calcium carbonate conveying system significantly improves material handling efficiency by reducing downtime and labor costs. By automating the transport process, the system minimizes manual handling, which is not only safer but also more consistent. The controlled flow rates and pressure management in the system prevent overloading or underloading of processing equipment, ensuring stable production output. This efficiency is further enhanced by the system's ability to handle varying material feed rates, adapting to different production demands without compromising performance.
Quality Preservation and Environmental Compliance
Another critical aspect of the conveying system is its role in preserving the quality of nanoparticle calcium carbonate. The enclosed pneumatic conveying process prevents contamination from moisture, air, or other substances, maintaining the material's purity and performance characteristics. This is especially important for applications where the material's surface properties and particle size distribution are critical, such as in plastics, coatings, and paper manufacturing. The system also includes dust collection and filtration components, ensuring compliance with environmental regulations and providing a safer working environment for personnel.
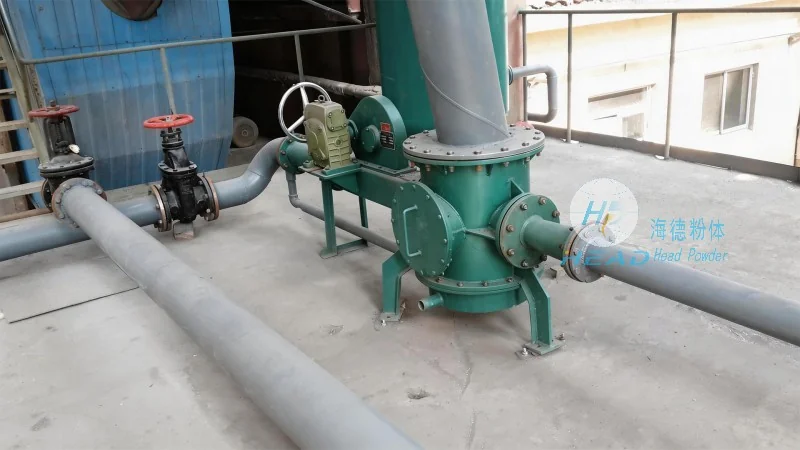
Customization and Scalability for Industrial Needs
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, offers customized nanoparticle calcium carbonate conveying systems tailored to specific industrial requirements. The company's expertise in engineering and manufacturing allows for the design of systems that can be scaled to meet the needs of small-scale operations as well as large industrial facilities. Whether for a new plant or an upgrade to an existing system, the company's solutions are designed to integrate seamlessly with existing infrastructure while delivering optimal performance. The systems are built with high-quality materials and components to ensure durability and long-term reliability, reducing maintenance costs and extending the system's operational life.
Conclusion
In conclusion, the nanoparticle calcium carbonate conveying system, particularly utilizing pneumatic conveying technology, is an essential component for industries dealing with nanoscale calcium carbonate. The system's ability to handle fine powders efficiently, preserve material quality, and ensure environmental compliance makes it a preferred choice over traditional methods. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., industries can implement advanced conveying solutions that enhance productivity, reduce costs, and maintain the highest standards of material handling. As the demand for high-quality nanoparticle calcium carbonate continues to grow, the importance of reliable and efficient conveying systems will only increase, making this technology a critical investment for future success.