

Introduction to Desulfurization and Denitrification Agent Delivery Systems, Advantages and Features
Desulfurization and denitrification agents are critical components in modern industrial processes, particularly in power generation and chemical manufacturing. The efficient and reliable delivery of these agents is essential for maintaining optimal performance and environmental compliance. This article introduces the desulfurization and denitrification agent delivery systems, with a focus on the advantages and features of pneumatic conveying technology.
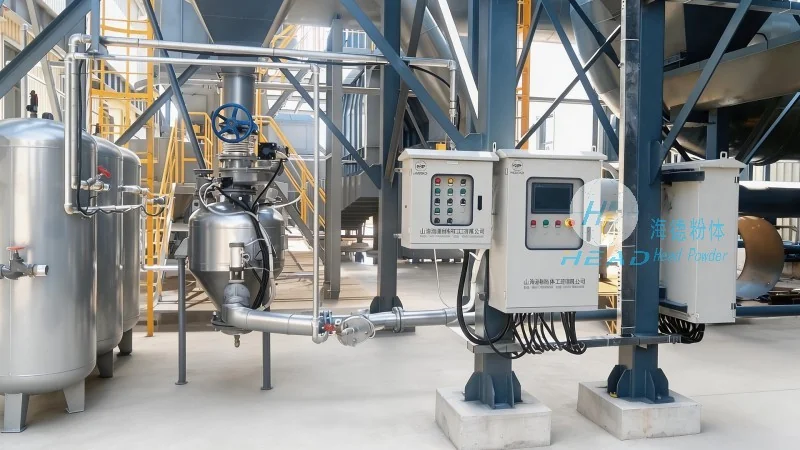
Overview of Desulfurization and Denitrification Agent Delivery Systems
Desulfurization and denitrification agents, such as limestone slurry or urea, are typically stored in bulk containers and need to be transported to reactors or injection points. Traditional methods like gravity flow or mechanical pumps may face challenges with abrasive or corrosive materials, leading to equipment wear and operational inefficiencies. Pneumatic conveying systems offer a solution by using air or gas to transport these agents, providing a flexible and effective method for material handling.
HeadPowder Engineering: A Leading Provider of Delivery Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company specializing in the design and manufacturing of advanced material handling systems. With a strong presence in China, particularly in Shandong, HeadPowder has established itself as a trusted partner for industries requiring reliable desulfurization and denitrification agent delivery solutions. The company's expertise lies in customizing systems to meet specific operational requirements, ensuring durability and performance under harsh conditions.
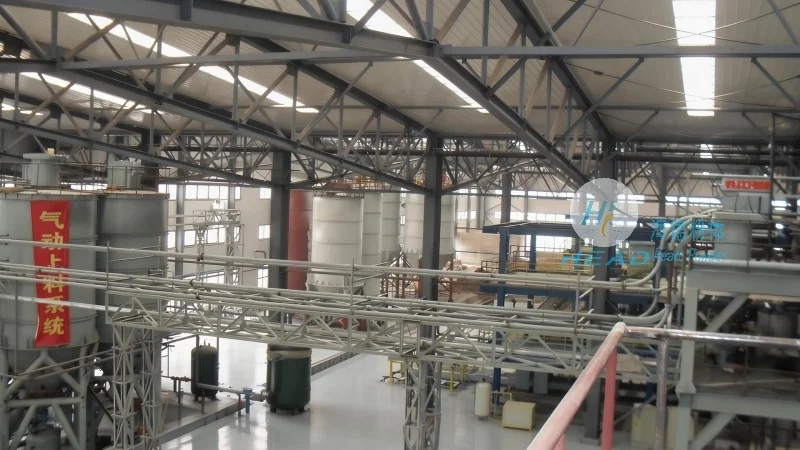
Pneumatic Conveying: Key Advantages for Agent Delivery
Pneumatic conveying technology offers several advantages over conventional methods. First, it provides a closed system, which helps prevent dust emissions and contamination, aligning with environmental regulations. Second, the system can handle a wide range of particle sizes and densities, making it suitable for various desulfurization and denitrification agents. Third, pneumatic conveyors are generally more compact and easier to integrate into existing plant layouts compared to other bulk handling solutions. Additionally, the technology allows for precise control over flow rates and pressure, ensuring consistent delivery to the target points.
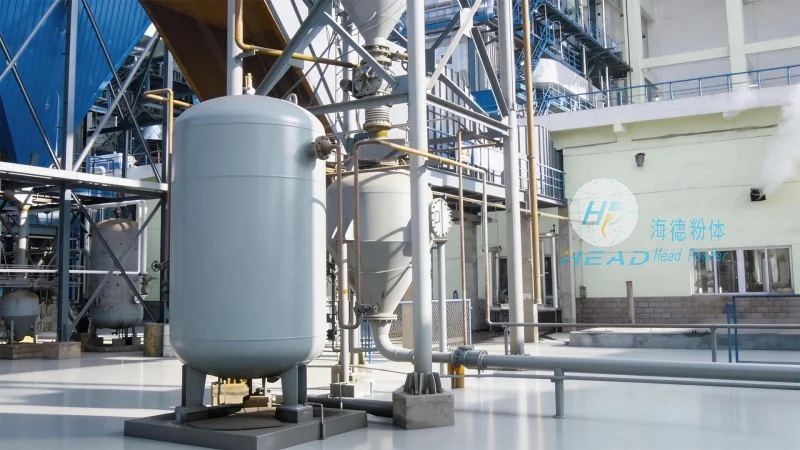
Key Features of Pneumatic Conveying Systems for Desulfurization and Denitrification Agents
Modern pneumatic conveying systems for desulfurization and denitrification agents incorporate several key features to enhance performance and reliability. These include high-efficiency air compressors that minimize energy consumption, robust material handling components such as rotary valves and feeders that withstand abrasive agents, and advanced control systems that monitor and adjust the conveying process in real-time. The systems are also designed with corrosion-resistant materials to handle the chemical properties of the agents, extending their service life and reducing maintenance costs.
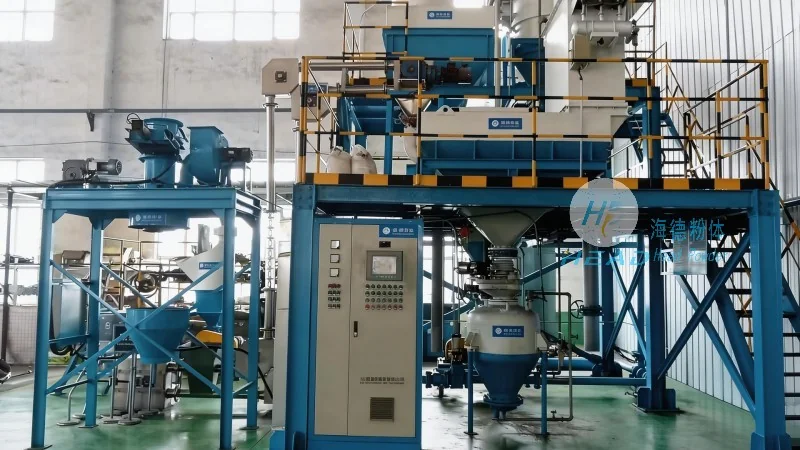
Application Examples and Operational Benefits
The application of pneumatic conveying systems in desulfurization and denitrification processes has yielded significant operational benefits. For instance, in power plants, these systems enable the efficient transport of limestone slurry to scrubbers, improving the overall efficiency of flue gas treatment. In chemical manufacturing, the technology ensures consistent delivery of urea or other reagents to reactors, enhancing product quality and reducing downtime. The closed-loop design of the systems also minimizes material loss and waste, contributing to cost savings and environmental sustainability.
Conclusion and Future Outlook
In conclusion, desulfurization and denitrification agent delivery systems, particularly those utilizing pneumatic conveying technology, play a vital role in modern industrial operations. The combination of advanced engineering, robust materials, and precise control ensures that these systems deliver reliable performance while meeting stringent environmental and operational standards. As industries continue to prioritize efficiency and sustainability, the demand for sophisticated material handling solutions like those offered by HeadPowder is expected to grow, supporting the development of cleaner and more efficient processes worldwide.