

Working Principle and Features of Ammonium Bicarbonate Material Handling
Ammonium bicarbonate, a widely used chemical in various industrial applications, requires efficient and reliable material handling systems to ensure smooth operations. This article delves into the working principle and key features of the material handling processes for ammonium bicarbonate, highlighting the technological advancements and operational benefits that modern systems offer.
Understanding the Working Principle of Ammonium Bicarbonate Material Handling
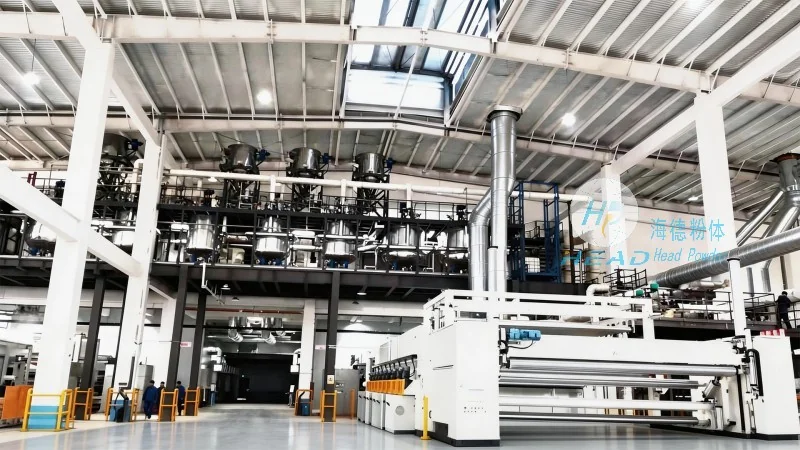
The material handling of ammonium bicarbonate typically involves a series of steps designed to manage the chemical's properties, such as its reactivity and handling characteristics. The process begins with the storage of the material in specialized containers, often equipped with temperature and humidity controls to maintain the product's stability. From there, the material is transferred through a network of conveyor systems, pneumatic conveyors, or bulk handling equipment, depending on the specific application and scale of operation.
One of the core components in the material handling system is the conveyor technology, which may include belt conveyors, screw conveyors, or bucket elevators. These systems are engineered to handle the flow of ammonium bicarbonate while minimizing the risk of caking or agglomeration, which can occur due to the material's hygroscopic nature. The design of these conveyors often incorporates features like anti-static coatings and smooth surfaces to prevent material buildup and ensure consistent throughput.
Key Features of Ammonium Bicarbonate Material Handling Systems
Modern ammonium bicarbonate material handling systems are characterized by several key features that enhance efficiency, safety, and product quality. Firstly, the systems are equipped with advanced control mechanisms that allow for precise regulation of flow rates and material movement. This is crucial for maintaining consistent product quality and preventing overloading or underloading of processing equipment.
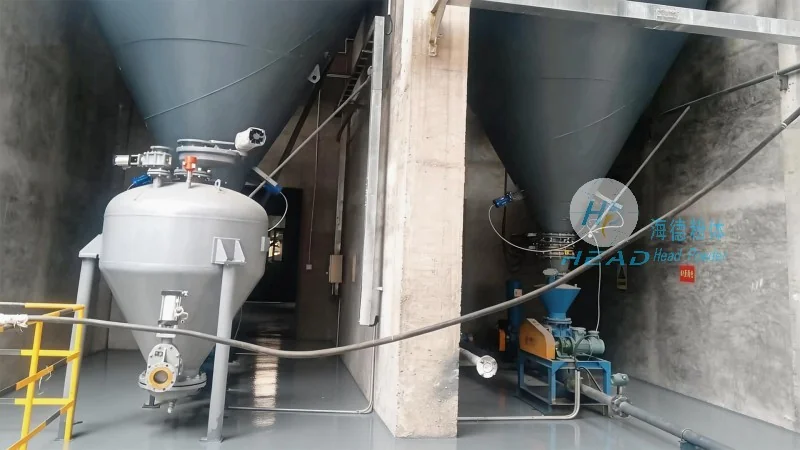
Secondly, the use of dust suppression and containment measures is a critical feature. Ammonium bicarbonate is a fine powder that can generate significant dust during handling, posing health and safety risks. Advanced systems incorporate dust collection systems, sealed conveyor sections, and explosion-proof designs to mitigate these risks and comply with environmental regulations.
Thirdly, the integration of monitoring and diagnostic tools provides real-time insights into the system's performance. Sensors and data loggers track parameters such as temperature, pressure, and flow rates, enabling proactive maintenance and reducing downtime. This feature is particularly important in industrial settings where continuous operation is essential.
Operational Benefits and Application Scenarios
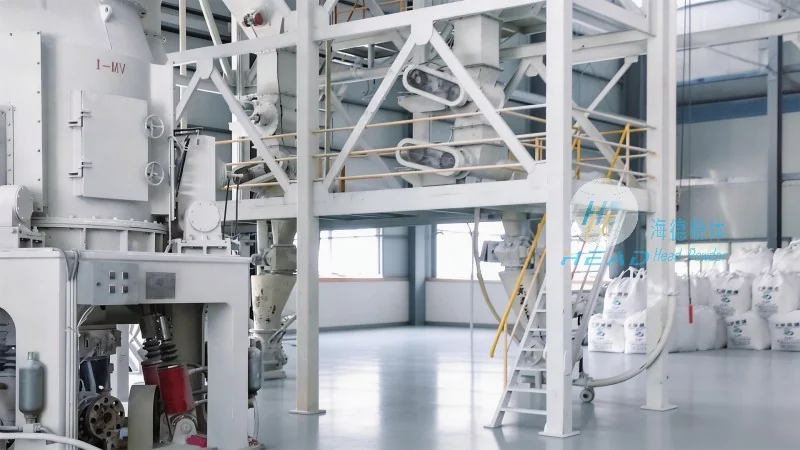
The effective material handling of ammonium bicarbonate offers several operational benefits. By optimizing the flow and storage of the chemical, companies can improve production efficiency, reduce waste, and enhance overall productivity. The systems also contribute to better workplace safety by minimizing exposure to dust and ensuring proper containment of the material.
These material handling solutions are widely used in industries such as food processing, pharmaceuticals, and chemical manufacturing, where ammonium bicarbonate is utilized as a leavening agent, a buffering agent, or a raw material in various formulations. The adaptability of the systems to different production scales and application requirements makes them a versatile choice for manufacturers.
Conclusion
In conclusion, the working principle and features of ammonium bicarbonate material handling systems are designed to address the unique challenges posed by this chemical. Through advanced technology and careful engineering, these systems ensure efficient, safe, and reliable handling of ammonium bicarbonate, supporting the smooth operation of industrial processes. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing tailored material handling solutions that meet the specific needs of clients, ensuring optimal performance and compliance with industry standards.