

Principles and Operational Scenarios of Small Bag Material Handling Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in providing advanced material handling solutions. The company's expertise lies in developing equipment that enhances efficiency and safety in various industrial processes.
Principles of Small Bag Material Handling Equipment
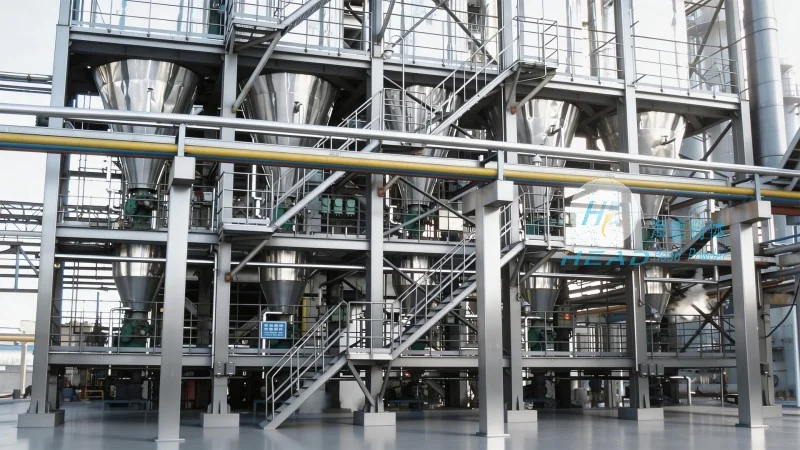
The small bag material handling equipment operates on a principle of automated material transfer. It typically consists of components such as feeders, conveyors, and control systems. The equipment is designed to handle bulk materials packaged in small bags, enabling seamless transfer from the source to the destination. The core mechanism involves the use of mechanical or pneumatic systems to lift, move, and discharge the bags. This ensures minimal human intervention while maintaining high throughput rates. The design incorporates features like adjustable speed control, which allows operators to optimize the handling process based on material characteristics and operational requirements. Furthermore, the equipment may include sensors and feedback systems to monitor the flow of materials, ensuring smooth operation and preventing blockages or overloading.
Operational Scenarios and Application Characteristics
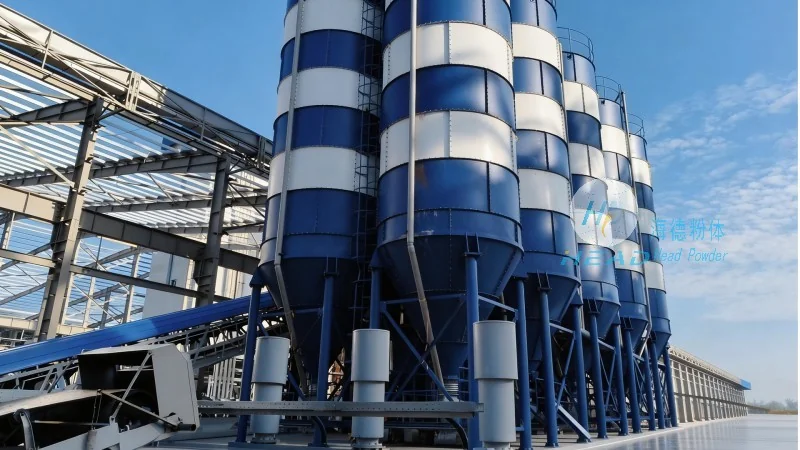
The operational scenarios of this equipment are diverse and tailored to various industrial applications. In pharmaceutical manufacturing, it is used to transport raw materials or finished products from storage to processing lines, ensuring compliance with hygiene and safety standards. The equipment's design, often made from stainless steel, meets the stringent requirements of the pharmaceutical industry, preventing contamination and maintaining product purity. In chemical plants, the equipment facilitates the movement of powdered chemicals, reducing the risk of dust exposure and improving workplace safety. The sealed system design minimizes the release of airborne particles, contributing to a safer working environment. Additionally, in food processing facilities, it helps in transferring ingredients while maintaining product integrity and preventing contamination. The equipment's hygienic design, with easy-to-clean surfaces, supports compliance with food safety regulations. Its compact and modular structure allows for integration into existing production lines without significant modifications, making it suitable for both new installations and retrofitting in existing facilities.
Key Features and Benefits
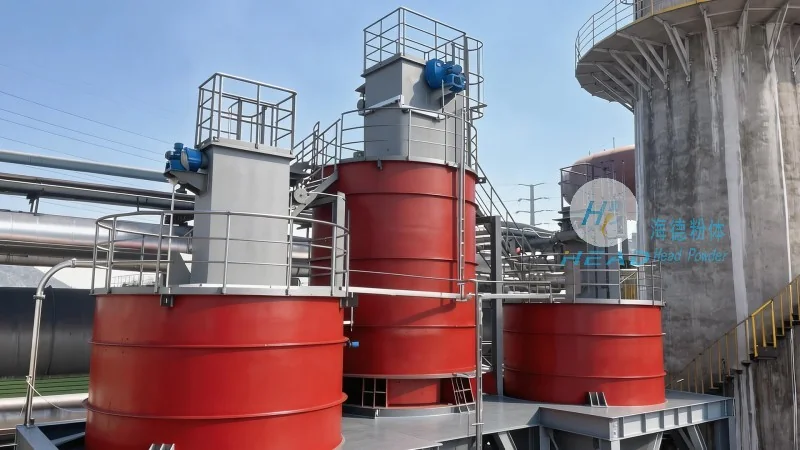
Small bag material handling equipment from HeadPowder offers several key features that enhance its performance and reliability. The equipment is equipped with durable components that can withstand harsh industrial environments, ensuring long-term operation with minimal maintenance. The adjustable speed control feature allows for flexibility in handling different types of materials, from fine powders to bulkier items. Additionally, the equipment's compact design saves space in production areas, making it ideal for facilities with limited floor space. The automated operation reduces labor costs and minimizes the risk of human error, leading to consistent and reliable material transfer. The company's commitment to quality ensures that each piece of equipment meets international standards, providing customers with a reliable solution for their material handling needs.