

Principles and Application Characteristics of Sugar Powder Pneumatic Conveying Lines
Pneumatic conveying systems, particularly those designed for sugar powder, operate on the fundamental principle of using air pressure to transport bulk materials through a pipeline. The core mechanism involves creating a pressure differential between the material source and the discharge point. By generating airflow—either through positive pressure (blowing air into the material) or negative pressure (suction from the material)—the system can move sugar powder efficiently. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational flexibility. The process typically starts with the sugar powder being fed into a hopper, where it is then drawn or pushed into the conveying line by the air flow. The air-sugar mixture travels through the pipeline, with the air providing the necessary force to overcome friction and gravity. At the destination, the air is separated from the powder, often via a cyclone separator or a filter, allowing the sugar to be deposited in the desired location. This principle is crucial for maintaining the quality of the sugar, as it prevents contamination and ensures a consistent flow.
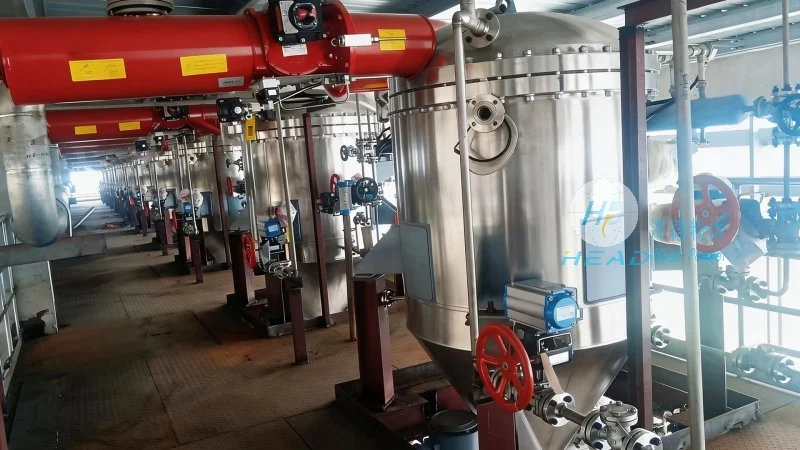
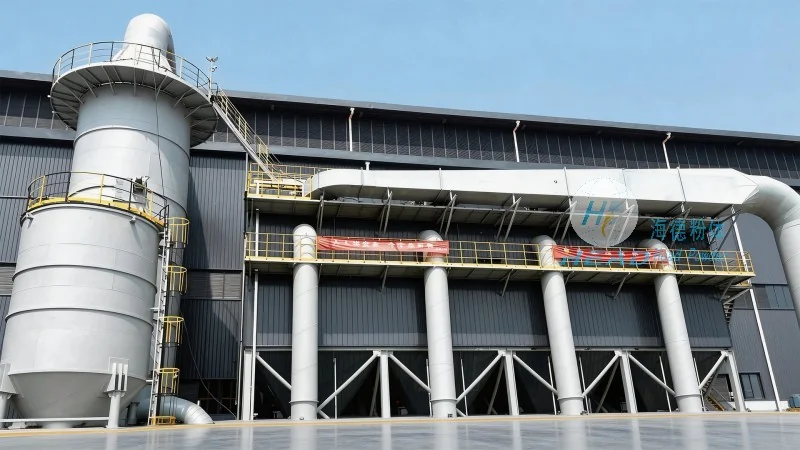
Application Characteristics in Sugar Processing Environments
The application characteristics of sugar powder pneumatic conveying lines are tailored to the specific demands of the sugar industry. These systems are commonly used in scenarios such as raw sugar handling, refined sugar processing, and bulk sugar storage. In raw sugar processing, the system efficiently transports sugar from storage silos to processing equipment, ensuring a continuous supply without the need for manual handling. For refined sugar, the pneumatic conveying line maintains the purity of the product by minimizing contact with external elements and preventing dust contamination. In storage facilities, the system can move large quantities of sugar between different storage areas, optimizing inventory management and reducing labor costs. The flexibility of these systems allows them to adapt to various production scales, from small-scale operations to large industrial plants. Additionally, the ability to handle different sugar grades (e.g., white sugar, brown sugar) without altering the system configuration makes them versatile for diverse processing needs. The operational efficiency of these lines is further enhanced by their ability to integrate with other processing equipment, such as crushers and classifiers, creating a seamless production flow.
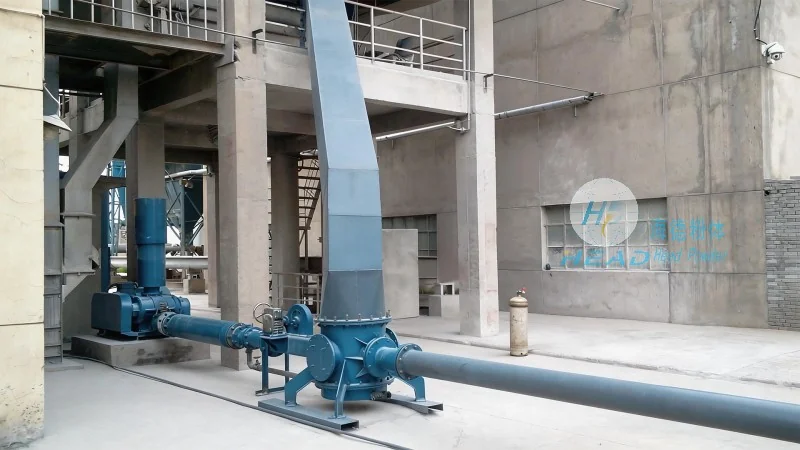
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling solutions, specializes in designing and supplying advanced pneumatic conveying systems for the sugar industry. With a strong presence in China, particularly in Shandong, the company has built a reputation for delivering high-quality, reliable equipment tailored to the unique requirements of sugar processing facilities. The company’s team of engineers and technicians brings extensive experience in powder technology, ensuring that each system is optimized for performance, efficiency, and durability. HeadPowder’s commitment to innovation is evident in its use of cutting-edge materials and design methodologies, which result in systems that meet international standards while addressing the specific challenges faced by sugar producers. The company’s customer-centric approach focuses on providing comprehensive solutions, including installation, maintenance, and technical support, to ensure long-term operational success. By leveraging its expertise in pneumatic conveying, HeadPowder helps sugar manufacturers improve productivity, reduce costs, and maintain product quality.
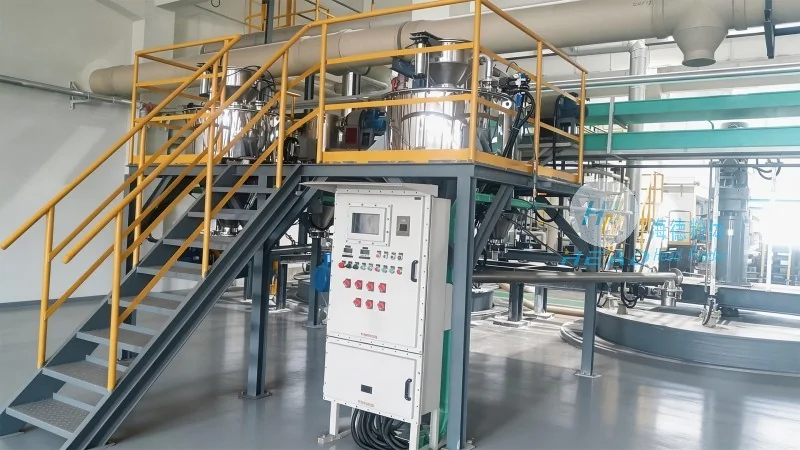
Key Features and Benefits of Sugar Powder Pneumatic Conveying Lines
The sugar powder pneumatic conveying lines offered by HeadPowder feature several key attributes that make them ideal for industrial applications. One of the primary benefits is the ability to handle fine powders without clogging or degradation, which is critical for maintaining the quality of sugar products. The systems are designed with smooth, corrosion-resistant pipelines and efficient air distribution to ensure consistent flow rates. This reduces the risk of material buildup and extends the lifespan of the equipment. Another significant advantage is the hygienic design, which is essential in food processing environments. The components are constructed from materials that meet food safety standards, such as stainless steel, and are easy to clean and sanitize. This helps prevent contamination and ensures compliance with regulatory requirements. The systems also offer energy efficiency, as they use less power compared to traditional mechanical conveying methods. By optimizing air pressure and flow rates, HeadPowder’s lines minimize energy consumption while maximizing throughput. Additionally, the modular design allows for easy expansion or modification, enabling manufacturers to adapt to changing production needs without significant investment. The reliability of these systems is further enhanced by advanced control systems that monitor pressure, flow, and temperature, providing real-time data and alerts for any issues. This proactive approach to maintenance helps prevent downtime and ensures continuous operation.