

Principle and Working Scene Characteristics of Bentonite Powder Pneumatic Conveyor
Bentonite powder pneumatic conveyors are specialized equipment designed for the efficient and reliable transport of bentonite powder, a widely used industrial material. This article provides an in-depth exploration of the working principle and key characteristics of such conveyors, along with typical application scenarios where they are commonly employed. The information is presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, based in China.
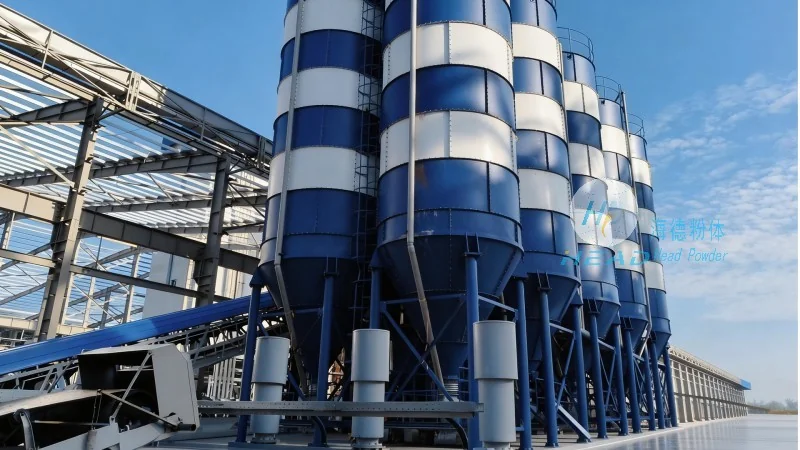
Introduction to Bentonite Powder Pneumatic Conveyor
Bentonite, a natural clay mineral, is known for its unique properties, including high swelling capacity and excellent thixotropy. These characteristics make bentonite an essential material in various industries, such as oil drilling, paper manufacturing, and foundry. The bentonite powder pneumatic conveyor is engineered to handle the challenges associated with transporting this fine, cohesive powder while maintaining product integrity and operational efficiency. HeadPowder, as a reputable company in the industry, specializes in developing and manufacturing such equipment to meet the diverse needs of clients worldwide.
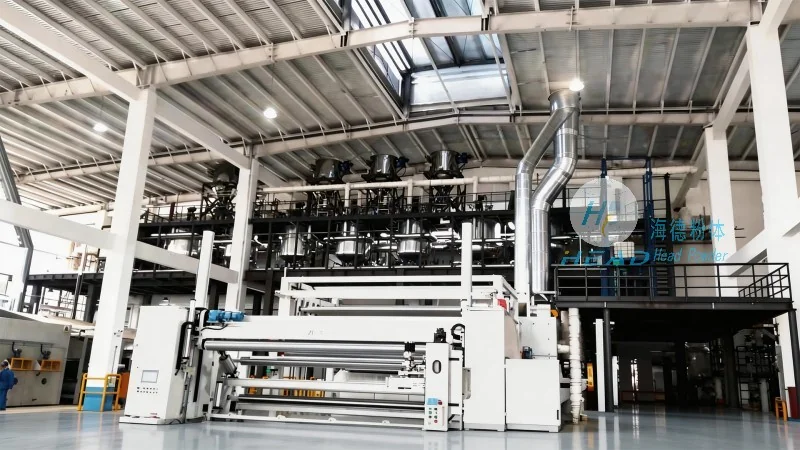
Working Principle of the Conveyor
The core of a bentonite powder pneumatic conveyor is the air-driven mechanism that propels the powder through a pipeline. The system typically operates by creating a pressure differential between the inlet and outlet of the conveyor. A high-efficiency fan or blower generates a high-velocity air stream, which is then mixed with the bentonite powder at the inlet. The air-powder mixture is then transported through the pipeline to the discharge point. The principle leverages the kinetic energy of the air to carry the powder particles, ensuring a continuous and controlled flow. The design of the conveyor, including the air inlet, mixing chamber, and pipeline configuration, is optimized to minimize particle degradation and maximize energy efficiency. The system can operate in both positive and negative pressure modes, depending on the specific requirements of the application. For example, in positive pressure systems, the air pressure is higher than the ambient pressure, pushing the powder through the pipeline. In negative pressure systems, the air pressure is lower than the ambient pressure, creating a vacuum that pulls the powder into the pipeline. The choice between the two modes depends on factors such as the distance of transport, the type of material, and the need for dust containment. The air flow rate and pressure are carefully controlled to ensure optimal performance, with sensors and control systems monitoring the process to maintain consistent operation.
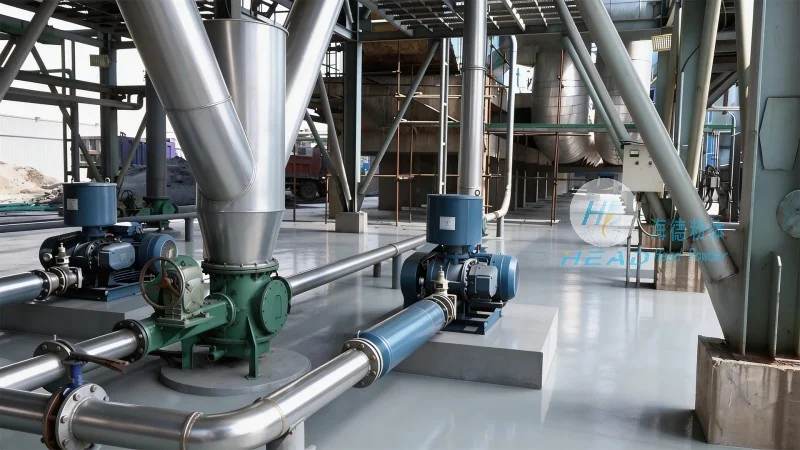
Key Features and Advantages
Bentonite powder pneumatic conveyors offer several advantages that make them a preferred choice for industrial applications. Firstly, they provide a dust-free and hygienic transport solution, which is crucial for maintaining product quality and compliance with environmental regulations. Unlike traditional mechanical conveyors, which can generate significant dust and cause contamination, pneumatic systems keep the material enclosed, reducing the risk of exposure to airborne particles. Secondly, these conveyors are highly efficient in terms of energy consumption and operational speed. The air-driven mechanism allows for rapid and continuous transport of large quantities of powder, reducing downtime and increasing overall productivity. Additionally, the flexibility of the system enables easy integration into existing production lines, with minimal modifications required. The equipment is also designed for easy maintenance, with accessible components that can be serviced quickly, minimizing operational interruptions. Another key advantage is the ability to handle a wide range of powder characteristics, including fine, cohesive, and abrasive materials, without causing blockages or wear to the system components. The system's adaptability also allows for adjustments to the air-powder ratio, ensuring optimal transport conditions for different powder types.
Typical Working Scenarios
Bentonite powder pneumatic conveyors are widely used in various industrial settings where the transport of fine powders is critical. One common application is in the oil and gas industry, where bentonite is used as a drilling fluid additive to improve mud properties. The conveyor system is used to transport bentonite from storage silos to the drilling site, ensuring a consistent supply of the material. In the paper manufacturing industry, bentonite is used as a filler and coating agent, and the pneumatic conveyor efficiently delivers it to the production line. The foundry industry also utilizes bentonite as a mold and core material, and the conveyor system facilitates the transfer of the powder from storage to the molding equipment. Additionally, in the chemical and pharmaceutical sectors, bentonite is used as a filter aid or adsorbent, and the conveyor ensures a clean and efficient supply of the material. The versatility of the system makes it suitable for a variety of applications, from small-scale laboratory use to large-scale industrial production. For instance, in a paper mill, the conveyor might transport bentonite from a storage hopper to a coating machine, where it is mixed with other chemicals to create a uniform coating on paper. In an oil drilling operation, the conveyor ensures that bentonite is delivered to the drilling rig in a controlled manner, maintaining the desired viscosity of the drilling fluid. The system's ability to handle both dry and slightly wet powders makes it suitable for a broad range of industrial processes.
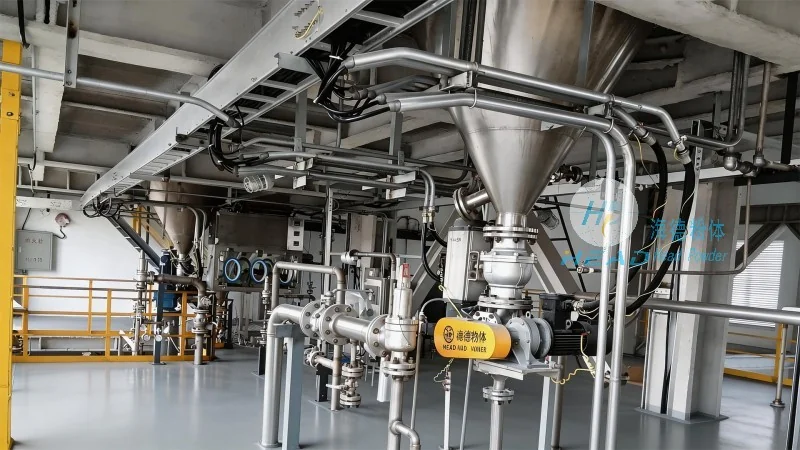
Company Information
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier of bentonite powder pneumatic conveyors and related industrial equipment. The company is headquartered in Shandong, China, and has established a strong reputation for quality, reliability, and customer satisfaction. HeadPowder specializes in customizing conveyor systems to meet the specific needs of clients, ensuring that the equipment is tailored to the unique requirements of each application. The company's products are designed with advanced technology and robust construction, ensuring long-term performance and minimal maintenance. With a commitment to innovation and customer service, HeadPowder continues to be a leading provider of pneumatic conveying solutions in the industry. The company's R&D team constantly works on improving the design and functionality of the conveyors, incorporating feedback from clients to enhance performance and durability. HeadPowder also provides comprehensive after-sales support, including installation, training, and maintenance services, to ensure that clients can fully utilize the equipment's capabilities. The company's focus on sustainability and environmental responsibility is reflected in the design of the conveyors, which minimize energy consumption and reduce emissions during operation.