

Operation Process and Working Principle of the Gray Bin Material Transport System
The Gray Bin Material Transport System, developed by Shandong HeadPowder Engineering Co., Ltd., is a sophisticated industrial solution designed for efficient material handling in various production environments. This system is particularly effective in applications where bulk materials need to be transported from storage bins to processing or packaging stations. The system integrates advanced engineering principles and robust components to ensure reliable and continuous operation, making it a critical asset for modern manufacturing operations. With a focus on durability and precision, the Gray Bin system is tailored to meet the demands of industries such as food processing, pharmaceuticals, and chemical manufacturing, where material integrity and safety are paramount.
Key Components and Their Functions
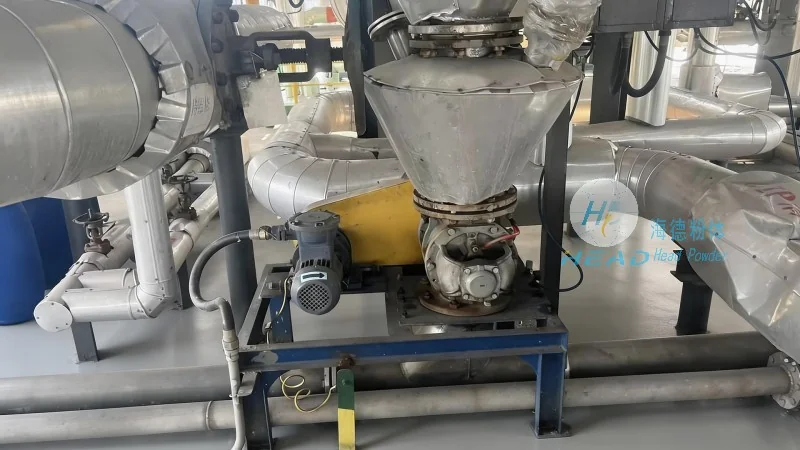
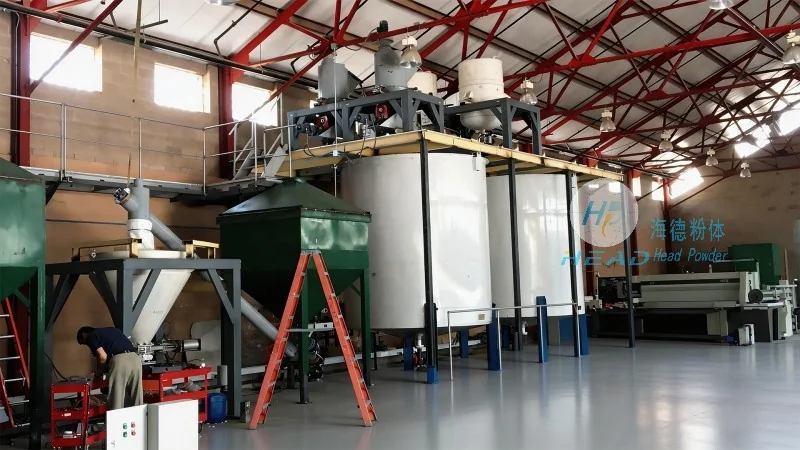
The Gray Bin Material Transport System comprises several essential components that work in harmony to facilitate smooth material flow. The primary components include the storage bin, conveyor mechanisms, control panels, and sensors. The storage bin, typically made of high-quality materials like stainless steel or reinforced plastic, is designed to hold bulk materials securely. It features a hinged or sliding lid for easy access and material loading. The conveyor system, which may consist of belt conveyors, screw conveyors, or pneumatic transport lines, is responsible for moving materials from the bin to the next stage of the production line. Control panels equipped with programmable logic controllers (PLCs) allow operators to monitor and adjust the system's performance in real-time. Sensors, including level detectors and position sensors, provide critical feedback to the control system, ensuring that the conveyor operates only when necessary and preventing overfilling or underfilling of the bin. Each component is engineered to withstand heavy usage and harsh environmental conditions, ensuring long-term reliability.
Operation Process Step-by-Step
The operation of the Gray Bin Material Transport System follows a systematic sequence that ensures efficient material handling. The process begins with the loading of materials into the storage bin. Operators typically use bulk loading equipment, such as a hopper or a bucket, to fill the bin to the desired level, as indicated by the level sensors. Once the bin is filled, the control system activates the conveyor mechanism. The conveyor then transports the material from the bin to the processing or packaging station. The speed of the conveyor can be adjusted based on the material type and production requirements, allowing for flexibility in operation. During the transport process, sensors continuously monitor the material level and position, providing feedback to the control system. If the bin becomes empty or the conveyor encounters an obstruction, the system automatically stops to prevent damage or material loss. After the material is fully transferred, the control panel signals the end of the cycle, and the system can be prepared for the next batch. This step-by-step operation ensures that the system operates safely and efficiently, minimizing downtime and maximizing productivity.
Working Principle Explained
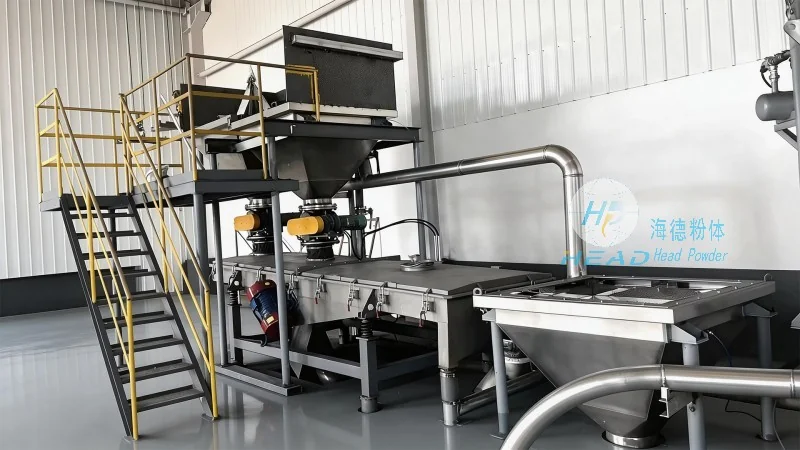
The working principle of the Gray Bin Material Transport System is based on the principles of mechanical and pneumatic engineering. The system operates by converting the potential energy stored in the bulk material within the bin into kinetic energy for transport. The conveyor mechanism, whether belt-driven or screw-driven, uses this energy to move the material forward. The control system, powered by PLCs, coordinates the operation of all components, ensuring that each step is executed in the correct sequence. Sensors play a crucial role in the working principle by providing real-time data to the control system. For example, level sensors detect when the bin is full or empty, triggering the start or stop of the conveyor. Position sensors monitor the movement of the material along the conveyor, ensuring that it reaches the correct destination. The system also incorporates safety features, such as emergency stop buttons and overload protection, to prevent accidents and equipment damage. By integrating these principles, the Gray Bin system achieves a high level of automation and efficiency, reducing the need for manual intervention and improving overall operational performance.
Benefits and Applications
The Gray Bin Material Transport System offers several benefits that make it an ideal choice for modern industrial applications. One of the primary benefits is its ability to handle large volumes of bulk materials with minimal human intervention. This reduces labor costs and improves safety in the workplace, as operators are less exposed to heavy lifting and material handling tasks. The system's robust design ensures long-term durability, even in harsh industrial environments, reducing maintenance costs and downtime. Additionally, the system's flexibility allows it to be adapted to various production requirements, making it suitable for a wide range of industries. The Gray Bin system is commonly used in food processing plants for transporting grains, powders, and other food ingredients. In pharmaceutical manufacturing, it is used to handle raw materials and finished products, ensuring compliance with stringent quality and safety standards. In chemical manufacturing, the system is employed to transport powders and granules, where material integrity and contamination control are critical. Overall, the Gray Bin Material Transport System enhances operational efficiency, improves product quality, and reduces operational costs, making it a valuable investment for any industrial facility.