

Design of a Pneumatic Conveying System for Coal Gangue Powder
Coal gangue, a byproduct of coal mining and processing, presents significant challenges in handling and utilization. The design of an efficient pneumatic conveying system is crucial for managing this material, ensuring safe, reliable, and cost-effective transportation. This article outlines the key aspects of a specialized system developed by Shandong HeadPowder Engineering Co., Ltd., focusing on the technical design, operational advantages, and practical applications.
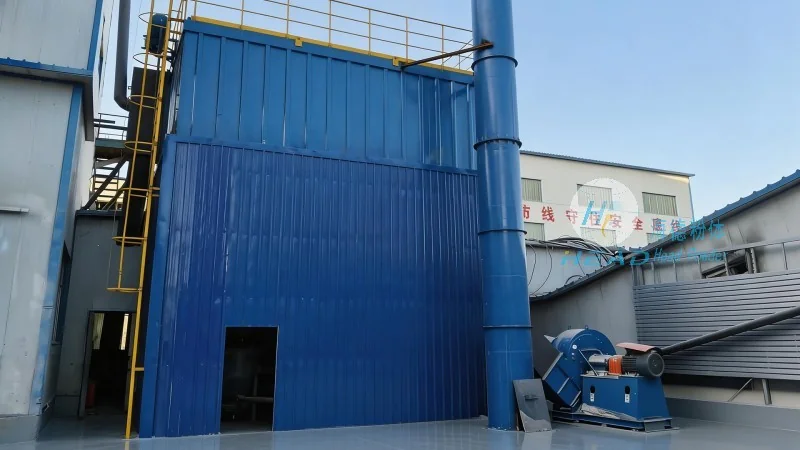
Overview of the Pneumatic Conveying System
The pneumatic conveying system for coal gangue powder is engineered to handle fine particulate materials, such as coal gangue, with high efficiency and minimal operational issues. The system integrates advanced components, including a high-pressure air compressor, a dust collection unit, and a flexible pipeline network, to facilitate the transport of gangue from storage areas to processing or disposal sites. By utilizing air as the conveying medium, the system eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and enhancing safety.
Technical Specifications and Design Considerations
The system is designed to accommodate varying particle sizes and moisture content typical of coal gangue. Key technical specifications include a maximum conveying capacity of up to 50 tons per hour, a pressure range of 0.5 to 1.0 MPa, and a pipeline diameter of 100 mm to 200 mm, depending on the application. The air compressor is equipped with a variable frequency drive (VFD) to adjust air flow and pressure dynamically, optimizing energy consumption and system performance. The dust collection unit incorporates a high-efficiency cyclone separator and a bag filter, ensuring compliance with environmental regulations and minimizing air pollution.
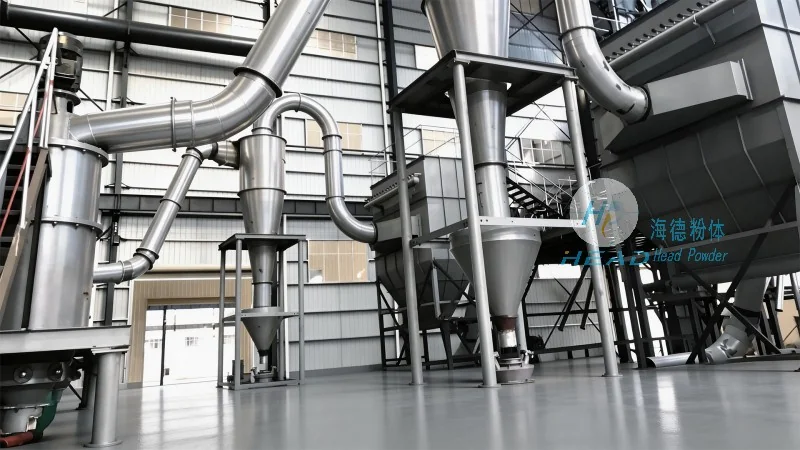
Operational Advantages and Benefits
Implementing this pneumatic conveying system offers several advantages over traditional methods. Firstly, it significantly reduces labor costs by automating the material handling process, eliminating the need for manual loading and unloading. Secondly, the system minimizes material degradation and loss, as the enclosed pipeline prevents contamination and spillage. Additionally, the compact design of the system allows for easy integration into existing industrial facilities, with minimal space requirements. The energy efficiency of the VFD-controlled compressor further reduces operational costs over time.
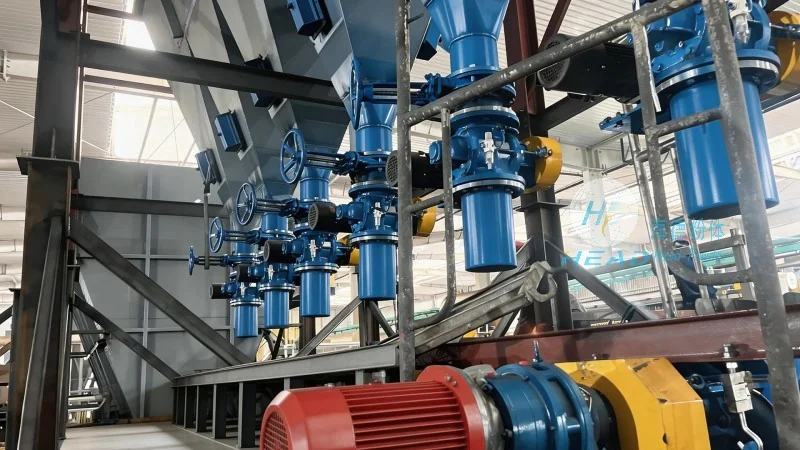
Application Scenarios and Industry Impact
The pneumatic conveying system is particularly suitable for coal processing plants, power generation facilities, and waste management sites where coal gangue needs to be transported over short to medium distances. In these applications, the system enhances operational efficiency by streamlining the material flow, improving production throughput, and reducing downtime. By effectively managing coal gangue, the system contributes to sustainable resource utilization and environmental protection, aligning with industry standards for responsible waste management.
Company Information and Background
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design and manufacturing of advanced material handling systems. With a focus on innovation and customer-centric solutions, the company has developed a range of products tailored to the unique needs of the coal and mining industries. HeadPowder's expertise in pneumatic conveying technology ensures that clients receive reliable, high-performance systems that meet both operational and regulatory requirements. The company is headquartered in Shandong, China, and serves clients globally with customized solutions and technical support.