

What is a Gelatin Material Handling Conveyor? And What Are Its Design Principles?
Understanding the gelatin material handling conveyor and its design principles is crucial for industries that rely on efficient processing of gelatin products. This equipment is engineered to streamline the movement of gelatin materials through various stages of production, ensuring optimal performance and reliability.
Overview of Gelatin Material Handling Conveyors
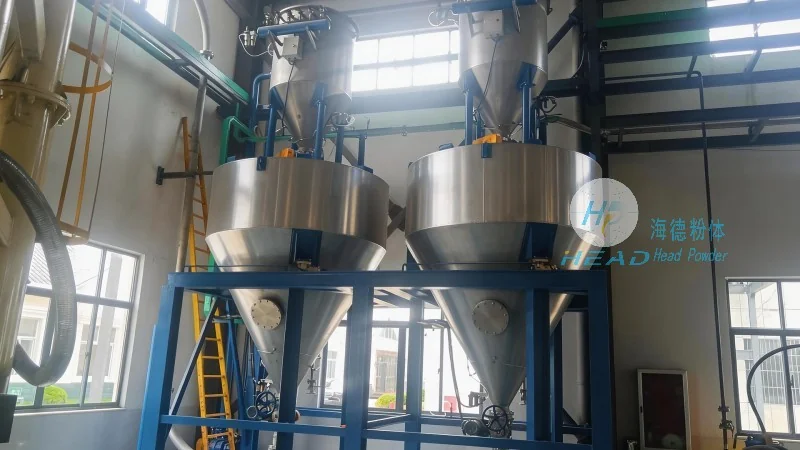
Gelatin material handling conveyors are specialized systems designed to transport gelatin materials from one processing stage to another. These conveyors are integral to the production workflow in industries such as food manufacturing, pharmaceuticals, and cosmetics, where gelatin is used as a key ingredient. The primary function of these conveyors is to facilitate the smooth and controlled movement of gelatin, minimizing downtime and enhancing overall operational efficiency.
Key Design Principles of Gelatin Material Handling Conveyors
The design of gelatin material handling conveyors adheres to several critical principles to ensure they meet the specific demands of gelatin processing. These principles include durability, hygiene, and adaptability to the unique properties of gelatin. Each component of the conveyor system is carefully selected to withstand the physical and chemical characteristics of gelatin, ensuring long-term performance and minimal maintenance.
Structural Components and Their Functions
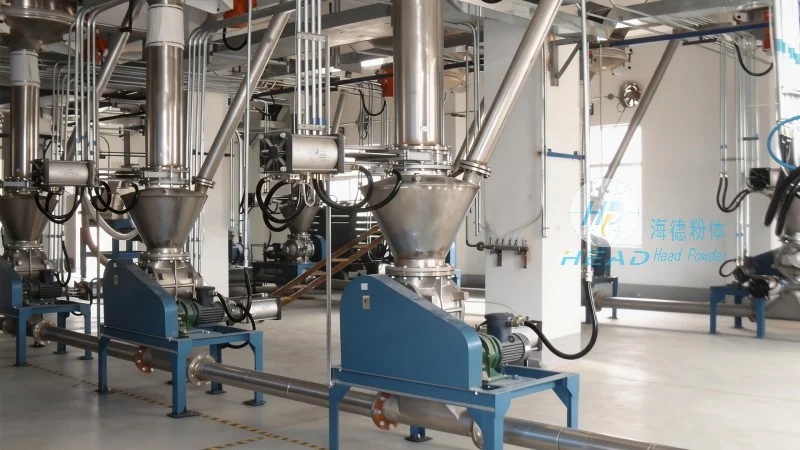
Gelatin material handling conveyors typically consist of several key structural components, each playing a vital role in the overall operation. The main components include the conveyor belt or chain, drive mechanisms, support frames, and control systems. The conveyor belt or chain is designed to handle the weight and texture of gelatin without causing degradation or contamination. Drive mechanisms, often powered by electric motors, provide the necessary force to move the gelatin along the conveyor path. Support frames ensure stability and proper alignment, while control systems allow for precise regulation of speed and direction.
Hygienic Design Considerations
Due to the food and pharmaceutical applications of gelatin, hygiene is a paramount consideration in the design of material handling conveyors. The systems are constructed from materials that are easy to clean and sanitize, such as stainless steel. Smooth surfaces and minimal crevices are incorporated to prevent the accumulation of gelatin residue, which could lead to contamination or bacterial growth. Additionally, the design allows for easy disassembly and cleaning, ensuring compliance with regulatory standards.
Adaptability and Customization
Modern gelatin material handling conveyors are designed to be adaptable to various production needs. Manufacturers often offer customizable options to accommodate different gelatin types, production volumes, and facility layouts. This flexibility allows companies to optimize their conveyor systems for specific operational requirements, enhancing efficiency and reducing costs. Customization may include variations in conveyor length, width, speed, and the inclusion of additional features such as sorting or packaging integration.
Operational Efficiency and Maintenance
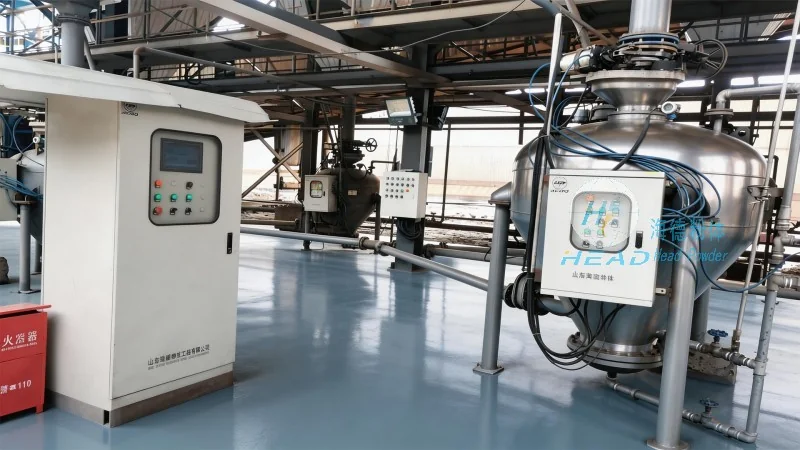
The design principles of gelatin material handling conveyors prioritize operational efficiency and ease of maintenance. The use of robust materials and well-engineered components minimizes the risk of breakdowns and extends the lifespan of the equipment. Regular maintenance, including lubrication of moving parts and inspection of conveyor belts, is essential to maintain optimal performance. Additionally, the control systems often include monitoring features that alert operators to potential issues, allowing for timely intervention and preventing costly downtime.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of material handling solutions, specializes in designing and producing gelatin material handling conveyors tailored to the needs of various industries. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner for companies seeking reliable and efficient conveyor systems. The company's products are engineered to meet the highest standards of performance, hygiene, and durability, ensuring that clients receive equipment that enhances their production processes and meets regulatory requirements.