

Working Principle and Features of Vacuum Suction Type Pneumatic Conveying Systems
HeadPowder, a leading provider of industrial solutions, specializes in advanced pneumatic conveying systems. Among these, the vacuum suction type system stands out for its efficiency and versatility in material handling. This article delves into the working principle and key features of this technology, highlighting how it addresses the needs of modern industrial operations.
Understanding the Working Principle of Vacuum Suction Type Pneumatic Conveying Systems
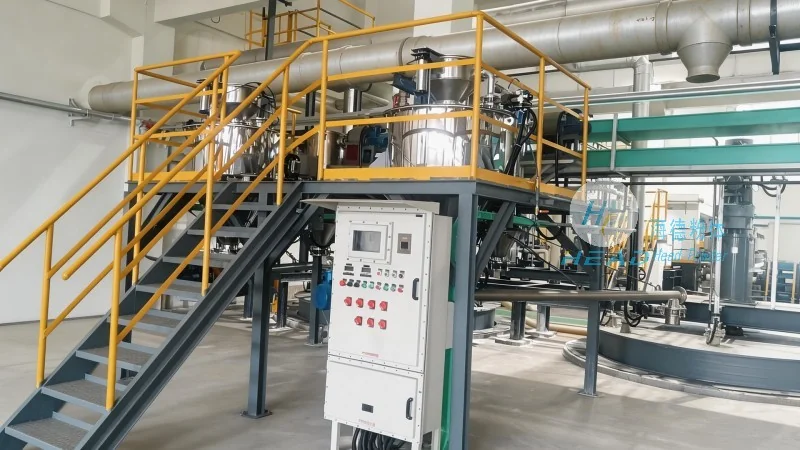
The vacuum suction type pneumatic conveying system operates on the principle of creating a negative pressure environment at the inlet to draw materials into the system. This method is particularly effective for transporting dry bulk materials over moderate distances, often from a storage silo or hopper to a processing unit. The process begins with the activation of the vacuum pump, which reduces the pressure inside the conveying line. As the pressure drops below atmospheric levels, the material inside the source container is drawn into the line due to the pressure differential. The material is then carried by a stream of air, which is typically introduced at the discharge end to maintain flow and prevent clogging. The system uses a combination of suction and air pressure to move materials without the need for mechanical components like augers or belts, making it ideal for handling delicate or abrasive powders.
Key Features and Advantages of Vacuum Suction Type Systems
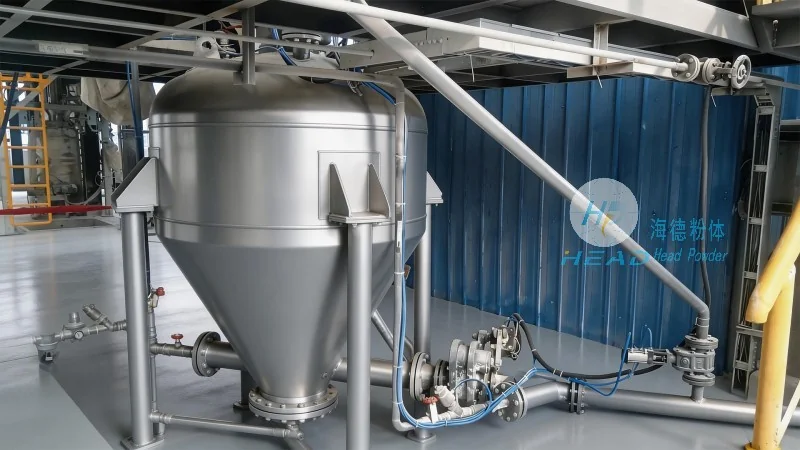
One of the primary advantages of vacuum suction type pneumatic conveying systems is their ability to handle a wide range of materials, including fine powders, granules, and even small particles. The gentle handling reduces product degradation and maintains the integrity of the material, which is crucial for sensitive products like pharmaceuticals or food ingredients. Additionally, these systems are highly efficient in terms of energy consumption, as they operate with lower air velocities compared to positive pressure systems, resulting in reduced operational costs. The design also allows for easy integration with existing facilities, as the suction inlet can be positioned close to the material source, minimizing the need for extensive modifications to the plant layout. Another notable feature is the system's adaptability to varying material flow rates and distances, making it suitable for both small-scale and large-scale industrial applications. The modular construction of the system enables easy maintenance and component replacement, ensuring long-term reliability and minimal downtime.
Application Scenarios and Industrial Benefits
Vacuum suction type pneumatic conveying systems are widely used in various industries, including food processing, pharmaceutical manufacturing, chemical processing, and mining. In the food industry, for example, these systems are employed to transport ingredients like flour, sugar, and spices from storage to production lines, ensuring hygienic and efficient handling. In pharmaceutical applications, the system's ability to maintain product purity and prevent contamination is critical, as it operates in a closed-loop environment with minimal human intervention. The chemical industry benefits from the system's resistance to corrosive materials and its ability to handle hazardous powders safely. The mining sector utilizes vacuum suction systems for transporting ore and tailings, reducing the risk of dust exposure and improving operational safety. Overall, the industrial benefits of these systems include increased productivity, reduced labor costs, and enhanced safety in material handling operations.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted manufacturer and supplier of vacuum suction type pneumatic conveying systems. With years of experience in the industry, the company has developed advanced solutions that meet the diverse needs of global clients. The systems are designed with precision engineering, ensuring high performance, reliability, and compliance with international standards. HeadPowder's commitment to quality and customer satisfaction has made it a preferred choice for businesses seeking efficient and sustainable material handling solutions. By leveraging the principles of vacuum suction technology, the company continues to innovate and provide tailored solutions that enhance operational efficiency and reduce costs for its clients.