

Principle and Working Scene Characteristics of Rare Earth Powder Pneumatic Conveying Systems
Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced pneumatic conveying solutions for rare earth powder applications. Our systems are designed to efficiently handle the unique challenges associated with transporting fine, abrasive, and valuable rare earth materials. This article explores the fundamental principles behind our pneumatic conveying systems and highlights the specific working scene characteristics that make them ideal for various industrial applications.
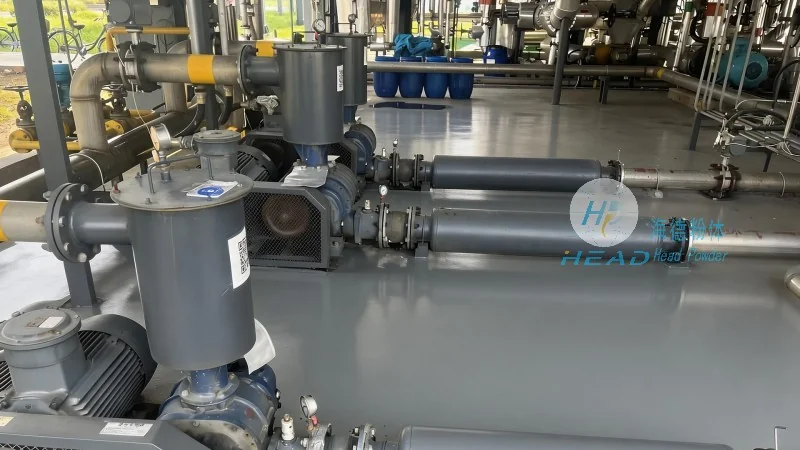
Introduction to Rare Earth Powder Pneumatic Conveying Systems
Pneumatic conveying systems utilize air or other gases to transport bulk materials, such as rare earth powders, through a pipeline network. Unlike traditional mechanical conveying methods, these systems offer a flexible, low-maintenance, and cost-effective solution for moving materials over short to medium distances. The technology is particularly well-suited for handling materials that are difficult to transport by conventional means, including those with high moisture content, low bulk density, or abrasive properties.
The Working Principle of Pneumatic Conveying Systems
At the core of our pneumatic conveying systems is the principle of fluidization and suspension. The system operates by creating a high-velocity air stream within the pipeline, which lifts and transports the rare earth powder particles. This is achieved through a combination of positive pressure (pressure conveying) or negative pressure (vacuum conveying) systems. In pressure conveying, compressed air is introduced at the material inlet, while in vacuum conveying, a vacuum is created at the discharge end to draw the material through the pipeline. The design of the system, including the type of air nozzles, pipeline diameter, and material feed mechanisms, is critical to ensuring efficient and stable material transport.
Key Features and Advantages for Rare Earth Powder Handling
Our pneumatic conveying systems are engineered with several key features that enhance performance and reliability for rare earth powder applications. These include:
1. Low Material Abrasion: The smooth, corrosion-resistant pipeline materials and optimized air flow reduce wear and tear on both the equipment and the material itself, extending the system's operational life.
2. Minimal Product Contamination: The sealed pipeline design prevents cross-contamination and exposure to external elements, ensuring that the rare earth powder remains pure and free from impurities.
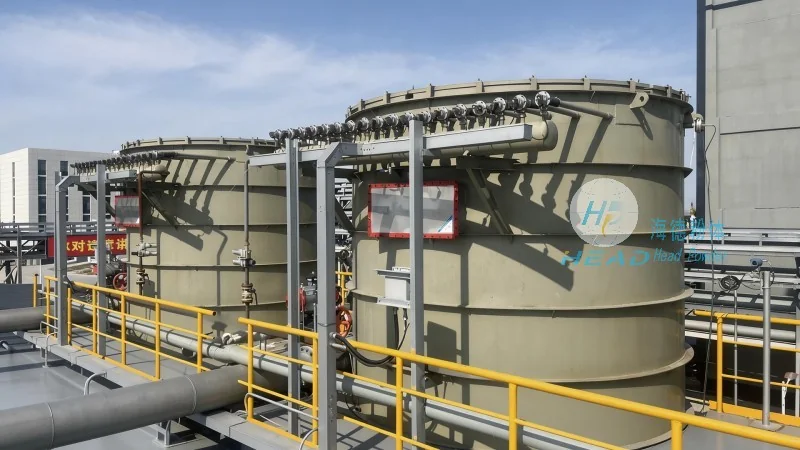
3. Energy Efficiency: Advanced control systems and optimized air pressure settings minimize energy consumption while maintaining consistent material flow rates.
4. Flexibility in Layout: The modular design allows for easy integration into existing production lines and can be adapted to various plant layouts, including horizontal, vertical, or combined configurations.
Application Scenarios and Industry Use Cases
The working scene characteristics of our pneumatic conveying systems make them suitable for a wide range of industrial applications involving rare earth powders. Some common use cases include:
1. Material Transfer Between Production Stages: In rare earth processing facilities, our systems efficiently transport raw rare earth powders from crushing and grinding units to subsequent processing steps, such as magnetic separation or chemical treatment.
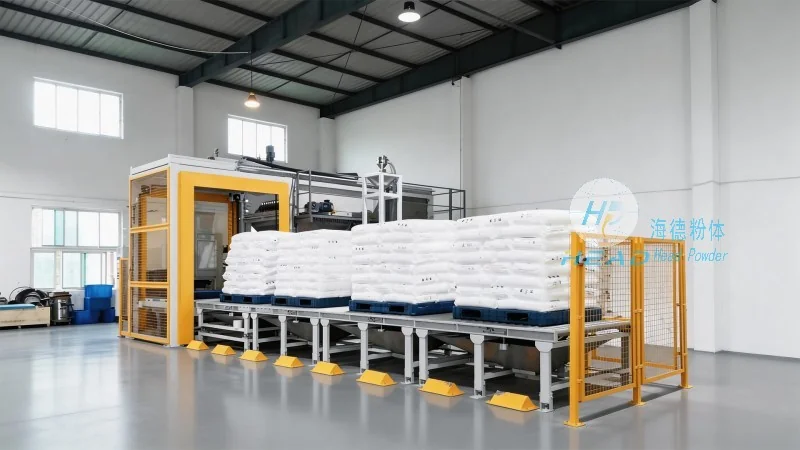
2. Storage and Distribution: The systems can be integrated with bulk storage silos to transfer materials from storage to processing equipment or for distribution to other parts of the facility.
3. Quality Control and Sampling: The sealed and controlled environment of the pneumatic system allows for precise sampling and quality control of the rare earth powder, ensuring product consistency and meeting regulatory standards.
4. Environmental Compliance: By containing the material within a closed system, our pneumatic conveying solutions help minimize dust emissions and comply with environmental regulations, making them an environmentally friendly choice for rare earth powder handling.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China, and specializes in the design, manufacturing, and installation of customized pneumatic conveying systems for various industrial applications. With years of experience in the field, our company has developed a deep understanding of the unique challenges associated with handling rare earth powders and has tailored our solutions to meet the specific needs of our clients. Our team of engineers and technicians works closely with customers to provide tailored system designs that optimize performance, reduce costs, and enhance operational efficiency.
At HeadPowder, we are committed to delivering high-quality, reliable, and efficient pneumatic conveying solutions that meet the demanding requirements of the rare earth industry. Our systems are built to last, with robust construction and advanced control technologies that ensure consistent performance and minimal downtime. Whether you are a new or existing user of rare earth powder handling systems, our team is ready to assist you in finding the perfect solution for your specific application needs.