

Principle and Working Scene Characteristics of Pneumatic Powder Conveyors
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic powder conveying systems. These systems are engineered to efficiently transport dry powders and granular materials in various industrial applications. The following article delves into the fundamental principles behind these systems and highlights key working scene characteristics that make them indispensable in modern manufacturing processes.
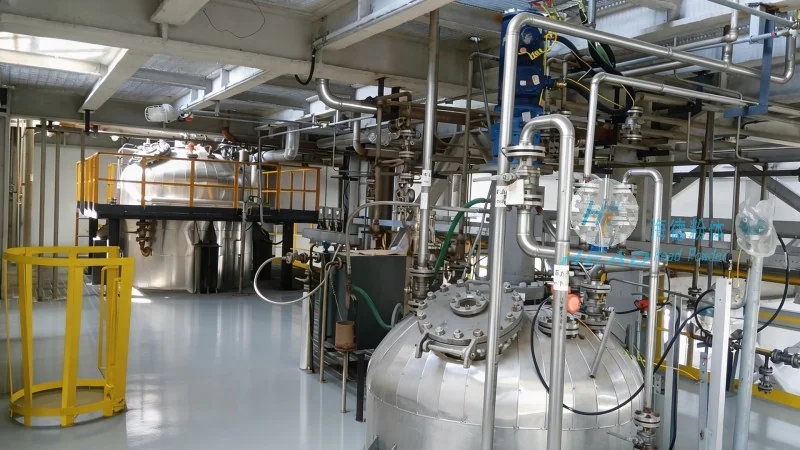
Understanding the Core Principle of Pneumatic Powder Conveyors
Pneumatic powder conveyors operate on the principle of using compressed air or other gases to move materials through a pipeline. The system typically consists of a hopper, a blower, a filter, and a discharge unit. As dry powder is fed into the hopper, the blower generates a high-pressure airflow that draws the material into the pipeline. The airflow carries the particles through the system, ensuring consistent and controlled transport. This method eliminates the need for mechanical components like belts or chains, reducing maintenance and enhancing safety. The efficiency of the system depends on factors such as the type of material, particle size, and the pressure of the air supply. By optimizing these parameters, manufacturers can achieve reliable and continuous material handling, minimizing downtime and operational costs.
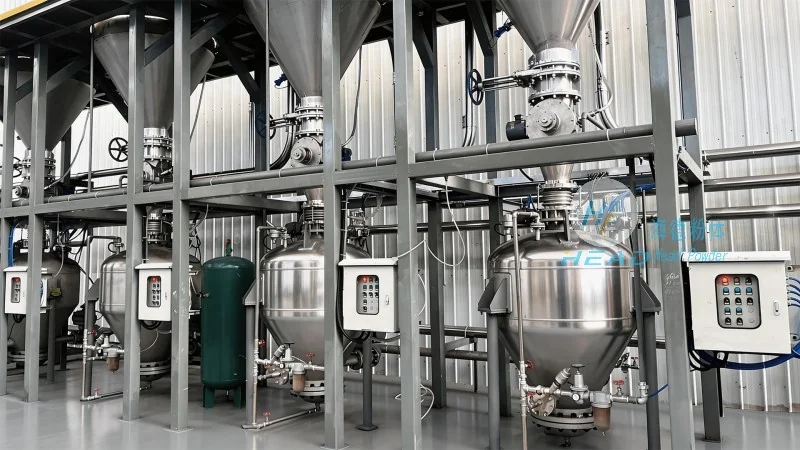
Key Working Scene Characteristics of Pneumatic Powder Conveying Systems
The application of pneumatic powder conveyors varies widely across different industries, each with unique requirements. In pharmaceutical manufacturing, for instance, these systems are used to transport sensitive powders with strict contamination control measures. The enclosed design and filtration systems ensure that the materials remain clean and free from particulate matter, meeting regulatory standards. In the food industry, similar considerations apply, where hygiene and product purity are paramount. The systems are often constructed from stainless steel and equipped with easy-to-clean components, facilitating compliance with food safety regulations. In chemical processing, the ability to handle abrasive or corrosive materials is crucial. Pneumatic conveyors are designed to withstand such conditions, with materials like stainless steel or special alloys used for the pipeline and components. This adaptability makes them suitable for a broad range of chemical applications, from bulk material handling to precise dosing.
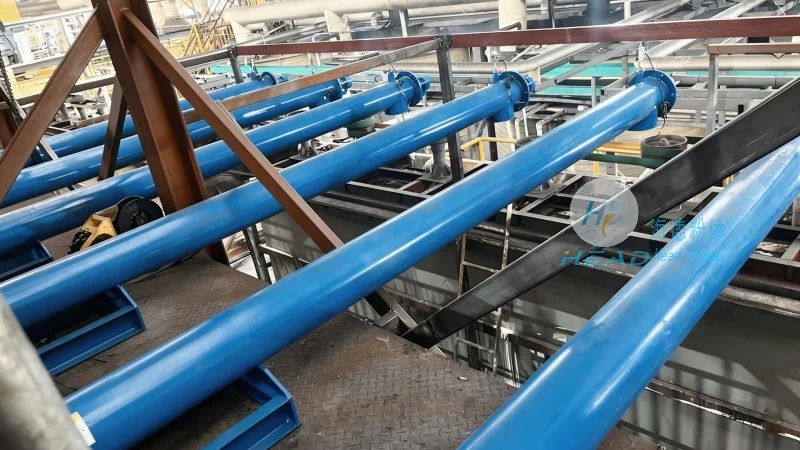
Advantages and Practical Applications in Industrial Settings
One of the primary advantages of pneumatic powder conveyors is their flexibility in handling different material types and particle sizes. Unlike mechanical systems, they can transport materials with varying densities and flow characteristics without requiring adjustments. This makes them ideal for applications where the material composition changes frequently, such as in blending or mixing operations. The system's ability to operate in a closed loop also reduces dust emissions, improving workplace safety and environmental compliance. In addition, the compact design of these conveyors allows for easy integration into existing production lines, minimizing the need for extensive modifications. This is particularly beneficial for manufacturers looking to upgrade their facilities without disrupting ongoing operations. The reliability of pneumatic systems, coupled with low maintenance requirements, results in significant cost savings over time. By eliminating the need for manual handling and reducing material loss, these systems enhance overall productivity and operational efficiency.
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable company dedicated to providing high-quality pneumatic powder conveying solutions. With years of experience in the industry, the company has developed a comprehensive range of products tailored to meet diverse customer needs. The team of engineers and technicians at HeadPowder is committed to innovation, continuously improving the design and performance of their systems to deliver superior results. The company's focus on customer satisfaction and technical support ensures that clients receive not only reliable equipment but also expert guidance throughout the entire process. Whether for new installations or system upgrades, HeadPowder stands as a trusted partner in optimizing material handling processes across various industries.