

Principle and Working Scene Characteristics of Powder Material Transport Systems Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder material transport systems. These systems are engineered to efficiently handle bulk powders such as grains, flour, and other fine particulate materials, ensuring reliable and consistent performance in various industrial applications. The core of these systems lies in their ability to transport materials from one location to another while maintaining product integrity and operational efficiency.
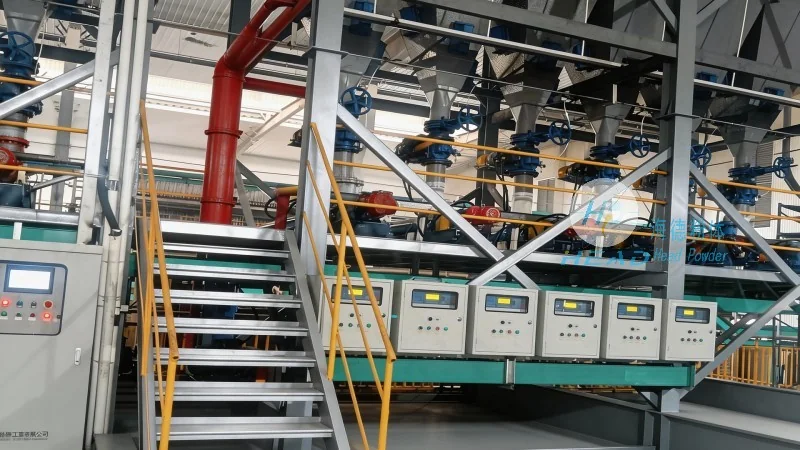
Principle of Operation for Powder Transport Systems
The fundamental principle behind powder material transport systems is the conversion of mechanical energy into the force required to move bulk materials. Common technologies include pneumatic conveying (air-assisted systems), screw conveyors, and bucket elevators. Pneumatic systems utilize compressed air to create a flow of material through a pipeline, while screw conveyors rely on rotating screws to push material forward. For applications involving high-volume or abrasive materials, bucket elevators provide a robust solution by lifting material vertically and transporting it horizontally. Each system is tailored to the specific characteristics of the powder—such as particle size, moisture content, and flowability—to optimize performance and minimize downtime.
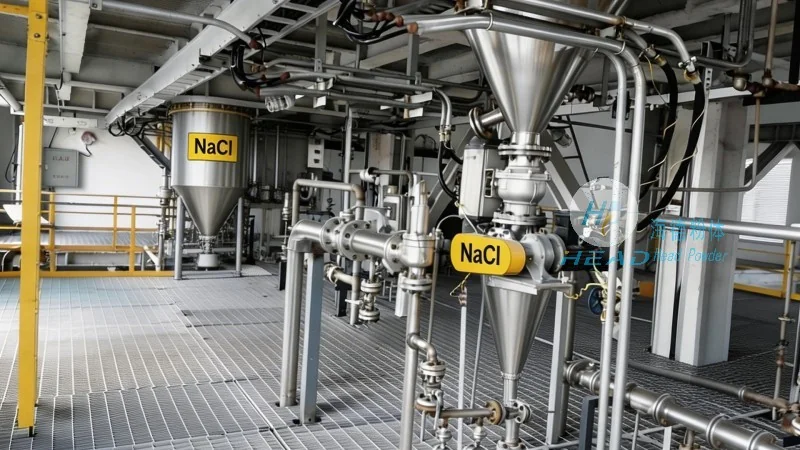
Working Scene Characteristics and Applications
Powder material transport systems are widely used across multiple industries, each with distinct operational requirements. In the food processing sector, systems must adhere to strict hygiene standards and ensure no contamination of the product. For example, in flour mills, pneumatic conveyors are employed to transport raw flour from storage silos to processing lines, maintaining a clean and controlled environment. In the chemical industry, systems are designed to handle corrosive or reactive powders, with materials like stainless steel or special coatings used for the conveyor components to prevent material degradation and equipment damage.
Key Features and Advantages
Modern powder transport systems from HeadPowder offer several advantages that enhance operational efficiency and product quality. These include: 1) **High Efficiency and Low Maintenance**: Advanced designs reduce energy consumption and minimize wear on components, leading to lower operational costs over time. 2) **Customization**: Systems can be tailored to specific material properties and process requirements, ensuring optimal performance for each application. 3) **Safety and Reliability**: Incorporating safety features such as overload protection and material flow monitoring ensures smooth operation and prevents accidents. 4) **Space Efficiency**: Compact designs allow for installation in limited spaces, making them suitable for both new and existing facilities.
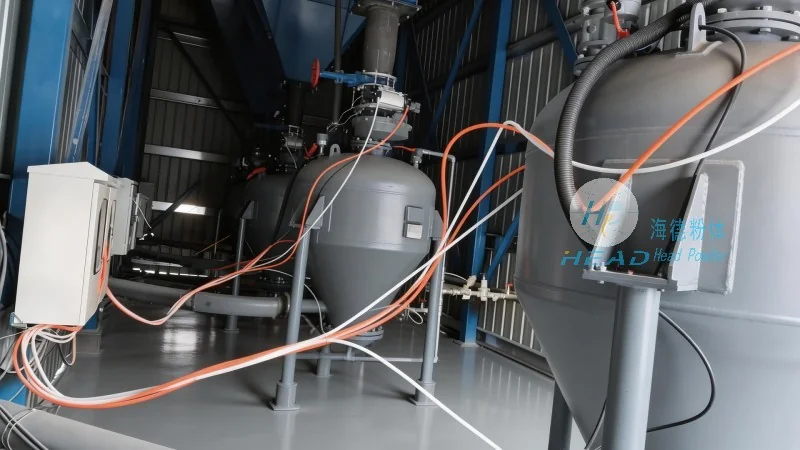
Conclusion
HeadPowder Engineering Co., Ltd. continues to innovate in the field of powder material transport systems, providing solutions that meet the evolving needs of industries worldwide. By combining advanced technology with a deep understanding of material handling, their systems deliver reliable performance, enhanced productivity, and improved product quality. With a strong presence in Shandong, China, HeadPowder remains committed to delivering high-quality equipment that meets the highest standards of industrial application.