

Principle and Working Scene Characteristics of Rare Earth Crystal Powder Material Handling Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material handling equipment tailored for the transportation of rare earth crystal powders. This article delves into the fundamental principles behind such equipment and highlights the key characteristics of its operational environments.
Introduction to Rare Earth Crystal Powder Material Handling Equipment
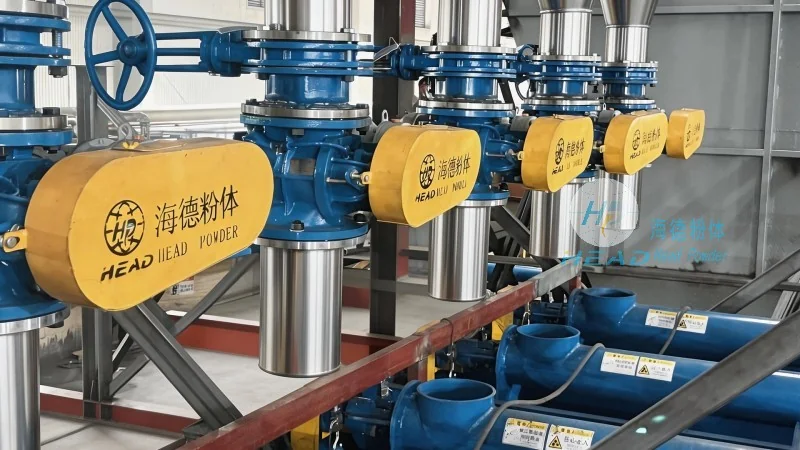
At the core of modern industrial processes, the efficient and safe transportation of rare earth crystal powders is critical for maintaining productivity and ensuring product quality. HeadPowder Engineering Co., Ltd. has developed specialized equipment that addresses the unique challenges posed by these materials, including their fine particle size, hygroscopic nature, and potential for dust generation. The equipment is engineered to handle these characteristics while optimizing material flow and minimizing operational risks.
Principle of Operation for Material Handling Equipment
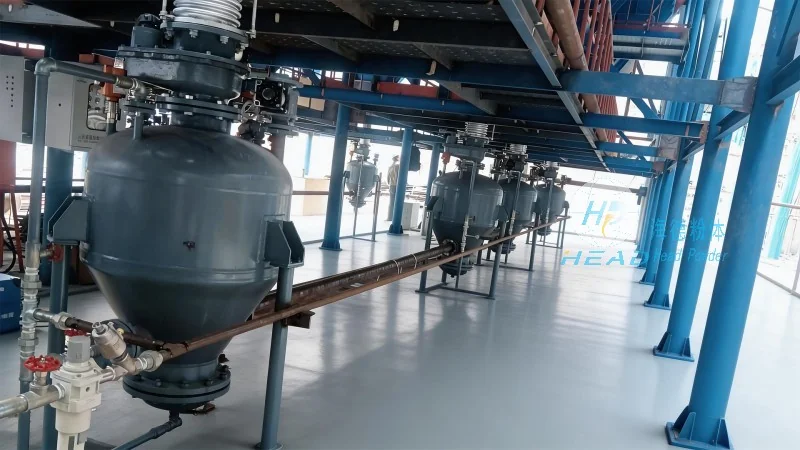
The primary principle of rare earth crystal powder material handling equipment revolves around the use of controlled air flow and specialized containment systems. These systems are designed to prevent material loss, cross-contamination, and exposure to environmental factors that could degrade the powder's properties. The equipment typically incorporates features such as sealed hoppers, flexible hoses, and vacuum or pressure-based conveying mechanisms. For example, vacuum conveyors are commonly used to transport powders from storage silos to processing lines, ensuring a gentle and continuous flow that preserves the material's integrity. The design also includes filtration and dust collection systems to maintain air quality and comply with safety regulations.
Key Working Scene Characteristics
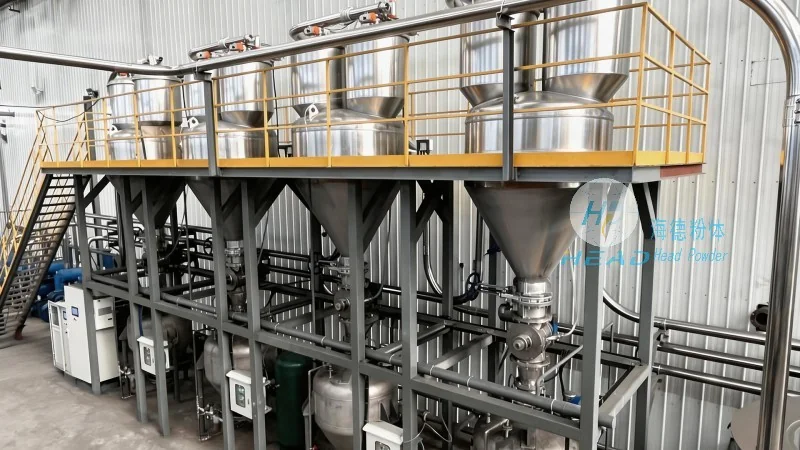
The operational environments where this equipment is deployed vary significantly based on the specific application and production scale. In large-scale manufacturing facilities, the equipment is integrated into automated production lines, requiring high throughput and reliability. The working scenes often involve multiple stages of material handling, from initial storage and feeding to final discharge and packaging. For instance, in rare earth element processing plants, the equipment may be used to transfer powders between grinding, classification, and sintering processes. The characteristics of these working scenes include high material volumes, continuous operation, and the need for precise control over flow rates and pressure. In smaller or laboratory-scale settings, the equipment may be more compact and portable, designed for batch processing and research applications. These environments demand flexibility and ease of maintenance, with features like quick-disconnect fittings and adjustable conveying speeds.
Technical Advantages and Applications
HeadPowder's material handling equipment offers several technical advantages that make it suitable for diverse industrial applications. The equipment is constructed from materials resistant to corrosion and wear, such as stainless steel and special alloys, which are essential for handling chemically active rare earth powders. The sealed design minimizes the risk of material contamination and environmental pollution, aligning with stringent environmental regulations. Additionally, the equipment is equipped with sensors and control systems that monitor parameters like pressure, flow rate, and temperature, providing real-time feedback and enabling automated adjustments. These features enhance operational efficiency and reduce downtime. The applications of this equipment span various industries, including electronics, automotive, and renewable energy, where rare earth elements are integral components. In the electronics industry, for example, the equipment is used to transport powders for the production of magnets and catalysts, while in the automotive sector, it supports the manufacturing of high-performance alloys.
Conclusion and Company Overview
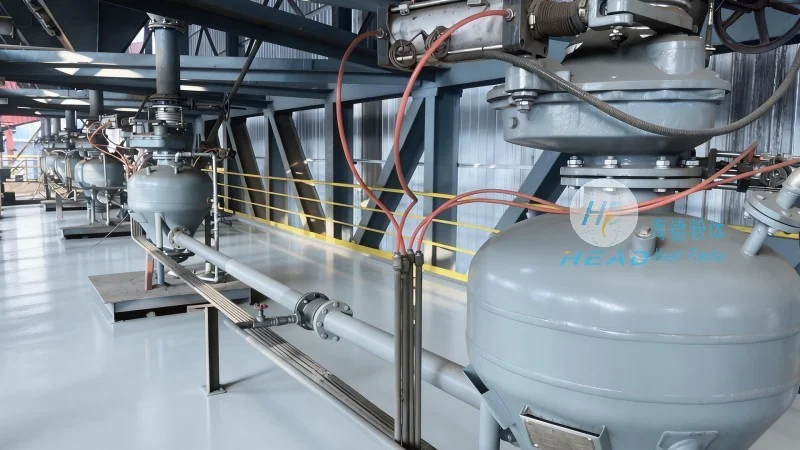
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides advanced material handling solutions for the transportation of rare earth crystal powders. The company's equipment is designed based on robust principles of controlled air flow and specialized containment, ensuring the safe and efficient handling of these critical materials. The working scene characteristics, ranging from large-scale industrial production to smaller research applications, are addressed through flexible and reliable equipment designs. With a focus on technical excellence and compliance with industry standards, HeadPowder continues to serve as a trusted partner in the rare earth processing industry, delivering equipment that meets the evolving needs of modern manufacturing.