

Principles and Application Scenarios of Glucose Powder Material Handling Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced material handling solutions tailored for industries dealing with bulk powders like glucose. This article explores the fundamental principles behind glucose powder material handling equipment and highlights key application scenarios where such systems excel in performance and efficiency.
Understanding the Core Principles of Glucose Powder Handling Systems
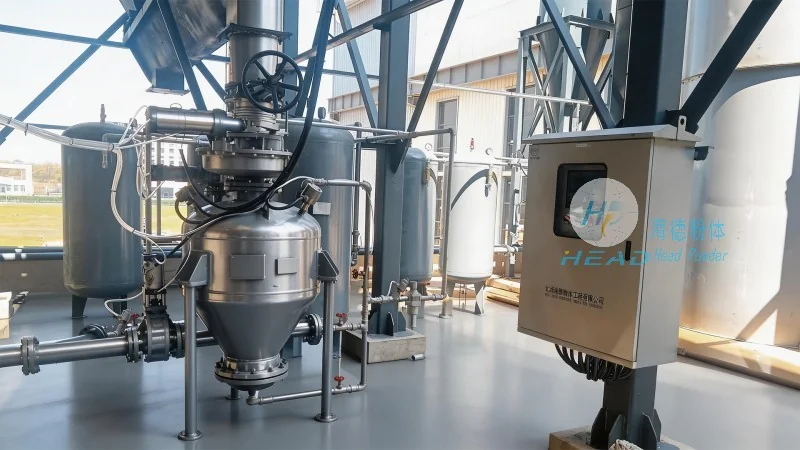
Glucose powder, a critical raw material in various industries including pharmaceuticals, food processing, and chemical manufacturing, requires specialized equipment to ensure safe, efficient, and hygienic handling. The primary principles of glucose powder material handling systems revolve around controlling particle flow, minimizing dust generation, and maintaining product integrity throughout the process. Key components typically include hopper designs, conveyor mechanisms, and dust control systems, all engineered to address the unique properties of glucose powder—such as its fine particle size, hygroscopic nature, and potential for caking.
One of the foundational principles is the use of aeration and vibration to prevent clogging in storage and transfer processes. Glucose powder is prone to agglomeration, which can disrupt flow and lead to equipment downtime. Advanced systems incorporate air knives, rotary valves, and vibratory feeders to maintain consistent material movement. Additionally, the design of hoppers and chutes is critical to minimize product degradation and ensure uniform discharge. By optimizing these elements, manufacturers can achieve reliable operation and reduce the risk of product contamination.
Key Application Scenarios for Glucose Powder Handling Equipment
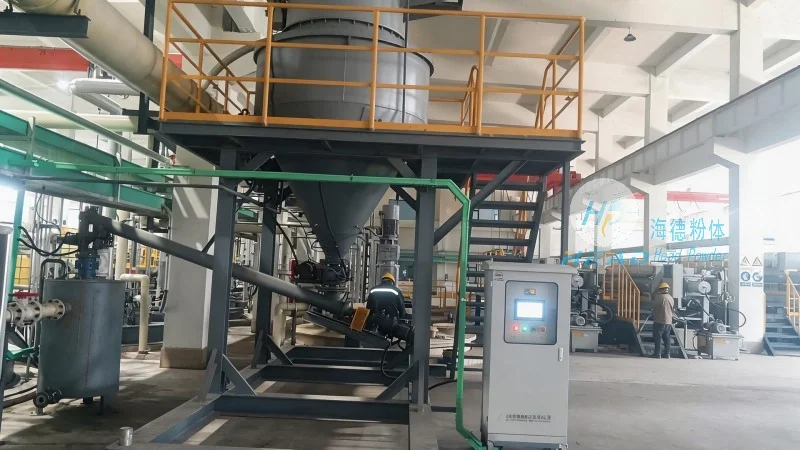
The versatility of glucose powder handling equipment makes it indispensable across multiple industrial sectors. In the pharmaceutical industry, for instance, precise control over powder flow is essential to meet stringent quality standards and regulatory requirements. Systems designed for this sector often feature stainless steel construction, HEPA filtration, and closed-loop transfer to prevent cross-contamination. These features ensure that glucose powders used in drug formulations remain pure and free from contaminants, which is critical for patient safety.
In the food processing industry, glucose powder handling equipment is used in the production of beverages, confectionery, and nutritional supplements. Here, the focus is on maintaining product freshness and preventing moisture absorption. Equipment may include enclosed conveyors and moisture-resistant components to preserve the quality of the powder. The ability to handle large volumes efficiently while maintaining hygiene standards is a key advantage in food manufacturing, where product safety and regulatory compliance are paramount.
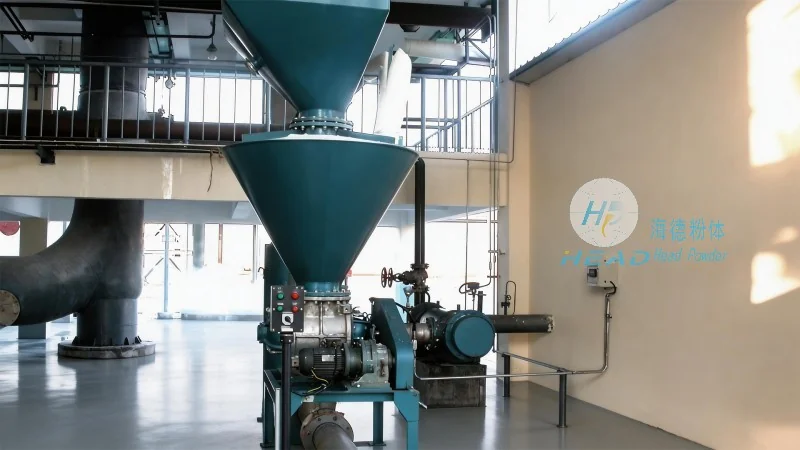
Chemical manufacturing also relies on specialized glucose powder handling systems, particularly in the production of sweeteners and industrial chemicals. These applications often require high-capacity transfer and integration with other processing equipment. The robust design of the systems, including heavy-duty motors and durable materials, ensures they can withstand the demands of continuous operation in chemical plants. Moreover, the ability to handle varying particle sizes and flow rates makes the equipment adaptable to different production needs.
Advantages of HeadPowder's Glucose Powder Handling Solutions
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, offers comprehensive solutions that address the specific challenges of glucose powder handling. The company’s expertise lies in customizing equipment to meet the unique needs of each client, whether it’s for small-scale production or large industrial applications. Their systems are designed to enhance operational efficiency, reduce downtime, and improve overall product quality.
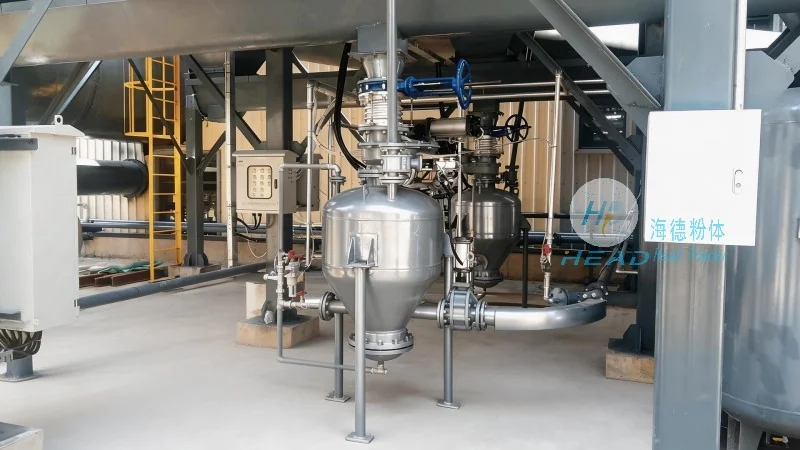
Key advantages of HeadPowder’s solutions include advanced control systems that allow real-time monitoring of material flow and system performance. This enables operators to quickly identify and address any issues, minimizing disruptions in production. Additionally, the company’s commitment to using high-quality materials and adhering to international standards ensures that their equipment meets the highest safety and hygiene requirements. By leveraging their experience and innovation, HeadPowder provides reliable and cost-effective solutions for glucose powder handling across various industries.
From pharmaceuticals to food processing and chemical manufacturing, the demand for efficient and reliable glucose powder handling equipment continues to grow. HeadPowder’s dedication to engineering excellence and customer satisfaction positions them as a trusted partner for businesses seeking to optimize their material handling processes. By understanding the core principles and application scenarios of glucose powder handling systems, companies can make informed decisions to enhance productivity and maintain product quality in their operations.