

Operation Process and Working Principle of Purified Powder Material Conveying System
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder material handling technology, specializes in the design, manufacturing, and installation of advanced conveying systems for various industrial applications. With a focus on precision, efficiency, and reliability, the company has established itself as a trusted partner for businesses requiring high-quality solutions for transporting fine powders and granular materials. HeadPowder's systems are engineered to meet stringent industry standards, ensuring optimal performance and minimal contamination in diverse operational environments.
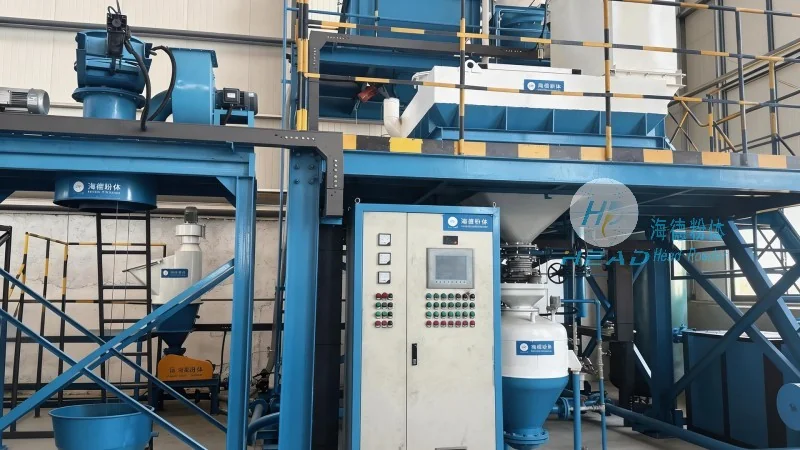
Purified Powder Material Conveying System Overview
The purified powder material conveying system is a sophisticated piece of industrial equipment designed to handle the transportation of fine powders and granular substances with precision and efficiency. This system is particularly suitable for industries such as pharmaceuticals, food processing, chemical manufacturing, and mining, where maintaining product purity and preventing contamination is critical. The system integrates advanced components and control mechanisms to ensure that materials are conveyed safely and effectively, adhering to regulatory requirements and operational standards.
Key Components and Functional Modules
The conveying system comprises several key components, each playing a vital role in the overall operation. These include feed hoppers, which are used to introduce the powder material into the system; conveying pipes or ducts, which transport the material from the source to the destination; and control valves and actuators, which regulate the flow and pressure within the system. Additionally, the system may incorporate dust collection and filtration units to maintain air quality and prevent dust emissions. The integration of these components ensures a seamless and controlled flow of material, minimizing the risk of blockages and ensuring consistent performance.
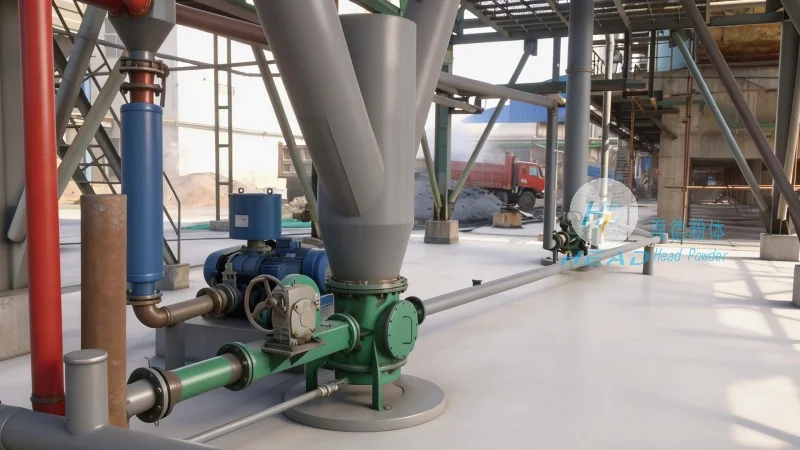
Operation Process of the Conveying System
The operation of the purified powder material conveying system follows a systematic process that begins with the loading of the material into the feed hopper. Once the hopper is filled, the system's control system activates the feeding mechanism, which gradually releases the powder into the conveying pipe. The material is then propelled through the pipe by a combination of air pressure (in pneumatic systems) or mechanical force (in mechanical systems). The conveying process continues until the material reaches the discharge point, where it is collected in a receiving container or transferred to the next processing stage. Throughout the operation, the system's sensors and monitoring devices track key parameters such as flow rate, pressure, and temperature, providing real-time feedback to the control system for adjustments as needed.
Working Principle of the Conveying System
The working principle of the purified powder material conveying system is based on the principles of fluid dynamics and mechanical engineering. In pneumatic conveying systems, the material is suspended in a stream of air and transported through the pipeline. The air pressure is carefully controlled to maintain the material in a suspended state, preventing it from settling or clogging the pipe. In mechanical conveying systems, such as screw conveyors or belt conveyors, the material is moved by rotating components that push or pull the material along the conveying path. The selection of the appropriate conveying method depends on factors such as the material's properties, the required conveying distance, and the operational environment. The system's design ensures that the material is handled gently, preserving its quality and preventing degradation.
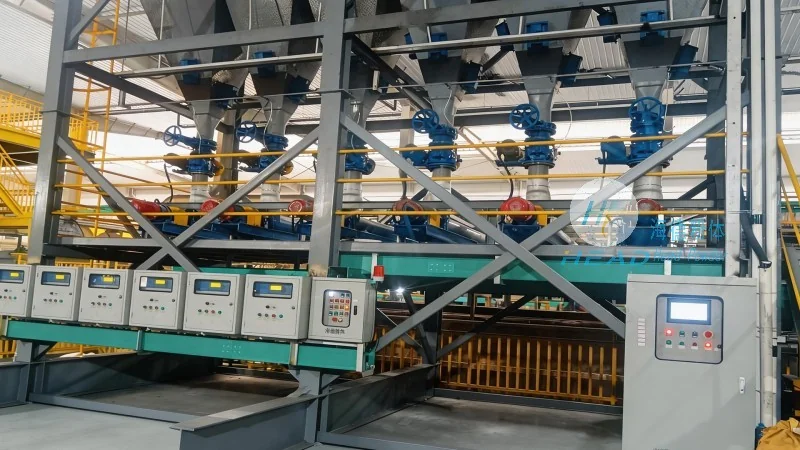
Advantages and Applications
HeadPowder's purified powder material conveying systems offer several advantages that make them ideal for a wide range of industrial applications. These include high efficiency in material transportation, minimal product loss and contamination, and low maintenance requirements. The systems are also designed to be flexible and adaptable, allowing for easy integration with existing production lines and modifications to accommodate changing operational needs. The applications of these systems span various industries, including pharmaceutical manufacturing, where the system ensures the safe and sterile transport of active ingredients; food processing, where it maintains the purity of food products; and chemical manufacturing, where it handles hazardous materials with precision and safety.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced and reliable purified powder material conveying systems that are engineered to meet the demanding requirements of modern industrial operations. By combining innovative technology with rigorous quality control, the company ensures that its systems deliver optimal performance, efficiency, and safety. The operation process and working principle of these systems are designed to provide consistent and reliable material handling, supporting the productivity and success of businesses across various sectors. With a commitment to excellence and customer satisfaction, HeadPowder continues to be a leader in the development and application of cutting-edge powder material conveying solutions.