

Crystal Particle Pneumatic Conveying: A Solution for Material Transport Beyond Distance Limits
HeadPowder, the professional brand of Shandong HeadPowder Engineering Co., Ltd., is dedicated to providing advanced material handling solutions. Based in Shandong, China, the company specializes in the design, manufacturing, and implementation of efficient pneumatic conveying systems, particularly for the transport of crystal particles. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industrial material transport sector.
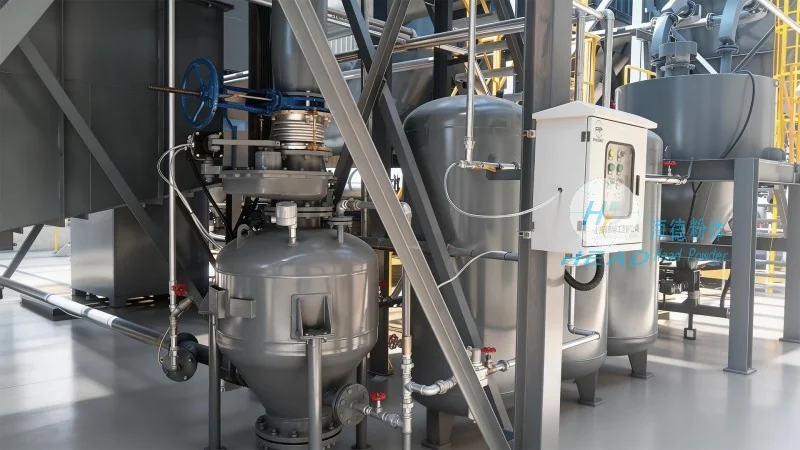
Crystal Particle Pneumatic Conveying Systems
Our crystal particle pneumatic conveying solutions are engineered to handle a wide range of crystalline materials, including pharmaceutical powders, chemical crystals, and food-grade particles. The systems utilize air as the primary transport medium, enabling the seamless movement of these delicate and often sensitive materials over long distances without the need for mechanical components like belts or chains. This approach not only minimizes product contamination but also reduces maintenance requirements, making it an ideal choice for industries where product purity and operational efficiency are paramount.
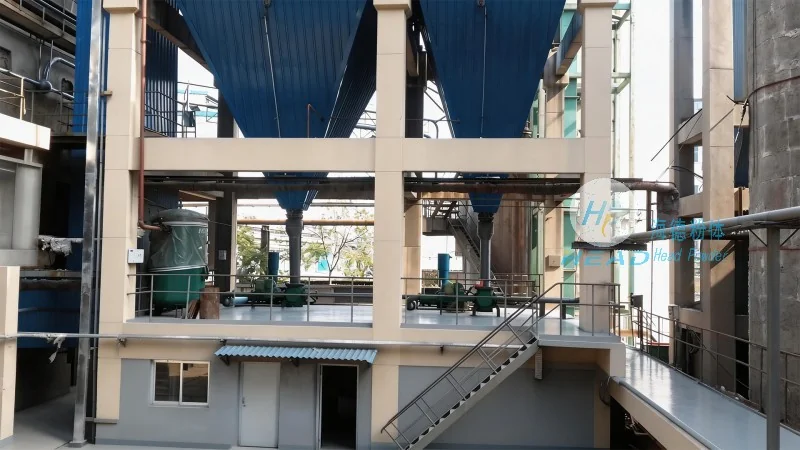
Overcoming Distance Limitations in Material Transport
Traditional material handling methods often face constraints when transporting crystal particles over extended distances. HeadPowder's pneumatic conveying systems address this challenge by leveraging high-pressure air to propel particles through pipelines. By optimizing the air velocity and pipeline design, our solutions can effectively transport materials over distances of several kilometers, far exceeding the capabilities of conventional systems. This capability is crucial for industries that require centralized material storage and distribution, as it allows for the efficient movement of raw materials from storage facilities to production lines without compromising on speed or product integrity.
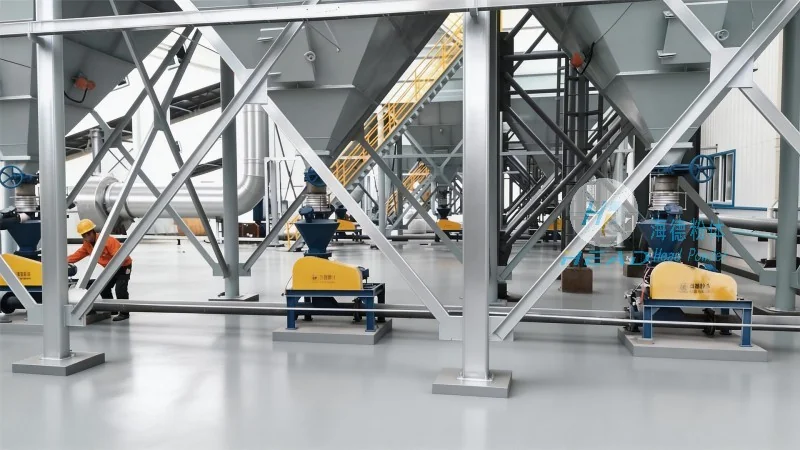
Technical Advantages of Pneumatic Conveying for Crystalline Particles
The pneumatic conveying technology employed by HeadPowder offers several key advantages for crystal particle transport. Firstly, it provides a dust-free and hygienic environment, which is essential for pharmaceutical and food applications where contamination control is critical. Secondly, the system's ability to handle fine and abrasive particles without causing wear and tear on equipment ensures long-term reliability and low maintenance costs. Additionally, the flexible pipeline layout allows for easy integration into existing industrial setups, minimizing downtime during installation and operation. These technical benefits collectively contribute to a more sustainable and cost-effective material handling process.
Applications in Industrial Processes
HeadPowder's crystal particle pneumatic conveying systems are widely used across various industrial sectors. In the pharmaceutical industry, they are employed to transport active pharmaceutical ingredients (APIs) and excipients with precision, ensuring that the final product meets stringent quality standards. In the chemical industry, the systems handle various chemical crystals, facilitating the smooth flow of raw materials between reactors and storage tanks. Similarly, in the food and beverage sector, the technology is used to convey food-grade crystalline products, maintaining the product's quality and safety throughout the transport process. Each application leverages the unique characteristics of the material, such as particle size, density, and moisture content, to optimize the conveying performance.
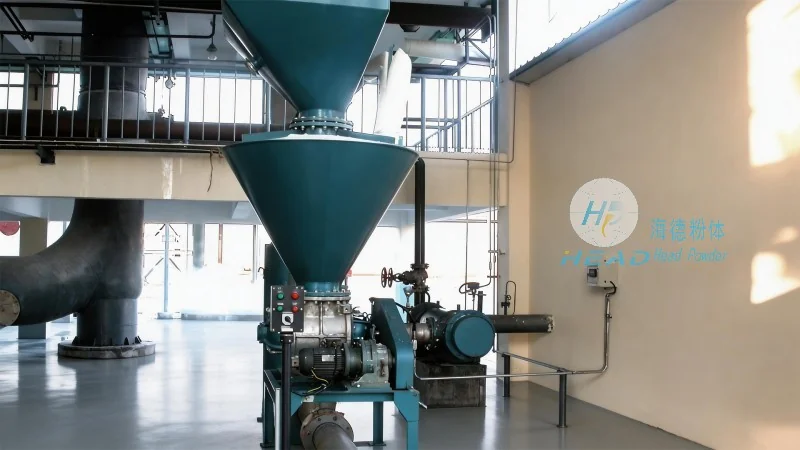
Quality and Reliability in Material Handling
At HeadPowder, quality is at the core of our operations. All our pneumatic conveying systems are manufactured with high-quality materials and undergo rigorous testing to ensure compliance with industry standards. The company adheres to strict quality control measures, from the design phase to the final product delivery, to guarantee that each system performs as intended. This commitment to quality ensures that customers receive reliable and durable equipment that can withstand the demands of continuous industrial use. Furthermore, HeadPowder provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure that the systems operate at peak efficiency throughout their service life.