

What is a Fertilizer Powder Pneumatic Conveying System? And What Are Its Design Principles?
A fertilizer powder pneumatic conveying system is a specialized industrial equipment designed to transport bulk powder materials, such as fertilizers, through a pipeline using air or gas as the conveying medium. This technology offers an efficient, dust-free, and flexible method for moving powders over long distances, making it a critical solution in the agricultural and chemical industries. The system combines various components that work together to ensure reliable and continuous material handling, addressing the unique challenges of handling fine, dry, or even slightly sticky powder materials commonly found in fertilizer production and distribution.
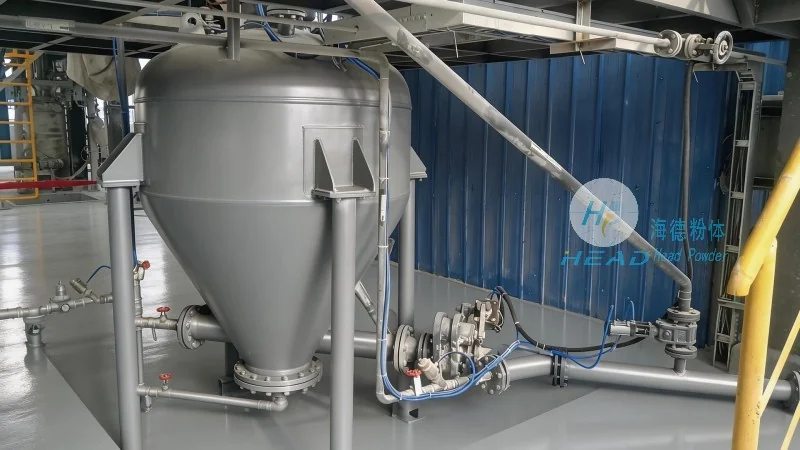
Key Components and Their Functions
The core components of a typical fertilizer powder pneumatic conveying system include the material feeder, conveying pipeline, air source (blower or compressor), separation and collection unit, and control system. The material feeder, often a rotary valve or a star feeder, ensures a consistent and controlled feed of the fertilizer powder into the system. The conveying pipeline, usually made of stainless steel or other corrosion-resistant materials, transports the powder mixed with air. The air source provides the necessary pressure and volume to move the powder through the pipeline. The separation and collection unit, such as a cyclone or bag filter, separates the powder from the air and collects it in a storage bin or silo. The control system monitors and regulates the flow of material and air to maintain optimal operation.
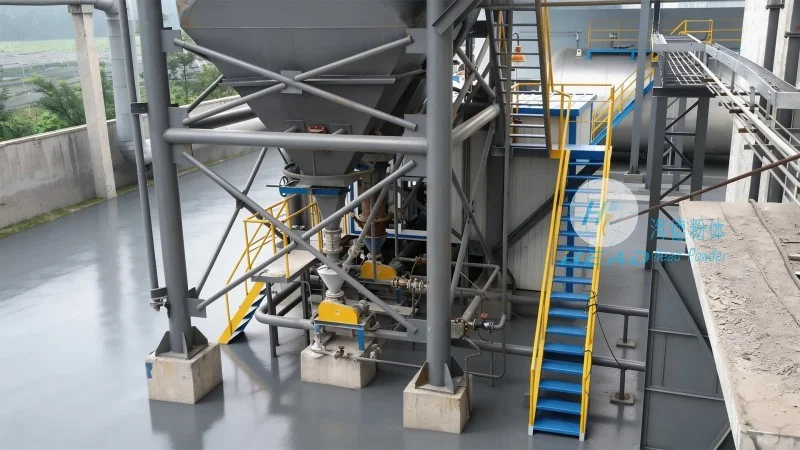
Design Principles and Considerations
The design of a fertilizer powder pneumatic conveying system involves several key principles to ensure efficiency, reliability, and safety. First, the system must be tailored to the specific properties of the fertilizer powder, including its particle size, moisture content, and flowability. For example, materials with high moisture content may require additional drying or moisture control measures to prevent caking or blockages. Second, the conveying distance and elevation change must be considered to determine the appropriate air pressure and blower capacity. Longer distances or higher elevations may require higher pressure or larger air volumes to maintain the conveying velocity. Third, energy efficiency is a critical design factor, as pneumatic conveying systems can consume significant power. Designers often use optimized pipe diameters, minimal bends, and efficient air separation to reduce energy consumption. Fourth, safety and environmental considerations are paramount. The system must be designed to prevent dust explosions, ensure proper ventilation, and comply with local regulations regarding emissions and noise. These principles guide engineers in creating a system that meets the specific needs of the fertilizer processing facility while minimizing operational costs and risks.
Advantages of Pneumatic Conveying in Fertilizer Handling
Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying offers several advantages in fertilizer handling. One of the most significant benefits is the ability to handle fine powders without the need for mechanical contact, which prevents contamination and degradation of the product. This is particularly important for fertilizers, as they are often sensitive to moisture and can easily caking or clumping if exposed to metal or other surfaces. Pneumatic systems also provide a dust-free environment, reducing the risk of respiratory issues for workers and minimizing the need for dust suppression equipment. Additionally, the flexibility of pneumatic conveying allows for easy integration with other processing equipment, such as mixers, granulators, or packaging machines. The system can be easily reconfigured to change the flow path or adjust the conveying rate, making it suitable for both batch and continuous production processes. These advantages make pneumatic conveying an ideal solution for modern fertilizer plants that require high efficiency, low maintenance, and consistent product quality.

Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, manufacturing, and installation of advanced powder handling systems, including fertilizer powder pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, the company has built a reputation for delivering high-quality, reliable equipment tailored to the unique needs of the fertilizer industry. HeadPowder's engineering team leverages years of experience and cutting-edge technology to develop customized solutions that optimize material flow, reduce operational costs, and enhance overall plant efficiency. The company's facilities in Shandong, China, are equipped with state-of-the-art manufacturing equipment and rigorous quality control processes to ensure that every system meets the highest standards. By partnering with HeadPowder, fertilizer manufacturers can benefit from expert guidance and support throughout the entire project lifecycle, from initial design and installation to ongoing maintenance and troubleshooting. HeadPowder's commitment to excellence and customer-centric approach makes it a trusted partner for businesses seeking to improve their powder handling capabilities and achieve sustainable growth in the agricultural sector.