

What is a Bentonite Powder Pneumatic Conveying System? And What Are Its Design Principles?
Bentonite powder pneumatic conveying systems are specialized industrial equipment designed to transport bentonite powder—a type of clay mineral—through a pipeline using air pressure. This technology is crucial in various industries, including construction, oil and gas, and environmental remediation, where bentonite is used for sealing, filtration, and stabilization. The system operates by creating a flow of air that carries the powder particles through the pipeline, ensuring efficient and dust-free transportation. Understanding the design principles behind these systems is essential for optimizing performance, minimizing downtime, and ensuring compliance with safety and operational standards.
Key Components of a Bentonite Powder Pneumatic Conveying System
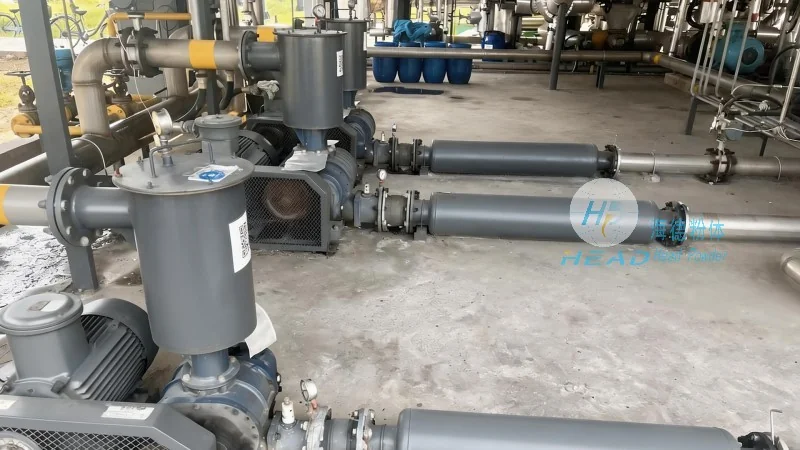
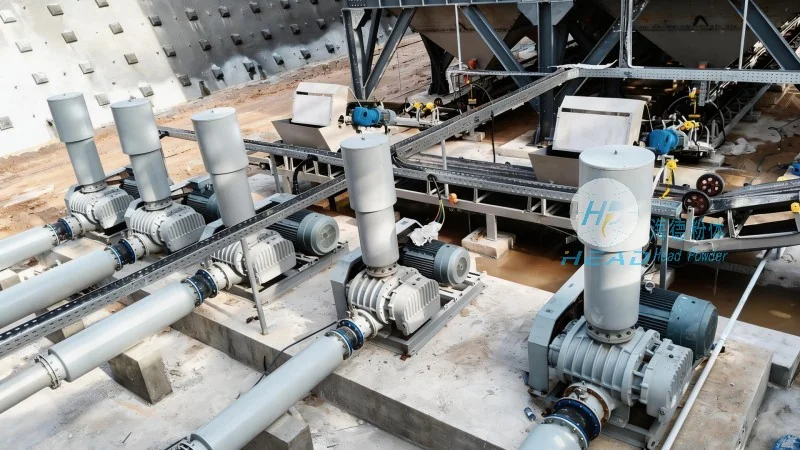
A typical bentonite powder pneumatic conveying system consists of several key components that work in tandem to achieve efficient material transport. These components include a powder feeder, a blower or compressor to generate the air flow, a pipeline network to guide the material, and a receiver or discharge unit to collect the powder at the destination. The powder feeder is responsible for accurately metering the bentonite powder into the system, ensuring a consistent flow rate. The blower or compressor provides the necessary air pressure and volume to move the powder particles through the pipeline. The pipeline network, often made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of bentonite and maintain airtight seals to prevent material loss. The receiver or discharge unit collects the powder at the end of the conveying line, allowing for easy unloading and storage.
Design Principles and Operational Mechanics
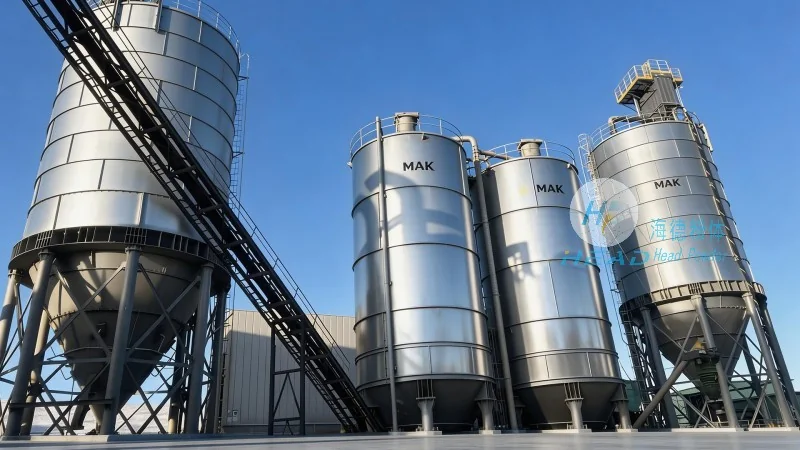
The design principles of a bentonite powder pneumatic conveying system are centered on maintaining a stable and continuous flow of material while minimizing the risk of blockages or system failures. One of the primary design considerations is the air-to-powder ratio, which refers to the amount of air used relative to the amount of powder being conveyed. An optimal air-to-powder ratio ensures that the powder particles are fully suspended in the air stream, preventing settling or clogging in the pipeline. Another critical principle is the pipeline layout, which must be designed to minimize changes in elevation and direction to avoid excessive pressure drops or turbulence that could lead to material degradation or system inefficiencies. The system also incorporates features such as pulse jets or air valves to maintain consistent flow and prevent the buildup of static charge, which is particularly important when handling fine powders like bentonite. Additionally, the use of corrosion-resistant materials and proper maintenance protocols is essential to ensure the longevity and reliability of the system.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems, including bentonite powder pneumatic conveying lines. HeadPowder is headquartered in Shandong, China, and has established itself as a trusted partner in the industry, providing high-quality equipment and tailored solutions to meet the diverse needs of its clients. The company specializes in designing and manufacturing custom pneumatic conveying systems that are tailored to specific application requirements, ensuring optimal performance and reliability. HeadPowder's commitment to quality, innovation, and customer satisfaction has made it a preferred choice for businesses operating in industries that rely on efficient powder handling and transportation.
Benefits of Using a Bentonite Powder Pneumatic Conveying System
Implementing a bentonite powder pneumatic conveying system offers numerous benefits for industrial operations. One of the most significant advantages is the ability to transport powder materials over long distances without the need for manual handling or traditional bulk transport methods. This reduces labor costs, minimizes the risk of material contamination, and improves overall operational efficiency. The system also provides a dust-free environment, which is crucial for maintaining workplace safety and compliance with environmental regulations. Additionally, pneumatic conveying systems are highly flexible, allowing for easy integration with existing production lines and the ability to adjust flow rates as needed. The use of corrosion-resistant materials and advanced control systems ensures that the system operates reliably over extended periods, reducing maintenance costs and downtime. Overall, a bentonite powder pneumatic conveying system is a cost-effective and efficient solution for handling and transporting bentonite powder in various industrial applications.